Rice husk ash, a byproduct of rice processing, is widely used in various industrial applications due to its unique properties. Efficient and reliable material conveying systems are essential for handling this material, ensuring smooth production processes and minimizing operational disruptions. This article provides a detailed overview of the operation process and working principle of rice husk ash material conveying systems, highlighting the key aspects that contribute to their effectiveness.
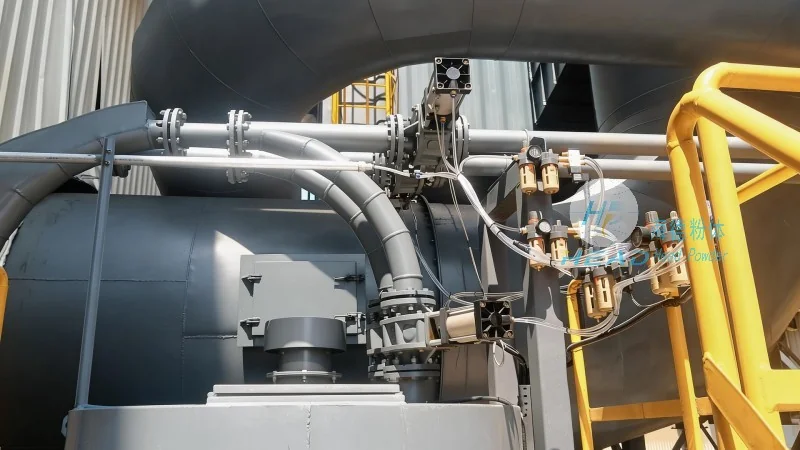
Rice husk ash material conveying systems are engineered to transport rice husk ash from storage areas to processing units or other destinations within industrial facilities. These systems are designed to handle the specific characteristics of rice husk ash, such as its light weight, abrasive nature, and potential for dust generation. The primary goal of these systems is to ensure safe, efficient, and consistent material transport while maintaining environmental standards and operational efficiency.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and supply of advanced material handling solutions. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing tailored solutions for diverse material conveying needs. HeadPowder's expertise lies in creating systems that are not only efficient but also durable and low-maintenance, catering to the demands of modern industrial operations.
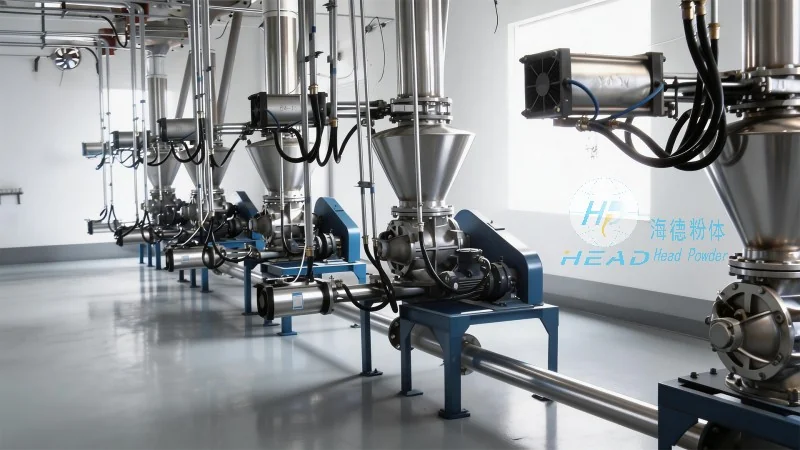
The core working principle of rice husk ash material conveying systems involves the use of mechanical components to move the material through a defined path. Typically, these systems employ a combination of components such as hoppers, feeders, conveyors (e.g., belt conveyors, screw conveyors), and control mechanisms. The process begins with the material being fed into a hopper, where it is stored and regulated before being transferred to the conveyor. The conveyor then transports the material to the desired location, such as a storage silo or processing equipment. Control systems monitor the flow rate, pressure, and other parameters to ensure optimal operation and prevent blockages or overloading.
The operation process of rice husk ash material conveying systems follows a systematic sequence to ensure smooth and continuous transport. Initially, the rice husk ash is collected from the source, such as a storage silo or a processing unit, and transferred to the conveying system's hopper. The hopper acts as a buffer, regulating the flow of material to the feeder. The feeder then controls the discharge rate, ensuring a consistent flow to the conveyor. The conveyor, powered by a motor, moves the material along its path, using rollers or a belt to transport the material. At the end of the conveyor, the material is discharged into the next processing stage or storage area. Throughout the process, sensors and control devices continuously monitor the system's performance, adjusting parameters as needed to maintain stability and efficiency.
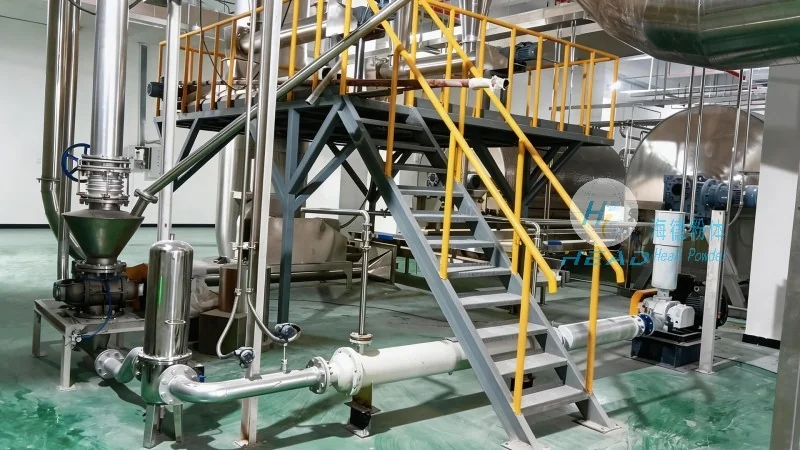
Several critical components are integral to the operation of rice husk ash material conveying systems. The hopper serves as the initial storage and feeding unit, providing a controlled environment for material accumulation. The feeder, often a rotary or vibratory type, regulates the material flow from the hopper to the conveyor, preventing overloading and ensuring a steady supply. The conveyor itself, which can be a belt conveyor or a screw conveyor, is the primary transport mechanism, moving the material along its designated path. Motor-driven systems provide the necessary power to operate the conveyor, while control panels manage the system's operation and monitoring functions. Additionally, dust collection systems may be integrated to handle the fine particles generated during transport, ensuring compliance with environmental regulations.
The efficient operation of rice husk ash material conveying systems offers numerous benefits to industrial operations. These systems enhance productivity by ensuring a continuous and reliable supply of material, reducing downtime and increasing throughput. They also improve safety by minimizing manual handling of the material, which can be dusty and abrasive. Furthermore, the systems are designed to be energy-efficient, reducing operational costs and environmental impact. Rice husk ash material conveying systems are widely used in industries such as cement production, construction materials, and agricultural applications, where the material is used as a raw ingredient or additive. The systems' adaptability allows them to be customized to meet the specific requirements of different industrial processes, making them a versatile solution for material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top