Understanding the operational dynamics and technical principles behind nitrile rubber material conveying is crucial for optimizing industrial processes. This article provides a detailed exploration of how these systems function, emphasizing the efficiency and reliability that characterize modern material handling solutions for nitrile rubber applications.
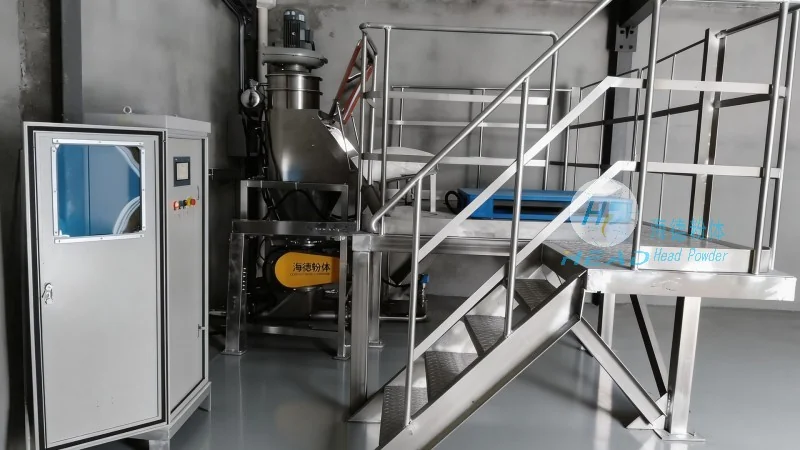
The nitrile rubber material conveying system comprises several critical components, each playing a vital role in ensuring smooth and consistent material transport. At the core of the system is the conveyor mechanism, which may include belt conveyors, screw conveyors, or pneumatic systems, depending on the specific requirements of the application. These components work in tandem to move nitrile rubber particles or bulk material from one location to another within an industrial setting. The design of these components is tailored to withstand the unique properties of nitrile rubber, such as its resistance to oil, fuel, and other chemicals, ensuring durability and long-term performance.
The operation of a nitrile rubber material conveying system typically follows a systematic sequence of steps. Initially, the nitrile rubber material is fed into the system, either manually or through an automated feeding mechanism. The material then travels along the conveyor path, guided by the system's design. As it moves, the material may undergo processes like sorting, screening, or blending, depending on the production requirements. The system's control mechanisms, such as sensors and control panels, monitor the flow and adjust the speed or direction as needed to maintain optimal performance. Finally, the material is discharged at the designated output point, ready for the next stage of processing or packaging.
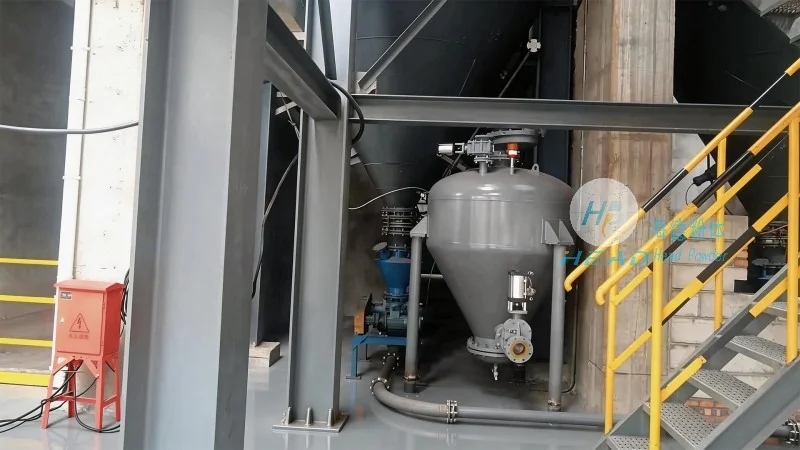
The working principle of nitrile rubber material conveying systems combines mechanical engineering with advanced control technologies. The mechanical aspect involves the transmission of power from a motor to the conveyor components, such as rollers or screws, which propel the material forward. This mechanical action is complemented by control systems that regulate the speed, direction, and timing of the conveying process. Sensors are integrated into the system to detect the presence and position of the material, providing real-time feedback to the control unit. This feedback loop ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity. The control systems may also include safety features, such as emergency stop buttons and overload protection, to prevent accidents and equipment damage.
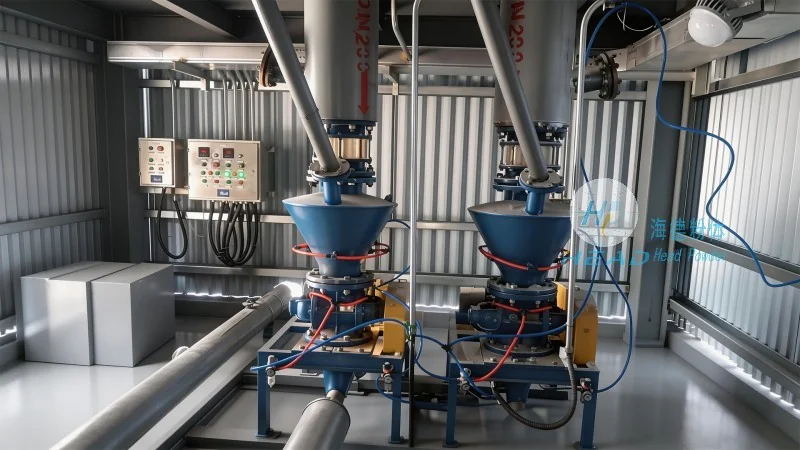
Nitrile rubber material conveying systems are widely used in various industries, including automotive, aerospace, and chemical manufacturing. In the automotive sector, these systems are essential for transporting nitrile rubber components used in seals, gaskets, and hoses. The aerospace industry relies on them for handling nitrile rubber parts that require high performance and resistance to extreme conditions. The chemical manufacturing industry uses these systems for processing nitrile rubber in bulk, ensuring consistent quality and safety. The versatility of nitrile rubber, combined with the efficiency of modern conveying systems, makes them indispensable in these and other sectors.
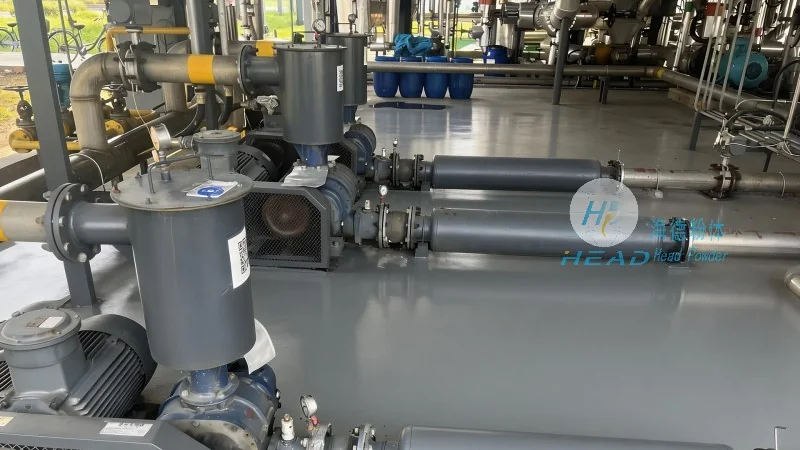
Implementing nitrile rubber material conveying systems offers several advantages over traditional manual or less efficient methods. One of the primary benefits is increased efficiency, as these systems can handle large volumes of material with minimal human intervention. This leads to higher productivity and reduced labor costs. Another advantage is improved safety, as the automated nature of the system minimizes the risk of accidents and exposure to hazardous materials. The systems also enhance product quality by ensuring consistent material handling, which reduces the likelihood of contamination or damage. Additionally, the durability of nitrile rubber and the robust design of the conveying equipment result in lower maintenance costs and longer operational lifespans.
In conclusion, nitrile rubber material conveying systems represent a sophisticated solution for efficient material handling in industrial applications. By understanding the operating process and working principles, businesses can optimize their operations and improve overall productivity. Shandong HeadPowder Engineering Co., Ltd., a leading provider of such systems, specializes in designing and manufacturing high-quality conveying solutions tailored to the unique needs of nitrile rubber processing. With a commitment to quality and innovation, HeadPowder delivers reliable and efficient systems that enhance the performance of industrial processes. Based in Shandong, China, HeadPowder leverages its expertise to meet the demands of various industries, providing customers with durable and effective nitrile rubber material conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top