Automatic quantitative pneumatic conveying systems represent a sophisticated solution for the efficient and precise transport of powders and bulk materials. These systems are designed to handle a wide range of powders, from fine particles to bulkier materials, ensuring consistent and controlled delivery in industrial applications. The technology integrates pneumatic conveying principles with advanced automation to achieve precise material measurement and transport, making it ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing.
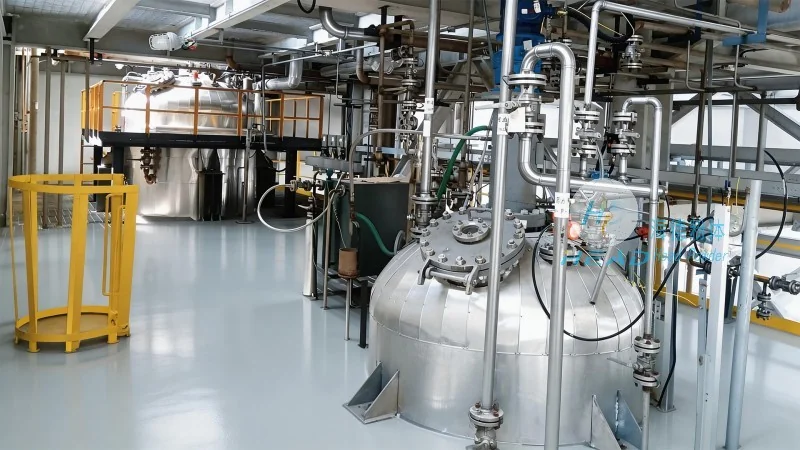
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in developing and supplying high-quality pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. HeadPowder's headquarters is located in Shandong, China, where the company maintains state-of-the-art manufacturing facilities and research centers to ensure the highest standards of product quality and performance.
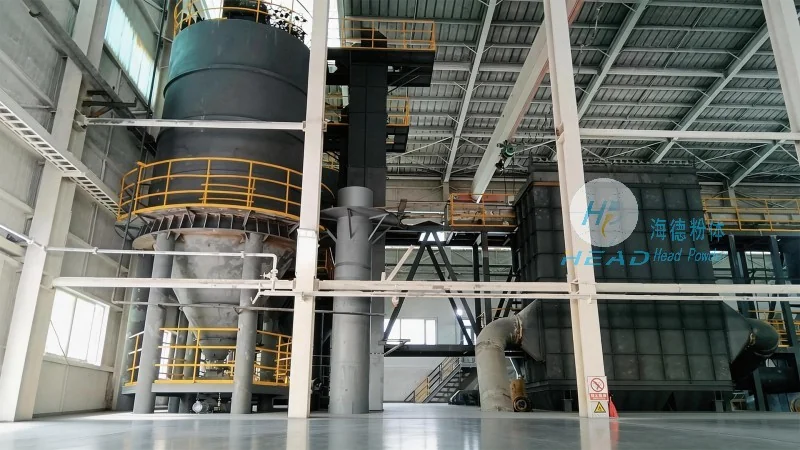
The automatic quantitative pneumatic conveying system operates on the principle of pneumatic transport, where materials are conveyed through a pipeline using compressed air. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The quantitative aspect is achieved through a precision feeder, often a rotary valve or a screw feeder, which measures and dispenses the material in controlled quantities. The compressed air, supplied by a blower or compressor, creates a pressure differential that propels the material through the pipeline. Sensors and control systems monitor the flow rate and pressure, ensuring accurate and consistent delivery. The system can be configured in various modes, such as dilute phase or dense phase, depending on the material characteristics and transport requirements.
One of the primary features of the automatic quantitative pneumatic conveying system is its high accuracy in material measurement. The system uses advanced control algorithms and sensors to maintain a consistent flow rate, minimizing material loss and ensuring that the exact quantity is delivered to the destination. This precision is crucial for applications where dosage accuracy is critical, such as in pharmaceutical production or food processing. Another key feature is the system's flexibility, as it can be adapted to handle different types of powders, including abrasive or corrosive materials, with appropriate material of construction (MOC) for the components. The system also offers a closed-loop operation, which helps in maintaining a clean and hygienic environment, reducing the risk of contamination and improving product quality. Additionally, the automated nature of the system reduces labor costs and increases operational efficiency, as it can run continuously without the need for manual intervention. The system's compact design and modular configuration make it suitable for both new installations and retrofitting into existing production lines, providing a cost-effective solution for material transport needs.
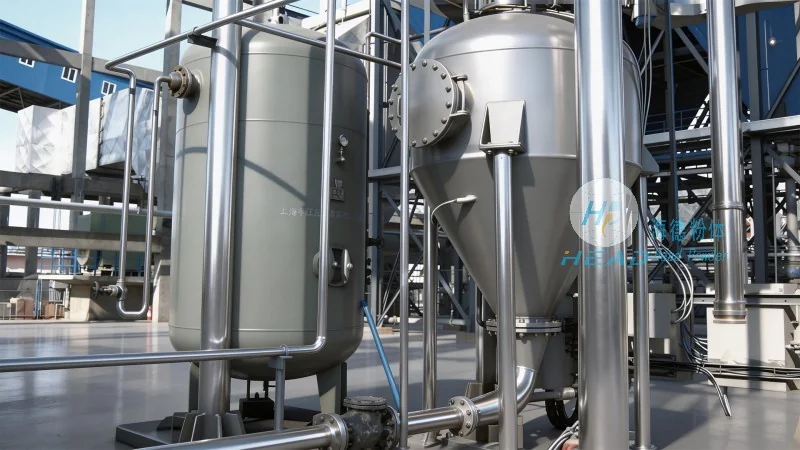
The technical specifications of the automatic quantitative pneumatic conveying system vary based on the specific model and application requirements. Typical specifications include conveying capacities ranging from a few kilograms per hour to several tons per hour, depending on the material and system configuration. The system can handle materials with particle sizes from sub-micron to several millimeters, and the conveying distance can range from short distances within a facility to long-distance transport over several kilometers. The system is designed to operate under different pressure conditions, with dilute phase systems operating at low to moderate pressures (typically 0.5 to 2 bar) and dense phase systems operating at higher pressures (up to 6 bar) for more efficient transport of bulkier materials. The system's components, such as the hopper, feeder, and pipeline, are constructed from materials like stainless steel, aluminum, or special alloys, depending on the material being conveyed, ensuring durability and resistance to corrosion. Application scenarios for this system include the transport of powders in pharmaceutical manufacturing for drug formulation, in food processing for ingredient delivery, in chemical industries for raw material handling, and in cement and mineral processing for bulk material transport. The system's ability to handle various materials and its precise delivery capabilities make it a versatile solution for a wide range of industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top