Coal ash slag pneumatic conveying systems are advanced industrial equipment designed to efficiently transport coal ash and slag from one location to another within industrial facilities. These systems utilize air as the primary medium to move particulate materials, offering a flexible and efficient solution for handling bulk materials in various industrial applications.
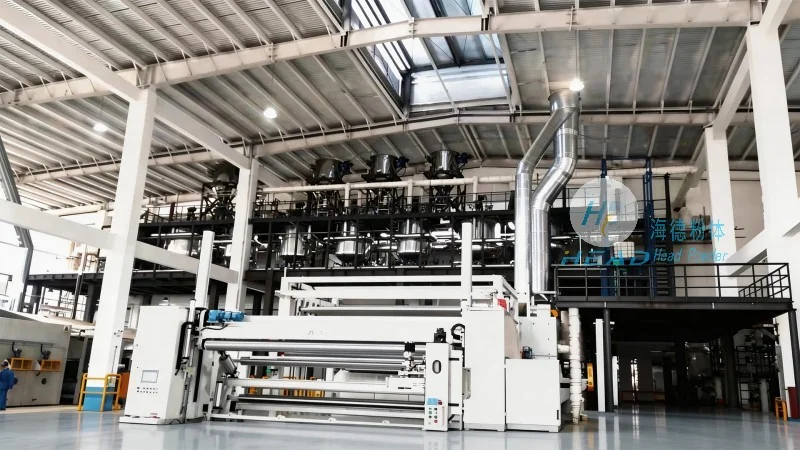
The core working principle of a coal ash slag pneumatic conveying system involves the use of a pressure or vacuum pump to generate airflow that propels the coal ash or slag particles through a pipeline network. The system typically consists of several key components, including a material hopper, a feeder, a conveying pipeline, a control system, and a dust collection or separation unit. When the material is fed into the hopper, it is then transported by the airflow through the pipeline to the destination point. The pressure or vacuum created by the pump ensures that the material is moved continuously and reliably, minimizing the need for mechanical components that could be prone to wear and tear.
There are two main types of pneumatic conveying systems based on the operating pressure: positive pressure systems and negative pressure systems. Positive pressure systems operate by blowing air into the pipeline, creating a pressure higher than the ambient air, which pushes the material forward. Negative pressure systems, on the other hand, create a vacuum in the pipeline, drawing the material into the system. Both systems have their advantages and are chosen based on the specific requirements of the application, such as the distance to be covered, the material characteristics, and the desired level of efficiency.
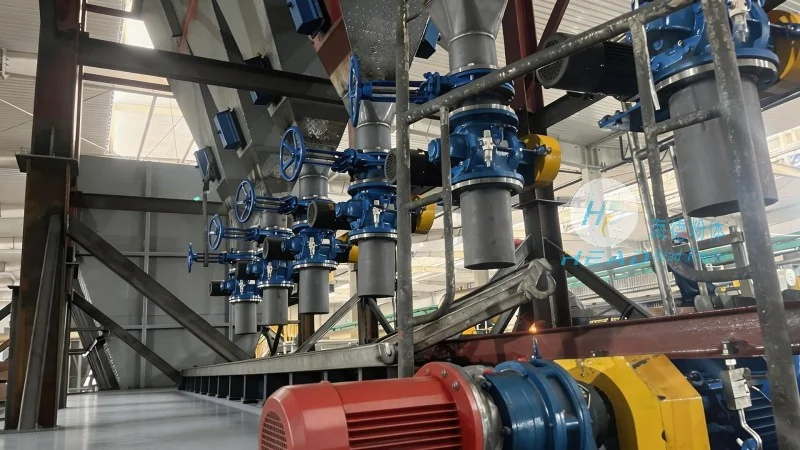
Coal ash slag pneumatic conveying systems offer several distinct features that make them an attractive choice for industrial material handling. One of the primary features is their ability to handle a wide range of material types, including fine powders, granules, and even larger particulates, without the need for additional processing or preparation. This versatility allows the system to be used in various industries, such as power generation, cement production, and waste management, where coal ash and slag are common byproducts.
Another significant feature is the system's flexibility in terms of layout and installation. Pneumatic conveying systems can be configured to follow complex routes, including vertical and horizontal segments, and can be easily integrated with existing infrastructure. This adaptability reduces the need for extensive civil engineering work and allows for the system to be installed in confined spaces or areas with limited access. The modular design of these systems also facilitates maintenance and repairs, as individual components can be replaced or serviced without disrupting the entire operation.
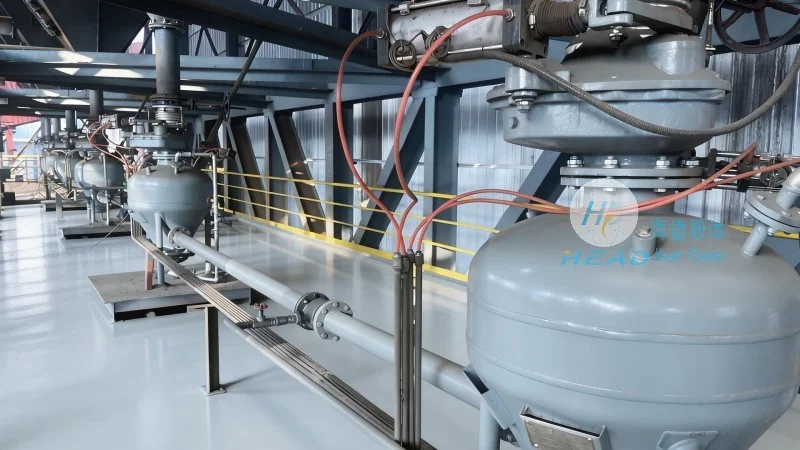
Efficiency and reliability are also key features of coal ash slag pneumatic conveying systems. By using air as the conveying medium, the system minimizes the risk of material degradation or contamination, which is particularly important for materials that are sensitive to moisture or temperature changes. Additionally, the absence of mechanical components like belts or buckets reduces the likelihood of mechanical failures and lowers the overall maintenance costs over the system's lifespan. The control systems used in these systems are typically advanced, with sensors and automation that ensure consistent performance and optimal energy usage.
The applications of coal ash slag pneumatic conveying systems are diverse and span across multiple industrial sectors. In power plants, these systems are commonly used to transport coal ash from the boiler to storage silos or disposal sites, ensuring a continuous and efficient process. In cement factories, the system helps in handling raw materials and byproducts, contributing to the overall production efficiency. Waste management facilities also benefit from these systems by effectively transporting slag and other waste materials to treatment or disposal locations.
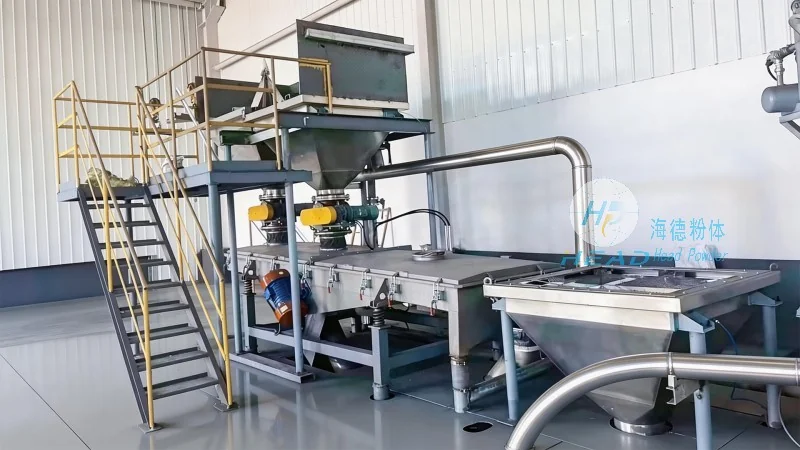
One of the main benefits of using pneumatic conveying systems is the reduction in labor costs and operational time. By automating the material transport process, the system minimizes the need for manual handling, which not only improves safety but also increases productivity. The systems also contribute to a cleaner and more organized industrial environment by reducing dust and spillage, which can be hazardous to workers and the surrounding environment. Furthermore, the energy efficiency of modern pneumatic conveying systems, particularly those using high-efficiency pumps and optimized pipeline designs, helps in reducing operational costs and environmental impact.
Coal ash slag pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of bulk materials in industrial applications. By leveraging the principles of pneumatic transport, these systems offer a flexible, versatile, and low-maintenance approach to material handling. The key features, including their ability to handle diverse materials, adaptability in layout, and high efficiency, make them a preferred choice for industries dealing with coal ash and slag. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, with a strong commitment to quality and customer satisfaction. HeadPowder, as the company is commonly known, is based in Shandong, China, and has established itself as a trusted partner for industrial material handling solutions, delivering systems that meet the highest standards of performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top