For industries dealing with soda ash, efficient material handling is crucial. The pneumatic conveying system, a key technology in this field, offers a reliable solution for transporting soda ash from one location to another. This article explores the working principle and key features of such systems, highlighting their benefits and applications.
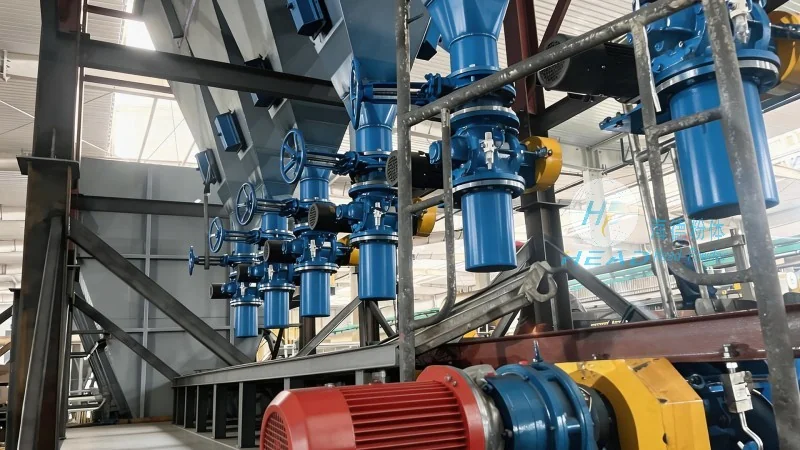
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing advanced material handling solutions. With a focus on innovation and quality, the company has developed state-of-the-art pneumatic conveying systems tailored for the soda ash industry. These systems are designed to meet the specific demands of transporting soda ash, ensuring safety, efficiency, and minimal material loss.
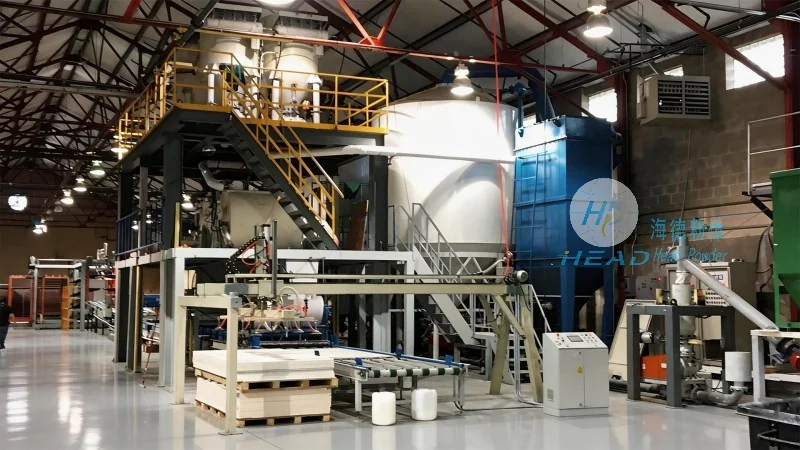
The core of a pneumatic conveying system is the use of air or gas to transport solid materials like soda ash. The process typically involves a few key components: a hopper to store the material, a conveyor line (either positive or negative pressure), and a receiver to collect the material at the destination. In positive pressure systems, air is blown into the conveyor line, pushing the soda ash forward. In negative pressure systems, air is drawn out, creating a vacuum that pulls the material through the line. The system operates by creating a flow of air that carries the soda ash particles, allowing for continuous and controlled movement.
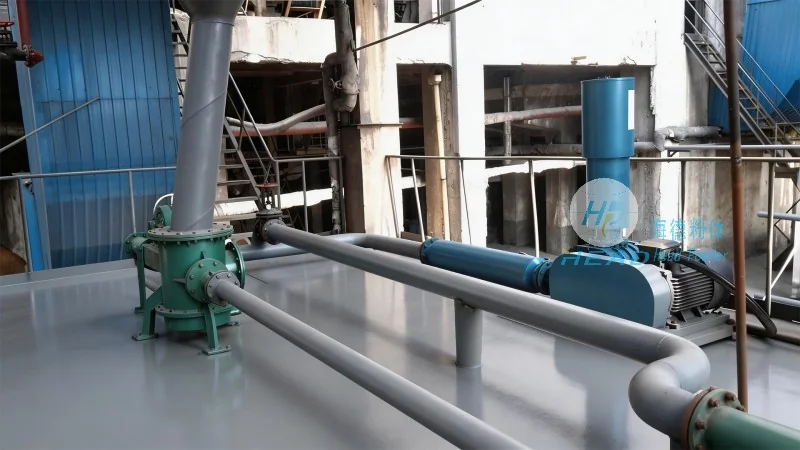
Several distinct features make pneumatic conveying systems ideal for soda ash applications. First, they offer a closed system, which helps in maintaining material integrity and preventing contamination. This is particularly important for soda ash, which can be sensitive to moisture or other environmental factors. Second, the systems provide high efficiency in terms of material transfer, with minimal downtime and low maintenance requirements. The design allows for smooth and consistent flow, reducing the risk of blockages or clogging. Additionally, these systems are flexible in terms of layout, enabling them to be adapted to various plant configurations without significant modifications. Another notable feature is the ability to handle different particle sizes and moisture levels, making them versatile for diverse soda ash processing needs.
Implementing a pneumatic conveying system for soda ash offers numerous advantages. The primary benefit is enhanced safety, as the closed system eliminates dust emissions and reduces the risk of material exposure to the environment. This not only improves workplace safety but also complies with environmental regulations. Furthermore, the system improves operational efficiency by automating the material handling process, reducing labor costs and increasing production throughput. In terms of applications, these systems are widely used in soda ash production facilities, from raw material transport to finished product delivery. They are also suitable for handling bulk quantities, making them ideal for large-scale operations.
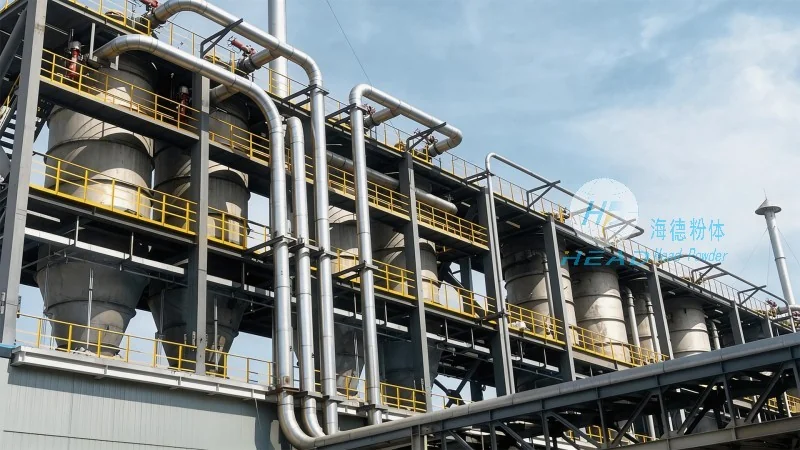
Shandong HeadPowder Engineering Co., Ltd. continues to be at the forefront of developing advanced pneumatic conveying systems for the soda ash industry. By understanding the working principle and leveraging the key features of these systems, industries can achieve efficient, safe, and cost-effective material handling solutions. The company’s commitment to quality and innovation ensures that their systems meet the evolving needs of the soda ash market, providing reliable performance and long-term value.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top