HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced fertilizer pneumatic conveying systems. These systems are essential for the efficient and safe transportation of bulk fertilizers in agricultural and industrial applications. This article explores the fundamental working principles and distinctive features of such systems, highlighting their role in modern material handling solutions.
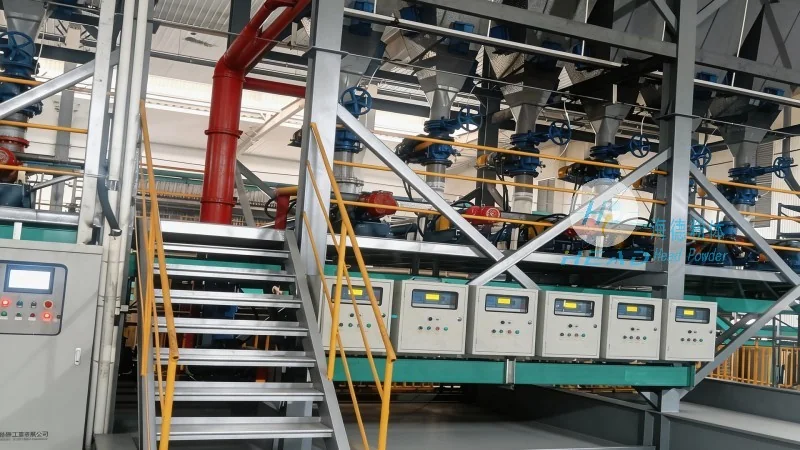
Fertilizer pneumatic conveying systems are engineered to transport bulk solid materials, such as granular or powdered fertilizers, through a pipeline using compressed air or vacuum. Unlike traditional mechanical conveyors, these systems rely on the kinetic energy of the air stream to move materials, offering a flexible and versatile solution for various industrial needs. The technology is widely adopted in the fertilizer industry due to its ability to handle different types of fertilizers, from nitrogen-based to phosphate and potassium compounds, while ensuring minimal product degradation and contamination.
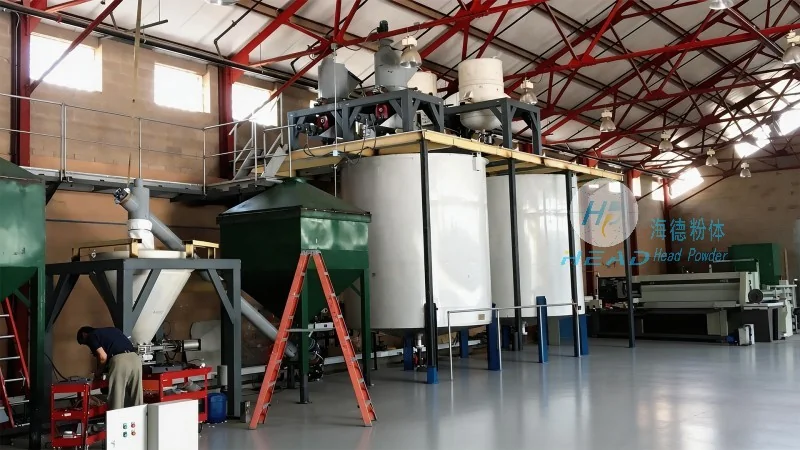
The core mechanism of a fertilizer pneumatic conveying system involves the creation of a high-velocity air stream within a pipeline. In a positive pressure system, compressed air is introduced at the material inlet, where the fertilizer is fed into the pipeline. The air flow accelerates the fertilizer particles, propelling them through the system. Conversely, in a negative pressure (or vacuum) system, a vacuum is created at the discharge end, drawing the material from the source and pulling it through the pipeline. The choice between positive and negative pressure depends on factors like material characteristics, distance, and system layout. The air velocity is carefully controlled to ensure the material remains suspended and transported efficiently without clogging or degradation.
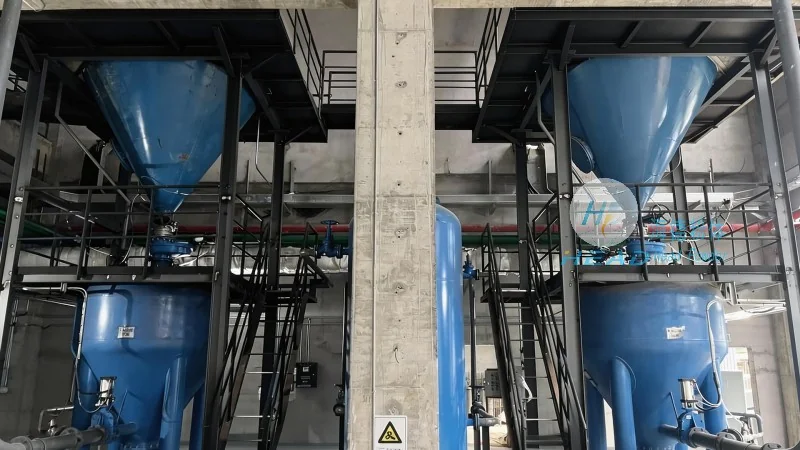
One of the primary advantages of fertilizer pneumatic conveying systems is their high efficiency in material handling. These systems can transport large volumes of fertilizer over significant distances with minimal energy consumption compared to mechanical conveyors. The technology also offers enhanced safety features, as it eliminates the need for moving parts in contact with the material, reducing the risk of product contamination and mechanical failure. Additionally, pneumatic conveyors are highly adaptable, capable of handling a wide range of fertilizer types, including sensitive granules that might be damaged by mechanical abrasion. The systems are designed for easy integration into existing production lines, with modular components that allow for flexible configuration and expansion. Another notable feature is the ability to maintain product quality, as the enclosed pipeline prevents exposure to moisture, dust, or external contaminants, preserving the fertilizer's chemical properties and shelf life.
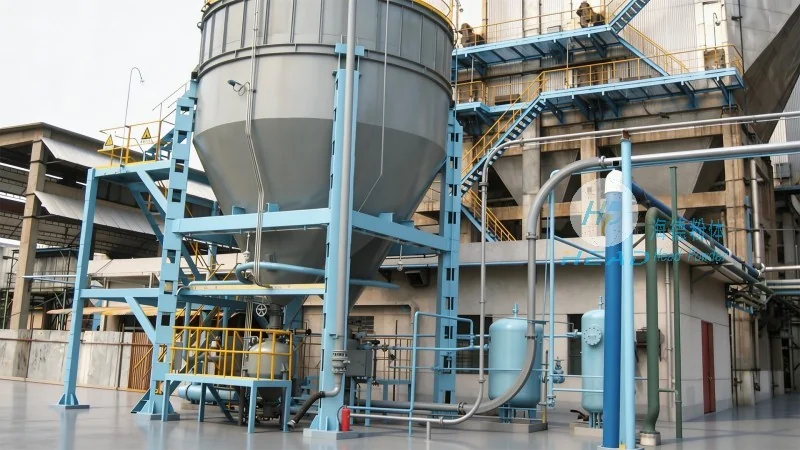
Fertilizer pneumatic conveying systems play a critical role in modern agricultural and industrial operations, enabling the seamless transfer of bulk fertilizers from storage to processing units, packaging lines, or distribution centers. The efficiency and reliability of these systems contribute to improved productivity and reduced operational costs for fertilizer manufacturers. By leveraging advanced engineering and materials, companies like Shandong HeadPowder Engineering Co., Ltd. have developed systems that meet the stringent requirements of the fertilizer industry, ensuring consistent performance and durability. The technology continues to evolve, with innovations in air flow control, material handling, and energy efficiency, further enhancing its applicability in diverse industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top