HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of pneumatic conveying systems for bulk materials. This article provides a detailed explanation of the fundamental principles behind grain bulk material pneumatic conveying systems, highlighting the technical aspects and operational benefits of such systems.
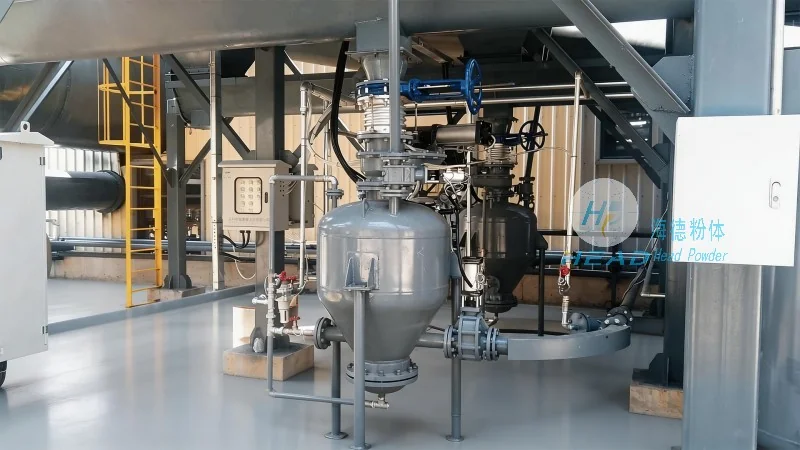
Pneumatic conveying systems are widely used in the agricultural and food processing industries to transport grain and other bulk materials efficiently. These systems utilize air or gas to move materials from one location to another, eliminating the need for mechanical components like belts or screws. The core principle involves creating a pressure differential to draw or push materials through a pipeline network.
The operation of a grain bulk material pneumatic conveying system typically involves several key components, including a feeder, a conveying line, a separator, and a receiver. The process begins when the grain is fed into the system, often through a hopper or a rotary valve. The feeder then meters the material into the conveying line, where it is mixed with air or gas under controlled pressure. As the mixture travels through the pipeline, the air flow propels the grain forward, maintaining a consistent flow rate and preventing material buildup or blockages.
Key to the system's efficiency is the air-to-material ratio, which must be carefully balanced to ensure optimal conveying performance. Too little air can lead to material settling or blockages, while too much air may cause excessive energy consumption and reduced material handling capacity. Advanced systems often incorporate variable speed drives and pressure sensors to dynamically adjust the air flow and material feed, enhancing operational flexibility and reducing wear on components.
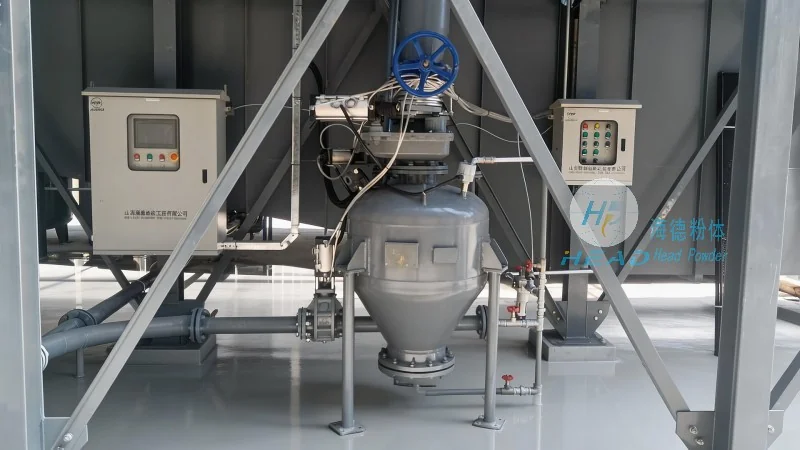
Compared to traditional mechanical conveying methods, pneumatic systems offer several advantages for grain handling applications. One of the primary benefits is the ability to transport materials over long distances with minimal maintenance. The absence of moving parts in the conveying line reduces the risk of mechanical failure and simplifies cleaning and sanitation, which is critical in food processing environments. Additionally, pneumatic conveying can handle a wide range of grain types, including powders, pellets, and granules, without causing segregation or degradation of the material.
Another significant advantage is the hygienic design of modern pneumatic systems. Components such as hoppers, feeders, and separators are often constructed from stainless steel or other food-grade materials, ensuring compliance with industry standards like FDA and HACCP. The enclosed pipeline system prevents contamination from external sources and minimizes dust emissions, contributing to a cleaner and safer working environment.
The effectiveness of a grain bulk material pneumatic conveying system depends on the proper selection and integration of its components. The feeder is a critical component, as it must consistently supply material to the conveying line without causing surges or interruptions. Common feeder types include rotary valves, screw feeders, and vibratory feeders, each with specific applications based on the grain's characteristics and flow properties.
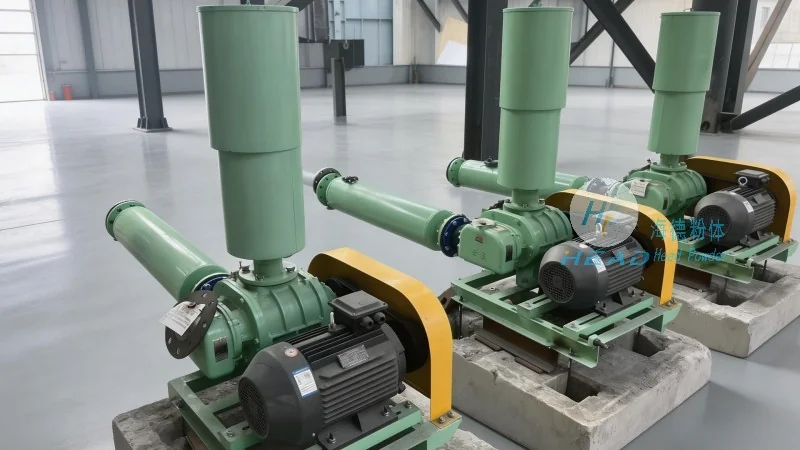
The conveying line itself is typically made of stainless steel or plastic, chosen for its durability and resistance to corrosion from grain dust and moisture. The diameter and length of the pipeline are carefully calculated to maintain the required air velocity, which is essential for preventing material settling. In larger systems, multiple pipelines may be used to distribute the material to different destinations, with branching and merging points designed to minimize pressure losses.
The separator is another vital component, responsible for separating the conveyed material from the air stream. This is typically achieved through a cyclone or a bag filter, which uses centrifugal force to separate the heavier grain particles from the lighter air. The separated grain is then collected in a receiver or storage bin, while the air is either vented to the atmosphere or recirculated back into the system, depending on the design.
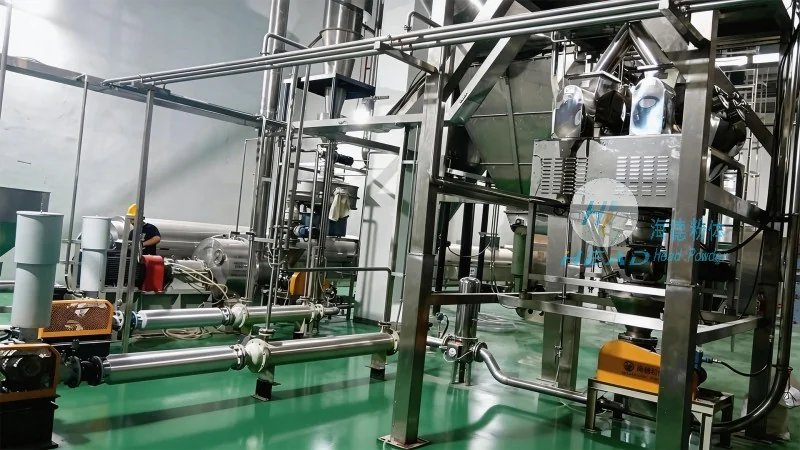
Pneumatic conveying systems are widely applied in various stages of grain processing, from storage and handling to milling and packaging. For example, in a grain storage facility, a pneumatic system can transport grain from silos to processing plants, reducing the need for manual labor and improving operational efficiency. In a flour mill, the system can convey raw wheat or other grains from storage bins to the milling equipment, ensuring a continuous and controlled feed.
In the packaging stage, pneumatic conveying can be used to move finished products from the milling line to packaging machines, where they are sealed and labeled. This seamless integration of conveying and packaging processes minimizes downtime and improves overall production throughput. Additionally, the system's ability to handle different grain types and sizes makes it suitable for diverse applications, from small-scale farms to large industrial processing facilities.
Grain bulk material pneumatic conveying systems represent a sophisticated and efficient solution for transporting grain and other bulk materials in the agricultural and food processing industries. By leveraging the principles of air flow and pressure differential, these systems offer significant advantages in terms of efficiency, hygiene, and flexibility. As a leading manufacturer in Shandong, China, HeadPowder Engineering Co., Ltd. provides customized pneumatic conveying solutions tailored to the specific needs of its clients, ensuring optimal performance and reliability in grain handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top