HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for calcined lime. This article delves into the fundamental principles behind such systems, exploring how they efficiently transport calcined lime from storage to processing units while maintaining material integrity and operational efficiency.
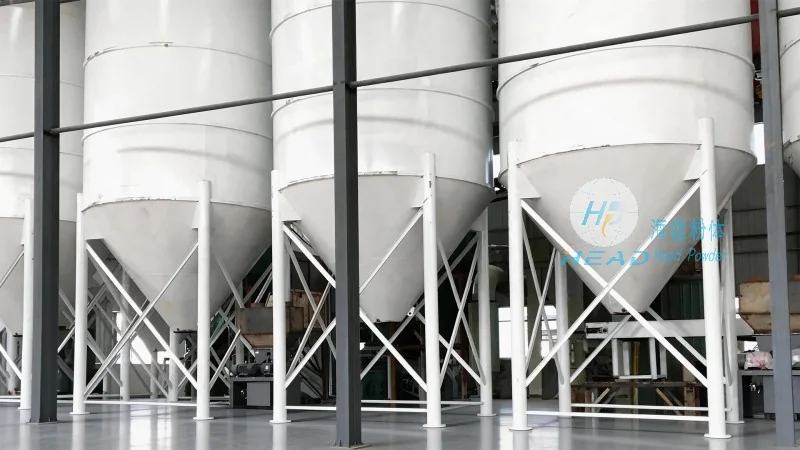
The pneumatic conveying system for calcined lime typically comprises several key components that work in concert to ensure smooth material handling. At the heart of the system is the material feed hopper, which stores the calcined lime and feeds it into the conveying line. A rotary valve or feeder is often used to regulate the flow of material from the hopper, ensuring a consistent and controlled feed rate. The conveying line itself can be either positive or negative pressure, depending on the specific application and distance requirements. Positive pressure systems use a blower or air compressor to push the material through the pipeline, while negative pressure systems use a vacuum to draw the material. For calcined lime, which is a dry, free-flowing powder, positive pressure systems are commonly preferred due to their ability to handle larger quantities and longer distances without clogging.
The operation of a pneumatic conveying system for calcined lime relies on the principles of fluid dynamics and particle transport. When the system is in operation, air is introduced into the conveying line at a controlled pressure. The material is then introduced into the air stream, and the combination of air velocity and particle size creates a suspension that allows the material to be transported through the pipeline. The air velocity must be sufficient to keep the particles in suspension and prevent them from settling or clogging the line. The system also includes a receiver or discharge hopper at the end of the line, where the calcined lime is deposited. The receiver may include a rotary valve or other equipment to control the discharge of the material into the next processing stage.
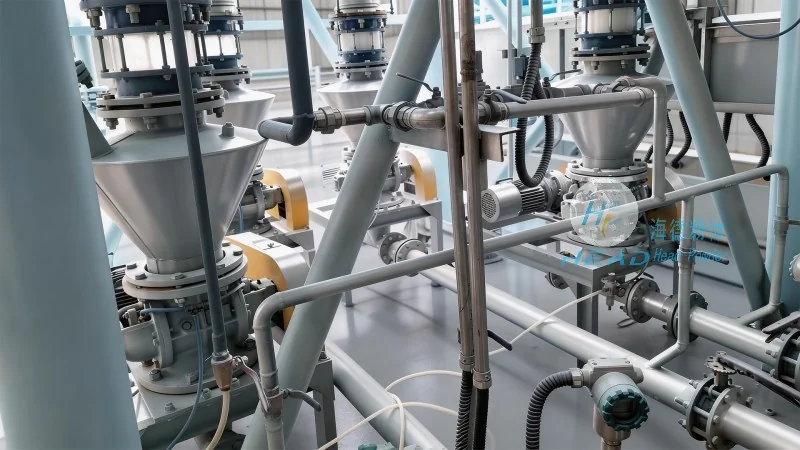
Implementing a pneumatic conveying system for calcined lime offers several advantages over traditional methods such as belt conveyors or bucket elevators. First, it eliminates the need for multiple transfer points and reduces the risk of material spillage or contamination. The enclosed system also helps maintain the quality of the calcined lime by preventing exposure to moisture or other environmental factors. Additionally, pneumatic conveying systems can be designed to handle varying material flow rates and can be easily integrated with other processing equipment. The systems are also relatively compact and can be installed in tight spaces, making them suitable for facilities with limited floor space. Another key advantage is the ability to transport calcined lime over long distances without the need for intermediate storage or handling, which can improve overall production efficiency.
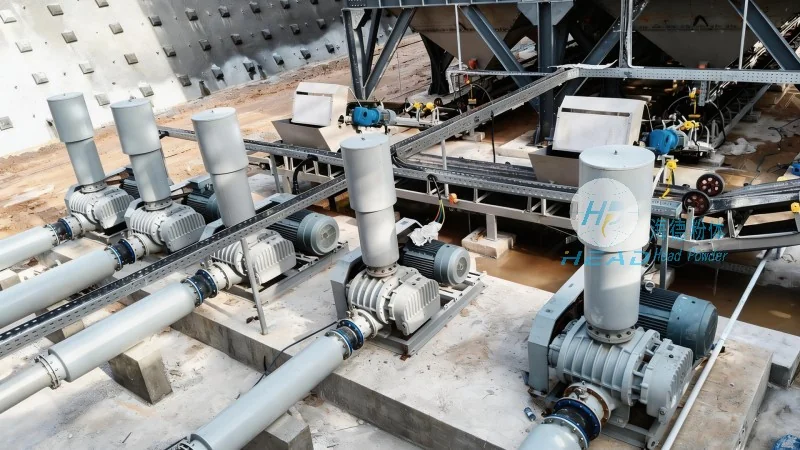
When designing a pneumatic conveying system for calcined lime, several factors must be considered to ensure optimal performance and longevity. The first consideration is the material properties of the calcined lime, including its particle size distribution, bulk density, and moisture content. These properties affect the air velocity required for proper suspension and the potential for clogging. The system designer must also consider the distance and elevation changes between the feed and discharge points, as these will impact the required air pressure and power consumption. The choice of pipeline material is another critical factor, as calcined lime is a abrasive material that can cause wear on the pipeline. Stainless steel or other corrosion-resistant materials are often used to ensure the system’s durability. Additionally, the system must be equipped with proper filtration and cleaning mechanisms to prevent the buildup of material in the air stream, which can reduce efficiency and increase maintenance costs.
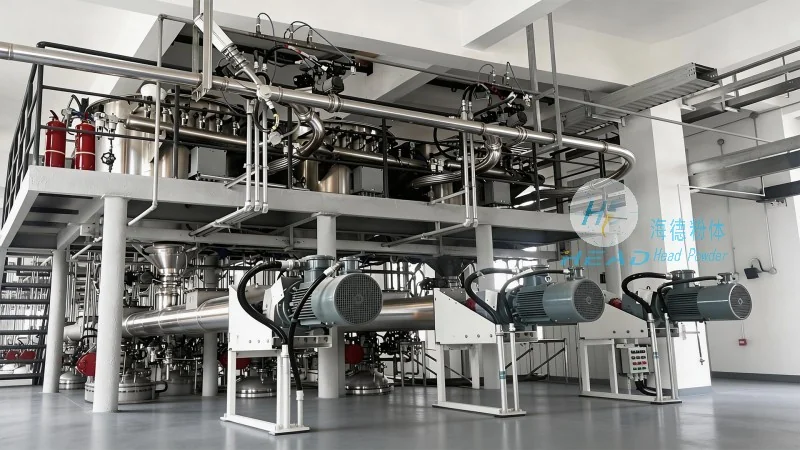
Pneumatic conveying systems for calcined lime are widely used in various industries, including cement production, chemical manufacturing, and food processing. In cement plants, calcined lime is often used as a raw material in the production of cement clinker. The pneumatic conveying system allows for the efficient transport of calcined lime from storage silos to the raw mill or kiln, where it is mixed with other raw materials. In chemical manufacturing, calcined lime is used as a filler or reactive agent in the production of various products, and the pneumatic conveying system ensures that the material is delivered to the processing line without any loss or contamination. In the food industry, calcined lime is used as a pH adjuster or buffering agent in the production of dairy products and other food items. The enclosed and sanitary design of the pneumatic conveying system is particularly important in this industry to maintain product quality and safety.
Proper maintenance is essential to ensure the long-term performance and reliability of a pneumatic conveying system for calcined lime. Regular inspection of the pipeline and components for signs of wear or damage is crucial. The rotary valve and feeder should be checked for proper operation and adjusted as needed to maintain consistent material flow. The air compressor or blower should be monitored for proper pressure and airflow, as any fluctuations can affect the system’s performance. The filtration system should be cleaned or replaced regularly to prevent clogging and maintain air quality. Additionally, the system should be inspected for any leaks or air loss, as these can reduce efficiency and increase energy consumption. By following these maintenance tips, the system can operate at peak efficiency and provide reliable performance for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top