Understanding the fundamental principles of pneumatic conveying systems is crucial for optimizing the handling and transportation of bulk materials, particularly in industries dealing with chemical powders like sodium bicarbonate. This article delves into the technical aspects of a sodium bicarbonate pneumatic conveying system, highlighting the key components, operational mechanisms, and the engineering considerations that ensure efficient and reliable material transport.
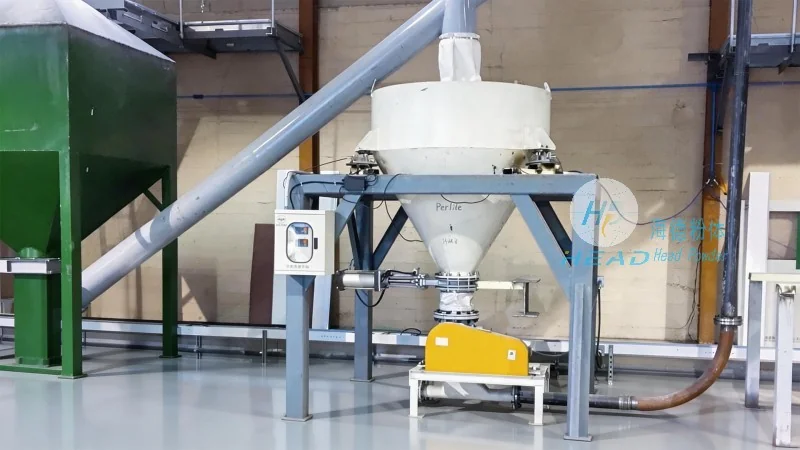
Pneumatic conveying is a method of transporting solid materials through a pipeline using a gas stream, typically air or other gases. It offers several advantages over traditional mechanical conveying systems, such as reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to move by other means. Sodium bicarbonate, also known as baking soda, is a common chemical powder used in various applications, including food processing, pharmaceuticals, and industrial manufacturing. Its properties, such as its fine particle size and relatively low density, make it an ideal candidate for pneumatic conveying applications.
The core components of a pneumatic conveying system for sodium bicarbonate include the material feed hopper, the air compressor or blower, the conveying pipeline, the control valves, and the discharge hopper. Each component plays a vital role in the overall operation of the system. The feed hopper is designed to store and meter the sodium bicarbonate, ensuring a consistent flow rate into the system. The air compressor or blower generates the necessary pressure or vacuum to move the material through the pipeline. The conveying pipeline is typically made of materials resistant to corrosion and abrasion, such as stainless steel or plastic, to withstand the handling of the chemical powder. Control valves are used to regulate the air flow and material flow, allowing for precise control over the conveying process. Finally, the discharge hopper collects the transported sodium bicarbonate and delivers it to the next stage of processing.
The operation of a sodium bicarbonate pneumatic conveying system can be categorized into two main types: positive pressure and negative pressure (or vacuum) systems. Positive pressure systems use a blower to force air into the pipeline, creating a pressure higher than the ambient air pressure, which pushes the material along the pipeline. Negative pressure systems, on the other hand, use a vacuum pump to create a low-pressure environment at the discharge end, drawing the material from the feed hopper into the pipeline. The choice between these systems depends on factors such as the distance to be covered, the material's characteristics, and the desired flow rate.
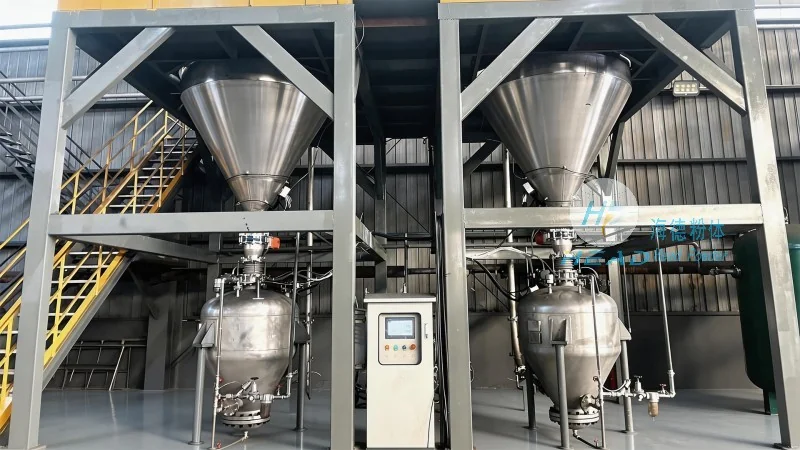
In a positive pressure system, the air compressor delivers compressed air to the material feed hopper. The sodium bicarbonate is then drawn into the air stream by the pressure differential, and the mixture is carried through the pipeline to the discharge point. At the discharge end, the air and material are separated, typically using a cyclone separator or a filter, and the air is recycled back to the compressor. In a negative pressure system, the vacuum pump creates a vacuum at the discharge end, which pulls the material from the feed hopper into the pipeline. The air and material mixture is then transported to a collection point where the material is separated from the air.
Several engineering factors must be considered to ensure the efficient and reliable operation of a sodium bicarbonate pneumatic conveying system. Particle size and density are critical parameters, as they affect the flow characteristics and the required air velocity. For sodium bicarbonate, which typically has a particle size ranging from 100 to 500 microns and a density of around 2.2 g/cm³, the air velocity must be carefully controlled to prevent particle segregation or blockages. The pipeline diameter and length also impact the system's performance; larger diameters and longer lengths may require higher air pressures or more powerful compressors to maintain the desired flow rate.
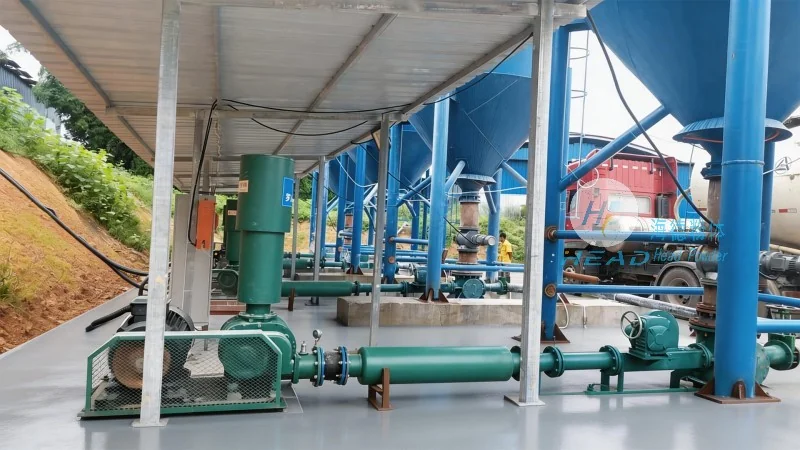
Corrosion resistance is another important consideration, as sodium bicarbonate is a mildly alkaline substance that can cause corrosion in certain materials. Stainless steel or corrosion-resistant plastics are commonly used for the pipeline and other components to ensure long-term durability. Additionally, the system must be designed to handle potential dust explosions, as fine powders like sodium bicarbonate can be a fire hazard under certain conditions. Proper grounding and explosion-proof components are essential safety measures.
Sodium bicarbonate pneumatic conveying systems are widely used in various industrial applications, including food processing, where the material is used as a leavening agent or in the production of baking powders. In pharmaceutical manufacturing, the system ensures the safe and hygienic transport of sodium bicarbonate, which is used as an excipient or active ingredient in medications. The system's ability to handle fine powders without generating dust or causing contamination makes it ideal for these applications. The benefits of using a pneumatic conveying system for sodium bicarbonate include improved process efficiency, reduced labor costs, and enhanced product quality. By maintaining consistent flow rates and minimizing material loss, the system contributes to overall operational excellence.
Understanding the principle of a sodium bicarbonate pneumatic conveying system is essential for optimizing material handling in industrial settings. The system's ability to efficiently transport fine powders like sodium bicarbonate, while maintaining product quality and safety, makes it a preferred choice for many industries. Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for bulk material handling, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its systems meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder leverages its expertise to deliver solutions that enhance operational efficiency and reduce costs for its clients, contributing to the success of their businesses.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top