The dry pebble pneumatic conveying system is a specialized industrial solution designed for the efficient transport of dry, granular materials such as pebbles, gravel, or similar bulk solids. This system operates on the principle of pneumatic conveying, where air is used as the medium to move material through a pipeline network. The technology is particularly valuable in applications requiring dust-free, low-maintenance, and flexible material handling, making it suitable for various industries including mining, construction, and manufacturing.
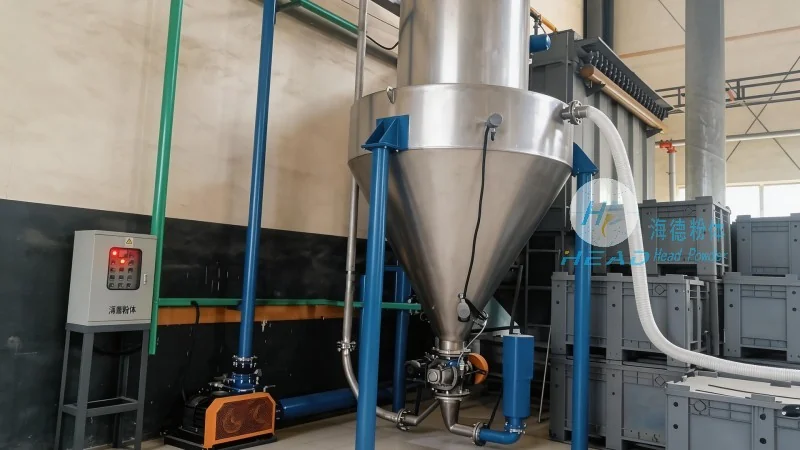
At the heart of the dry pebble pneumatic conveying system lies the fundamental concept of using compressed air to create a flow that propels the material. The system typically consists of a blower or air compressor, a hopper for material storage, a pipeline network, and a discharge point. The process begins with material being fed into the hopper, where it is then drawn into the pipeline by the moving air stream. The air velocity within the pipeline must be sufficient to overcome the gravitational and frictional forces acting on the pebbles, ensuring stable and continuous transport. Key factors influencing the system's performance include air pressure, flow rate, pipeline diameter, and the characteristics of the pebble material (e.g., size, density, and moisture content).
The dry pebble pneumatic conveying system comprises several critical components, each playing a vital role in the overall operation. The first component is the air compressor or blower, which generates the necessary pressure and volume of air to drive the material. This equipment is typically selected based on the system's required air flow rate and pressure, ensuring it can handle the material's specific characteristics. The second component is the material hopper, which stores the pebbles and provides a controlled feed to the conveying line. The hopper is equipped with a feeder, such as a rotary valve or screw feeder, to regulate the material flow into the pipeline. The pipeline itself is a crucial element, often made of stainless steel or other corrosion-resistant materials, to withstand the abrasive nature of pebbles and prevent material buildup or blockages. The pipeline network may include bends, elbows, and expansion joints to accommodate changes in direction and elevation, maintaining consistent air velocity and preventing pressure losses. Finally, the discharge point, which can be a silo, storage bin, or processing equipment, receives the conveyed pebbles, completing the material transport cycle.
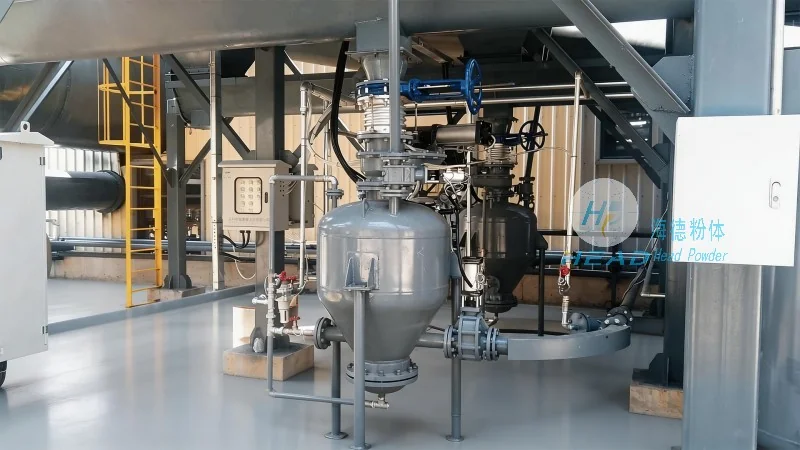
Compared to traditional mechanical conveying methods, dry pebble pneumatic conveying systems offer several advantages that make them an attractive choice for industrial applications. One of the primary benefits is the ability to transport materials over long distances with minimal infrastructure. Unlike belt conveyors or bucket elevators, pneumatic systems can navigate complex layouts, including vertical lifts and horizontal curves, without the need for additional support structures. This flexibility reduces installation costs and allows for easier integration into existing facilities. Another significant advantage is the dust-free operation. By enclosing the material in a sealed pipeline, the system prevents dust emissions, which is crucial for maintaining a safe and healthy work environment, especially in industries where dust can be a health hazard or cause equipment damage. Additionally, pneumatic conveying systems are generally low-maintenance, as they have fewer moving parts compared to mechanical systems, reducing downtime and maintenance costs. The system's ability to handle abrasive materials like pebbles is also a key advantage, as the enclosed pipeline protects both the material and the equipment from wear and tear. Furthermore, the system can be easily scaled up or down to meet changing production demands, providing flexibility in material handling operations.
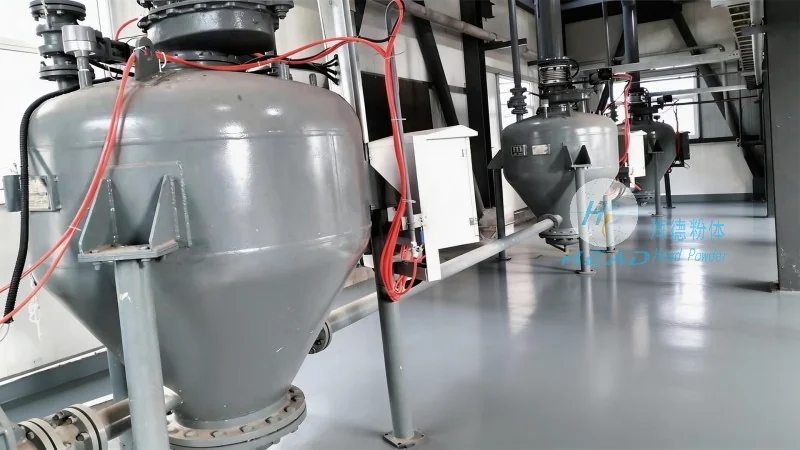
Dry pebble pneumatic conveying systems are widely used in various industries where the transport of dry, granular materials is essential. In the mining industry, these systems are employed to move crushed rock, gravel, or ore from processing plants to storage facilities or for further processing. The ability to handle abrasive materials and transport them over long distances makes the system ideal for mining operations, where efficiency and durability are critical. In the construction industry, the system is used to transport sand, gravel, or other aggregates from quarries or storage sites to construction sites. The dust-free operation and flexibility of the system help maintain site safety and compliance with environmental regulations. The manufacturing industry also benefits from dry pebble pneumatic conveying systems, particularly in applications involving the transport of raw materials or finished products. For example, in the production of building materials, such as concrete or asphalt, the system can efficiently convey aggregates from storage to mixing plants. Additionally, in the chemical industry, where the handling of dry powders or granules is common, the system can be adapted to transport materials like limestone or silica, ensuring a consistent and controlled supply to production lines.
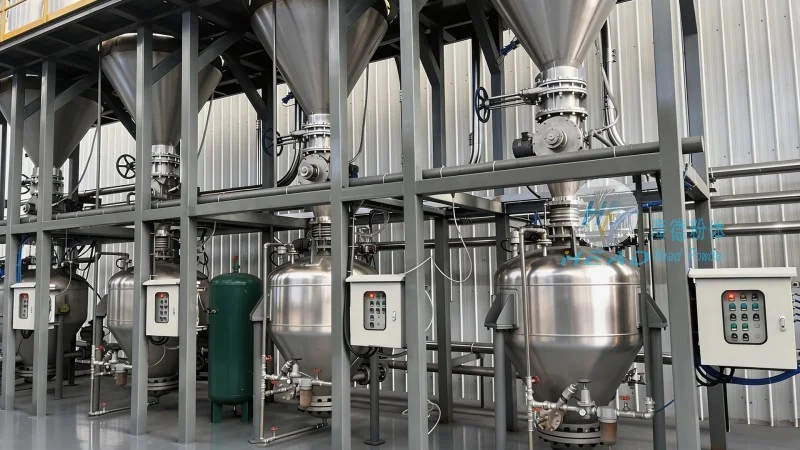
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of industrial material handling solutions, specializing in the design, manufacturing, and installation of pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, delivering high-quality equipment tailored to the specific needs of its clients. HeadPowder's expertise lies in understanding the unique challenges of material handling and developing customized solutions that optimize efficiency, reduce costs, and enhance safety. The company's team of experienced engineers and technicians works closely with clients to assess their material handling requirements, conduct feasibility studies, and provide comprehensive system designs. HeadPowder's commitment to quality is evident in its adherence to international standards and rigorous testing procedures, ensuring that all products meet the highest performance and safety requirements. The company's facilities, located in Shandong, China, are equipped with advanced manufacturing capabilities and state-of-the-art testing equipment, enabling it to produce reliable and durable pneumatic conveying systems that stand the test of time.
The dry pebble pneumatic conveying system represents a sophisticated and efficient solution for the transport of dry, granular materials, offering significant advantages over traditional mechanical methods. As industries continue to demand more reliable and flexible material handling solutions, the demand for pneumatic conveying systems is expected to grow. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing cutting-edge solutions that meet the evolving needs of its clients. By leveraging its expertise and commitment to quality, HeadPowder is poised to continue leading the way in the development and application of advanced pneumatic conveying systems, contributing to the efficiency and sustainability of industrial operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top