Dust-free closed-circuit pneumatic conveying systems represent a sophisticated solution in material handling, designed to transport bulk materials efficiently while maintaining a controlled environment. These systems are particularly valuable in industries where material purity, safety, and operational efficiency are paramount. The HeadPowder dust-free closed-circuit pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., based in China, is a prime example of this technology, offering advanced features and reliable performance for various industrial applications.
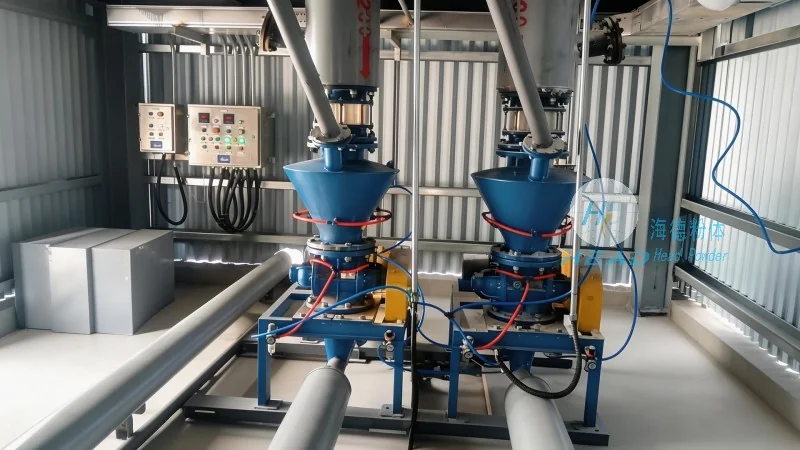
The HeadPowder dust-free closed-circuit pneumatic conveying system is engineered with several distinctive features that set it apart in the market. Firstly, its closed-loop design eliminates the need for external air intake, thereby preventing contamination from external sources and maintaining the integrity of the conveyed material. This feature is crucial for industries like pharmaceuticals, food processing, and chemical manufacturing, where product purity is non-negotiable. Secondly, the system employs high-efficiency filtration and recycling mechanisms, ensuring that any airborne particles are captured and returned to the system, reducing waste and enhancing overall efficiency. Additionally, the system is equipped with advanced control systems that allow for precise regulation of air flow, pressure, and material flow rates, enabling seamless operation and minimizing downtime. The robust construction of the system, utilizing high-quality materials, ensures durability and long-term reliability, even under demanding operational conditions.
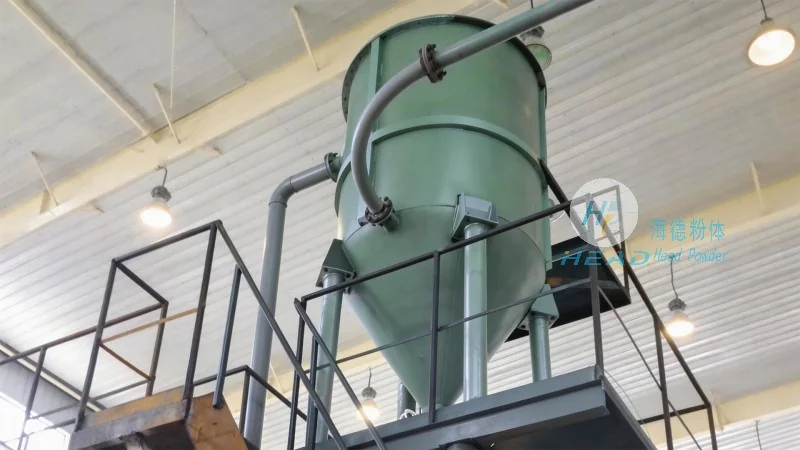
The operational principle of the HeadPowder dust-free closed-circuit pneumatic conveying system is based on the fundamental concept of pneumatic transport, where materials are conveyed through a pressurized or vacuum system using air or other gases. In a closed-circuit configuration, the system operates in a loop, with the material being drawn from a hopper or storage container and transported through a series of pipes to a destination, such as a processing unit or storage silo. The system uses a combination of positive pressure and vacuum to move the material, with the air being filtered and recycled to maintain a dust-free environment. The process begins with the material being introduced into the system, where it is mixed with the air stream. The air, under pressure, propels the material through the conveying line, while the filtration system captures any particles that may escape, ensuring that the air is clean and free from contaminants. The material is then deposited at the receiving point, and the air is returned to the system for reuse. This closed-loop operation minimizes energy consumption and reduces the environmental impact compared to traditional open-circuit systems.
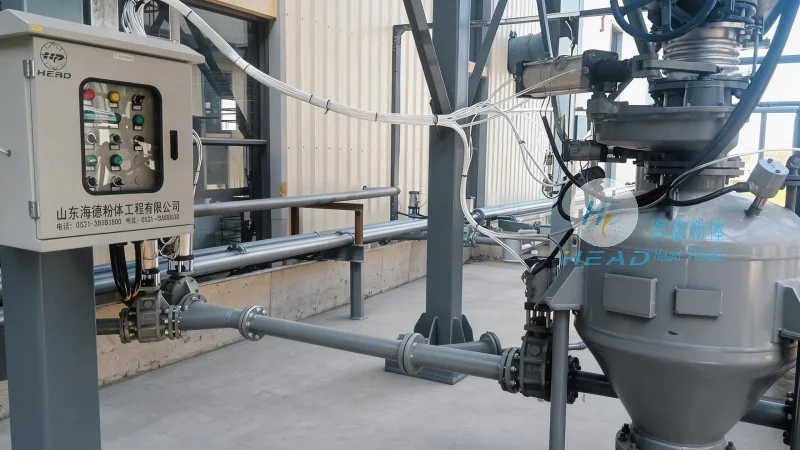
The dust-free closed-circuit pneumatic conveying system offers numerous advantages that make it a preferred choice for various industrial applications. One of the primary benefits is the elimination of dust and airborne particles, which not only protects the material from contamination but also enhances workplace safety by reducing the risk of respiratory issues and other health hazards. This feature is particularly important in industries where human exposure to dust is a concern, such as in pharmaceutical manufacturing or food processing. Another advantage is the system's ability to handle a wide range of materials, including powders, granules, and even bulk solids, with minimal degradation. The closed-circuit design also reduces the need for manual handling and cleaning, as the system can be operated continuously without the need for frequent shutdowns for maintenance. The HeadPowder system is particularly well-suited for applications in the pharmaceutical, food, chemical, and agricultural sectors, where product quality and safety are critical. For example, in pharmaceutical manufacturing, the system can be used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets stringent quality standards. In the food industry, the system can handle various food powders, such as flour, sugar, and spices, while maintaining hygiene and preventing cross-contamination. The chemical industry also benefits from the system's ability to transport hazardous materials safely, as the closed-circuit design prevents the release of toxic gases or particles into the environment.
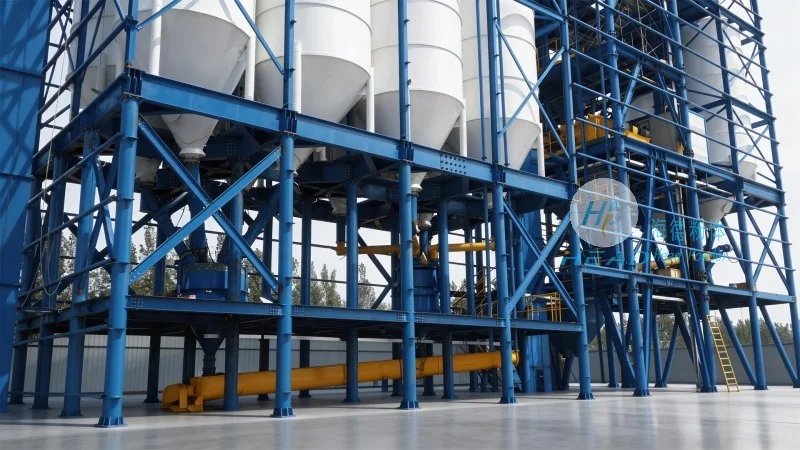
The HeadPowder dust-free closed-circuit pneumatic conveying system is available in various configurations to meet the specific needs of different industries and applications. The system can be customized in terms of conveying capacity, material type, and operational parameters, ensuring that it can be tailored to the unique requirements of each client. Technical specifications include a conveying capacity ranging from 0.5 to 50 tons per hour, depending on the material and system design. The system operates at pressures between 0.5 to 2 bar, with adjustable air flow rates to optimize performance. The filtration system is equipped with high-efficiency particulate air (HEPA) filters, capable of capturing particles as small as 0.3 microns, ensuring that the air is clean and free from contaminants. The system also includes safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure safe operation. Additionally, the system can be integrated with other equipment, such as mixers, classifiers, and storage silos, to form a complete material handling solution. The HeadPowder team provides comprehensive technical support and customization services, working closely with clients to design and implement the most suitable system for their needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top