When discussing industrial material handling solutions, the gray bin pneumatic conveying system stands out as a highly efficient and versatile option for transporting bulk materials. This system, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to handle various powder and granular materials with precision and reliability. Understanding its working principle and key features is essential for industries seeking to optimize their material transport processes.
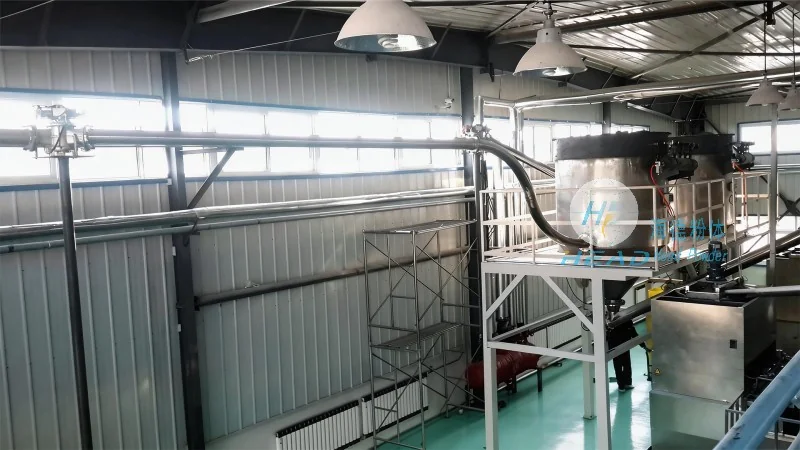
The core of the gray bin pneumatic conveying system lies in its air-driven mechanism. The system operates by using compressed air to create a flow that propels material from the storage bin (gray bin) through a series of pipelines to the discharge point. The process typically involves several key components: the storage bin, air compressor, conveying pipes, and a control system. As compressed air is introduced into the bin, it creates a negative pressure or positive pressure environment, depending on the system design, which draws the material into the conveying line. The material is then carried along the pipes by the air stream, reaching the destination where it is discharged. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
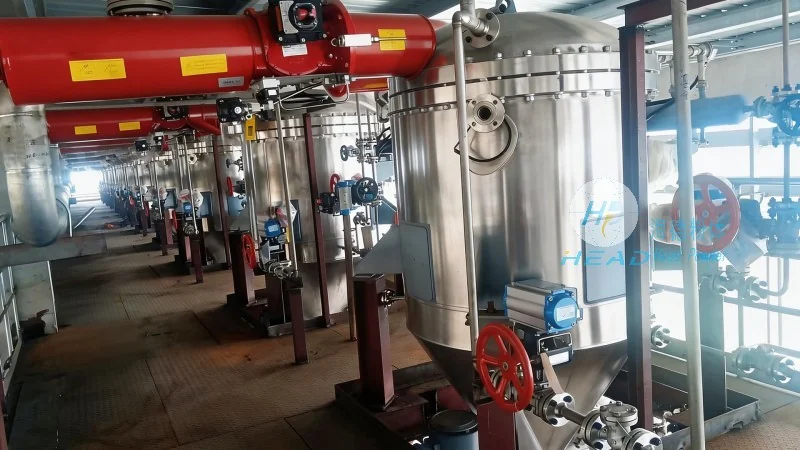
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into the gray bin pneumatic conveying system to enhance performance and user experience. One of the most notable features is its adaptability to different material types. The system can handle a wide range of materials, including powders, granules, and even fine particles, without causing degradation or segregation. This versatility makes it suitable for industries such as pharmaceuticals, food processing, and chemical manufacturing. Another significant feature is the system's energy efficiency. By utilizing compressed air as the primary driving force, it minimizes energy consumption compared to traditional mechanical conveying systems. This not only reduces operational costs but also aligns with sustainability goals. The gray bin itself is designed for durability and easy maintenance. Made from high-quality materials, it can withstand the rigors of continuous operation and is equipped with features like level indicators and access ports for monitoring and maintenance. Additionally, the system offers precise control over material flow. Advanced control systems allow operators to adjust the air pressure and flow rate, ensuring consistent and controlled delivery of materials. This level of control is crucial for applications where material consistency is critical, such as in pharmaceutical production or food processing. The system also incorporates safety features to protect both the equipment and the operators. These include pressure relief valves, emergency shut-off mechanisms, and monitoring systems that alert users to any abnormalities in the system's operation. Such safety measures ensure that the system operates reliably and safely in industrial environments.
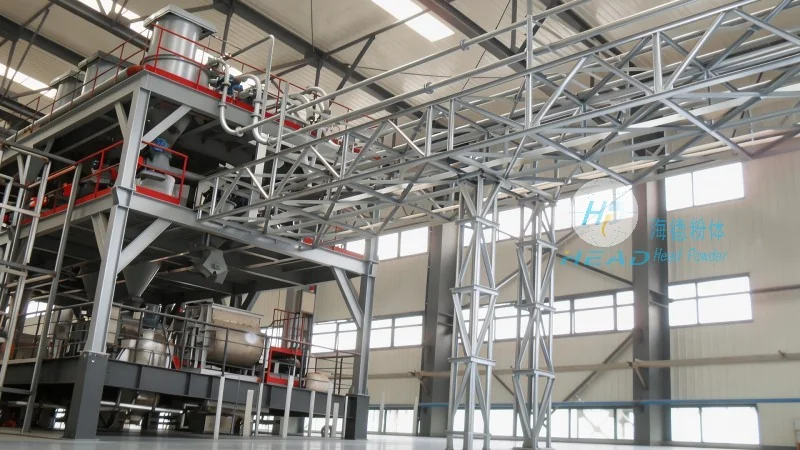
The gray bin pneumatic conveying system, manufactured by Shandong HeadPowder Engineering Co., Ltd., finds applications across various industries due to its robust design and efficient performance. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the materials remain uncontaminated and in their original state. The system's ability to maintain a sterile environment and prevent cross-contamination is a major advantage. In the food processing industry, it handles ingredients like flour, sugar, and spices, maintaining the quality and freshness of the products. The system's hygienic design and easy cleaning features make it suitable for food-grade applications. In the chemical industry, it transports various powders and granules, including chemicals and reagents, with precision and safety. The system's ability to handle corrosive materials and its robust construction make it ideal for these applications. The benefits of using this system extend beyond just material transport. It reduces labor costs by automating the material handling process, minimizes material loss and waste, and improves overall production efficiency. The system's compact design allows for easy integration into existing production lines, without requiring significant modifications to the facility. This makes it a cost-effective solution for industries looking to upgrade their material handling capabilities. Furthermore, the system's low maintenance requirements contribute to long-term cost savings. With fewer moving parts and less wear and tear, the system requires less downtime for maintenance, ensuring continuous operation and higher productivity.
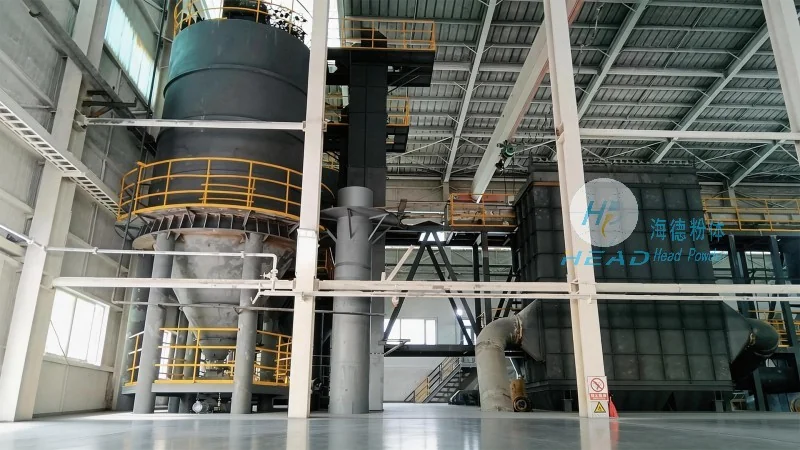
Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of industrial material handling solutions, with the gray bin pneumatic conveying system being a prime example of their expertise. The system's working principle, based on air-driven conveying, and its key features, such as adaptability, energy efficiency, and precise control, make it a superior choice for industries requiring reliable and efficient material transport. The company's commitment to quality and innovation is reflected in the system's design and performance. By choosing the gray bin pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd., industries can enhance their operational efficiency, reduce costs, and improve the quality of their products. The system's robust construction and advanced features ensure that it meets the demands of modern industrial applications, providing a reliable solution for material handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top