For industrial operations dealing with bulk powders, efficient and reliable material handling is crucial. A tonne bag unloading station powder conveying line is a specialized system designed to facilitate the safe and effective transfer of bulk materials from large bags, commonly known as tonne bags, into processing equipment or storage systems. This article explores the functionality of such systems and the underlying design principles that ensure optimal performance.
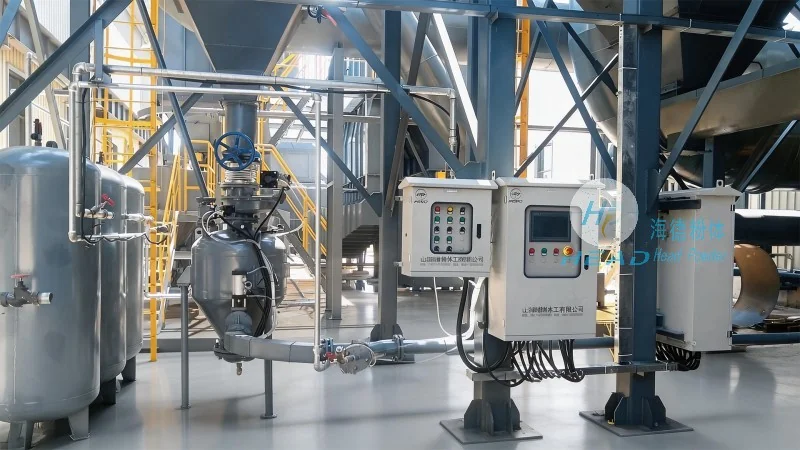
The tonne bag unloading station typically consists of several key components that work in concert to achieve seamless material transfer. The primary elements include a bag opening mechanism, a hopper or receiving hopper to collect the material, a conveyor system (such as a screw conveyor or pneumatic conveyor) to transport the material to the next stage, and a dust collection system to maintain air quality and prevent contamination. Each component is engineered to handle the specific challenges associated with bulk powder handling, including material flow control, dust suppression, and structural integrity. The bag opening mechanism, often a hydraulic or mechanical device, is designed to safely and efficiently open the tonne bag without damaging the material inside. The receiving hopper is typically equipped with a sloped bottom to ensure smooth material flow into the conveyor system. The conveyor system may vary depending on the material properties—for instance, a screw conveyor is suitable for free-flowing powders, while a pneumatic conveyor is ideal for dusty or fine powders. The dust collection system, which may include filters and fans, is critical for maintaining a safe and clean environment by capturing airborne particles and returning clean air to the workspace.
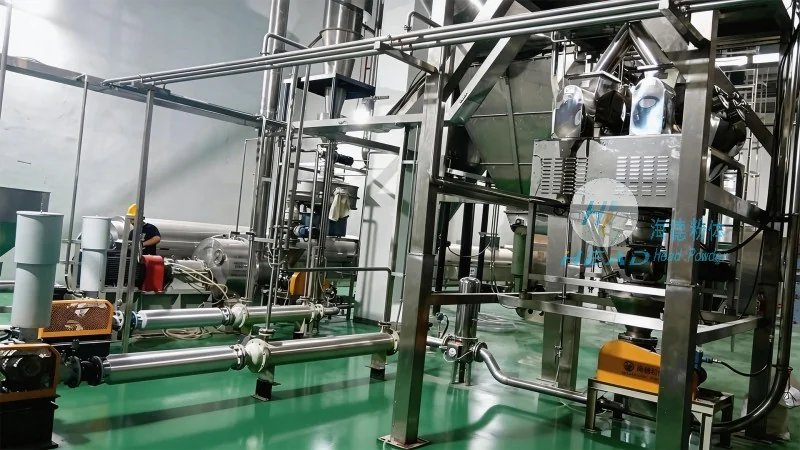
The design of a tonne bag unloading station powder conveying line is guided by several fundamental principles aimed at maximizing efficiency, safety, and durability. One key principle is the use of appropriate material handling equipment that minimizes the risk of material degradation or contamination. For example, the hopper and conveyor components are often constructed from materials resistant to the specific powders being handled, such as stainless steel or specialized plastics, to prevent chemical reactions or material buildup. Another critical principle is the incorporation of dust control measures, including sealed hoppers, air filtration systems, and explosion-proof designs, to ensure compliance with safety regulations and maintain a clean working environment. The system is also designed with considerations for material flow, ensuring that the conveyor speed and hopper geometry are optimized to prevent blockages or agglomeration. Additionally, the design incorporates features to enhance operational safety, such as emergency stop buttons, interlocks, and visual indicators that alert operators to potential issues.
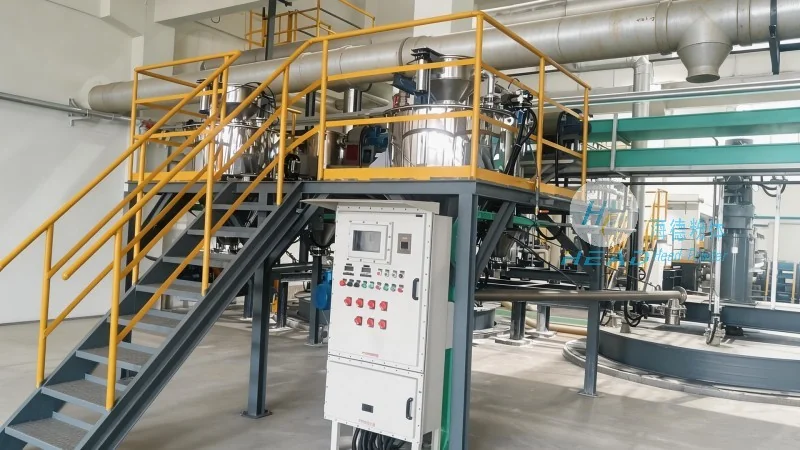
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial powder handling solutions, specializes in designing and manufacturing tonne bag unloading stations tailored to the unique needs of various industries. With years of experience in the field, HeadPowder combines advanced engineering with practical application knowledge to deliver systems that meet the highest standards of performance and reliability. The company's team of experts works closely with clients to understand their specific material handling challenges and develop customized solutions that optimize workflow and reduce operational costs. HeadPowder's commitment to quality is evident in their use of high-grade materials and rigorous testing protocols, ensuring that each system is built to withstand the demands of continuous industrial use. The company also provides comprehensive support, including installation, maintenance, and training, to help clients maximize the lifespan and efficiency of their powder handling equipment.
HeadPowder understands that each industrial application has distinct requirements, which is why their tonne bag unloading stations are designed with flexibility and adaptability in mind. The systems can be customized to accommodate various bag sizes, material types, and processing needs, ensuring seamless integration with existing production lines or new installations. For example, the company offers options for different bag opening mechanisms, conveyor types, and dust control systems, allowing clients to select the configuration that best suits their operational environment. Additionally, HeadPowder provides integration services to ensure that the unloading station works in harmony with other equipment, such as mixers, classifiers, or storage silos, creating a cohesive and efficient material handling system. This integration capability is particularly valuable for large-scale operations where multiple processing steps are involved, as it streamlines the overall workflow and reduces the need for manual material transfer.
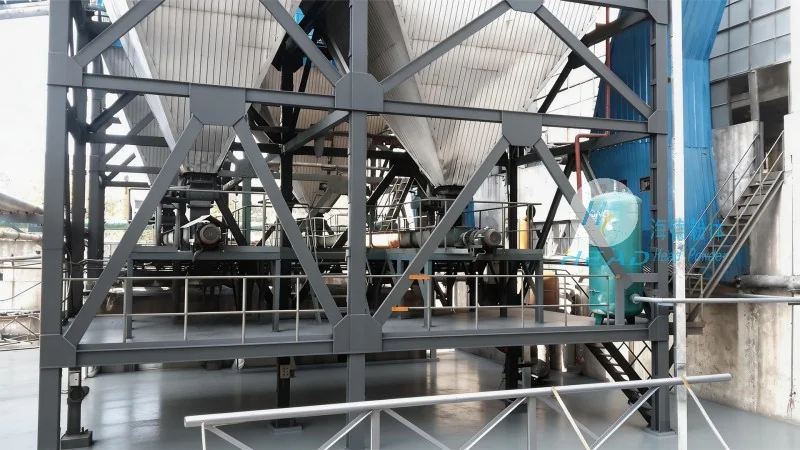
Implementing a tonne bag unloading station powder conveying line offers numerous benefits for industrial operations. By automating the material transfer process, businesses can reduce labor costs and minimize the risk of human error. The system also enhances safety by eliminating the need for manual handling of heavy bags and reducing exposure to dust and other airborne particles. Furthermore, the consistent and controlled flow of material improves the quality and consistency of downstream processes, leading to higher product quality and reduced waste. The durability and low maintenance requirements of these systems also contribute to long-term cost savings and operational efficiency. For example, a well-designed tonne bag unloading station can operate for years with minimal downtime, providing a reliable solution for continuous production. Additionally, the system's ability to handle large volumes of material efficiently helps businesses meet production targets and improve overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top