For industrial applications involving the transport of coal particle materials, pneumatic conveying systems offer an efficient and reliable solution. Understanding the working principle and key characteristics of such systems is crucial for selecting the right equipment and optimizing operational performance. This article provides an in-depth exploration of the mechanisms behind pneumatic conveying for coal particles, highlighting its advantages and practical considerations.
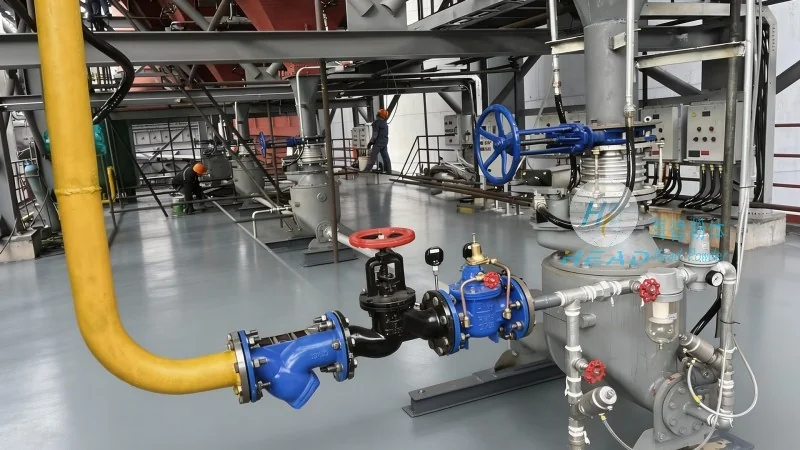
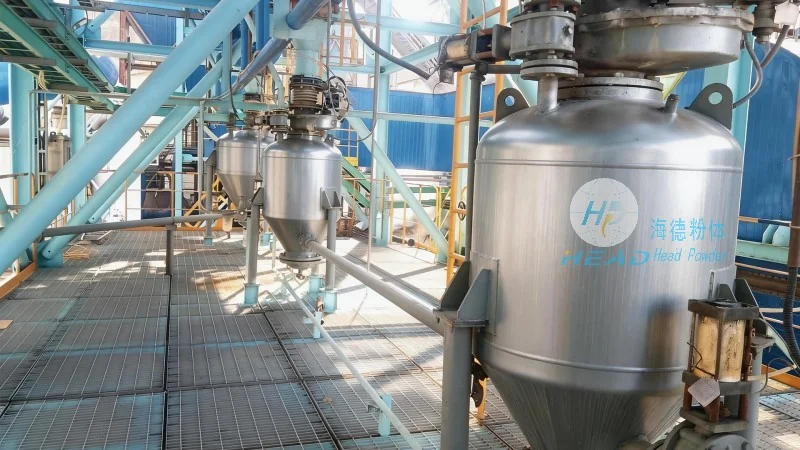
Pneumatic conveying operates by using a gas stream, typically air or a mixture of air and other gases, to transport solid particles through a pipeline. In the case of coal particle materials, the process involves several key steps that ensure efficient material movement. First, the coal particles are introduced into the conveying system, often through a hopper or feeder, where they are drawn into the pipeline by the moving air stream. The air flow creates a negative pressure or positive pressure environment, depending on the system design, which propels the particles forward. The velocity of the air is critical; it must be sufficient to overcome the gravitational forces acting on the particles and maintain them in suspension within the pipeline. As the particles travel through the system, they may encounter various components such as bends, expansions, or filters, which are designed to maintain the flow and prevent blockages. The entire process is controlled by a system of valves, regulators, and sensors that monitor pressure, flow rate, and particle concentration, ensuring stable and consistent operation.
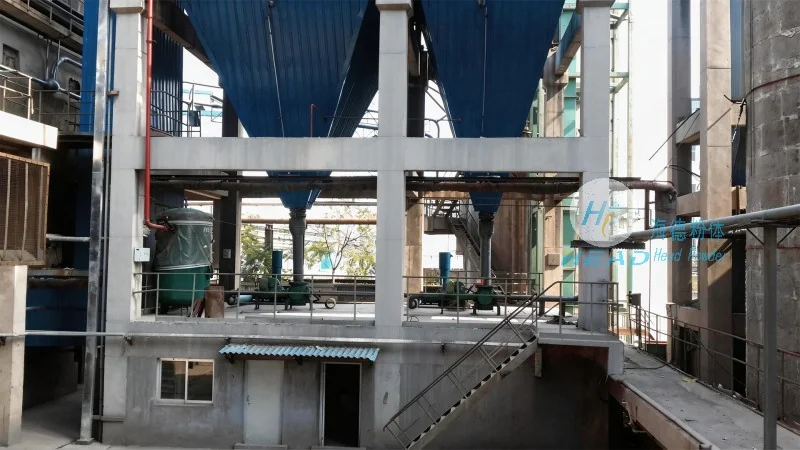
When evaluating pneumatic conveying systems for coal particle applications, several distinct characteristics stand out as advantages. One primary benefit is the ability to transport materials over long distances without the need for intermediate transfer points or mechanical components, reducing downtime and maintenance requirements. The system also offers flexibility in terms of layout, as pipelines can be installed in various configurations to accommodate complex plant layouts. Additionally, pneumatic conveying is well-suited for handling materials with varying particle sizes and moisture content, as the air flow can adapt to these variations while maintaining efficient transport. Another important characteristic is the system's ability to handle abrasive or corrosive materials, as the internal components are designed to withstand the wear and tear associated with coal particles. However, it is essential to consider the energy consumption of pneumatic conveying, as it typically requires more power than other transport methods. The system's performance is also influenced by factors such as particle density, size distribution, and the presence of dust, which can affect the air flow and overall efficiency. Proper design and maintenance are crucial to mitigate these challenges and ensure optimal performance.
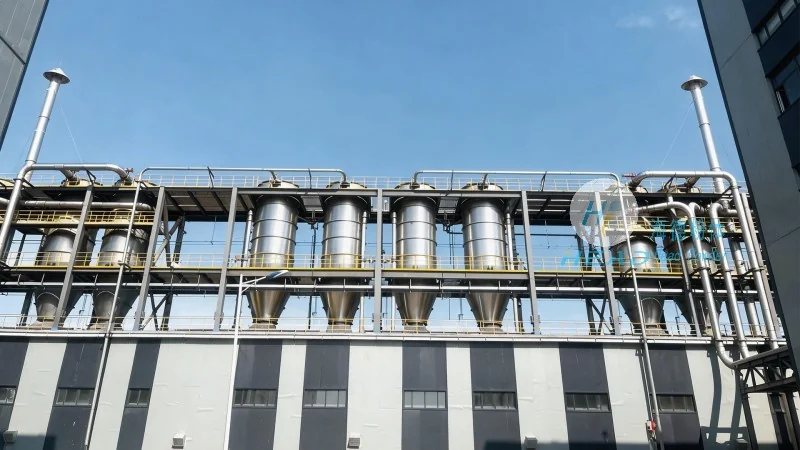
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions for material handling and processing. With a focus on innovation and quality, the company specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the needs of various industries, including coal processing. HeadPowder's expertise lies in developing customized solutions that address the unique challenges of material transport, ensuring reliable and efficient operations for clients. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the field of industrial material handling. HeadPowder is headquartered in Shandong, China, where it operates from its facilities, providing local support and service to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top