Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of bulk material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for ammonia fertilizer applications. With a focus on efficiency, safety, and reliability, the company's expertise lies in delivering customized solutions that meet the unique demands of fertilizer processing and distribution industries.
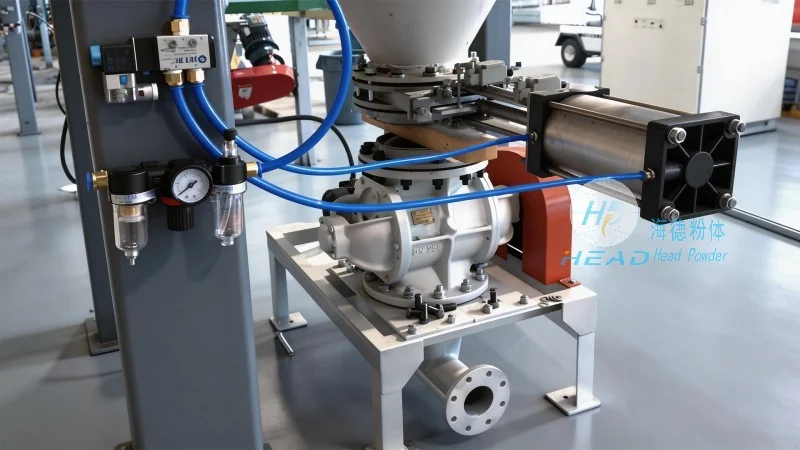
The ammonia fertilizer powder pneumatic conveying system operates on the fundamental principle of transporting dry bulk materials through a pressurized or vacuumed air stream. In this system, the fertilizer powder is introduced into a conveying line where it is suspended and propelled by the moving air. The process typically involves a combination of positive pressure (blower-driven) or negative pressure (vacuum) systems, depending on the specific application requirements. The core components include a feeding hopper, a rotary airlock valve, a conveying pipeline, a separation unit, and a discharge device. The feeding hopper ensures a consistent flow of fertilizer powder into the system, while the rotary airlock valve prevents backflow and maintains pressure integrity. The conveying pipeline transports the powder mixture, and the separation unit, such as a cyclone or bag filter, separates the powder from the air stream, allowing for clean air discharge and powder collection. This mechanism enables the efficient and continuous movement of ammonia fertilizer from the storage area to processing or packaging equipment.
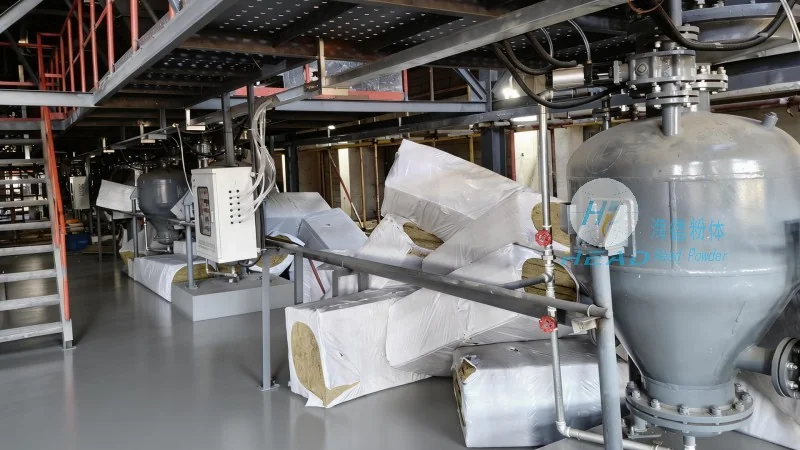
The working scenario characteristics of the ammonia fertilizer powder pneumatic conveying system are tailored to the specific operational needs of fertilizer production and handling facilities. These systems are commonly employed in scenarios where bulk ammonia fertilizer needs to be transferred over medium to long distances within a plant or between different processing stages. For instance, in large-scale fertilizer manufacturing plants, the system efficiently moves raw ammonia fertilizer from storage silos to mixing and granulation units, ensuring a seamless and uninterrupted production flow. Additionally, the system is suitable for transferring finished fertilizer products from the production line to storage silos or packaging areas, minimizing manual handling and reducing the risk of material loss or contamination. The characteristics of the system include high conveying capacity, which allows for the rapid movement of large volumes of fertilizer, and the ability to handle fine or cohesive powders without clogging, thanks to the optimized design of the conveying line and separation equipment. Furthermore, the system operates with minimal environmental impact, as it uses enclosed pipelines to prevent dust emissions and maintain a clean working environment. This makes it an ideal solution for facilities that prioritize safety and compliance with environmental regulations.
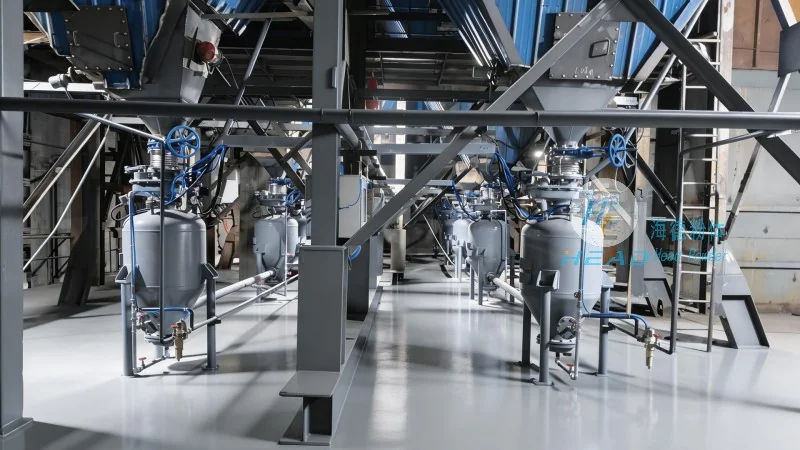
The ammonia fertilizer powder pneumatic conveying system is particularly well-suited for various operational scenarios within the fertilizer industry. One common application is the internal transport of raw materials within a fertilizer plant, where the system efficiently moves ammonia fertilizer from storage silos to the production line, reducing the need for manual handling and improving overall productivity. Another scenario involves the transfer of finished fertilizer products from the production area to the packaging and shipping facilities, ensuring that the product reaches its destination in a timely and efficient manner. The system's ability to handle different particle sizes and moisture contents of ammonia fertilizer makes it versatile for various product types, including urea, ammonium nitrate, and other nitrogen-based fertilizers. Operational advantages of the system include reduced labor costs due to automated material handling, improved product quality through minimized exposure to air and moisture, and enhanced safety by eliminating the need for manual loading and unloading of bulk materials. The system also contributes to energy efficiency by optimizing air flow and pressure, which reduces operational costs and environmental impact. Overall, the ammonia fertilizer powder pneumatic conveying system offers a reliable and efficient solution for bulk material handling in the fertilizer industry, aligning with the operational requirements of modern production facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top