Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and implementation of advanced powder handling systems, with a particular focus on systems for handling ammonium nitrate. The company leverages extensive industry experience to develop solutions that address the unique challenges posed by this critical industrial chemical, ensuring safe, efficient, and reliable material transport. This article delves into the working principle and key features of such systems, illustrating how they are engineered to meet the demands of modern industrial applications.
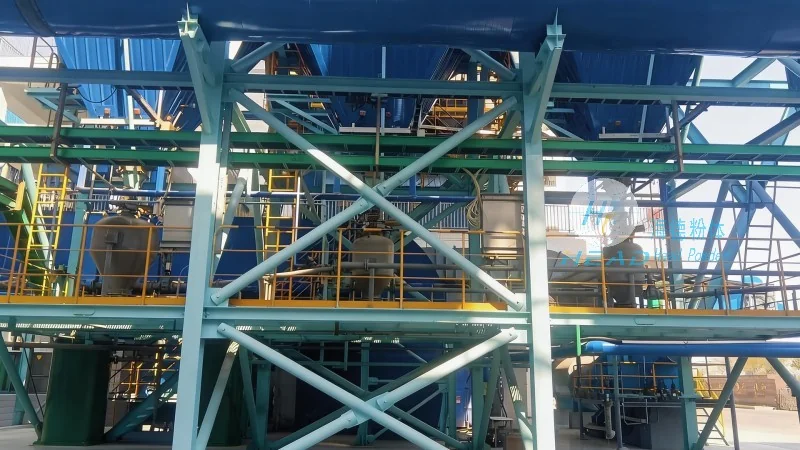
The working principle of an ammonium nitrate powder handling system involves a systematic sequence of operations designed to manage the material from its storage point to its final destination. The process typically begins with the storage of ammonium nitrate in a specialized silo or hopper, where the material is held under controlled conditions to prevent caking, moisture absorption, or degradation. From the storage vessel, the system uses a combination of mechanical and pneumatic equipment to transport the powder. For short-distance or horizontal/vertical transport, components such as screw conveyors, belt conveyors, or bucket elevators may be employed. For longer distances or when navigating complex pathways, a pneumatic conveying system—often utilizing positive displacement blowers or rotary airlocks—becomes the primary method. This system draws the powder into a sealed pipeline using compressed air, ensuring minimal exposure to the environment and reducing the risk of dust dispersion.
A critical component of the working principle is the integration of safety and control mechanisms tailored to the hazardous nature of ammonium nitrate. The system incorporates robust dust collection and explosion prevention measures. For example, sealed hoppers and conveyors are used to minimize dust leakage, while explosion relief valves and flame arrestors are installed to protect the system from potential ignition sources. The control system, equipped with sensors and monitoring devices, continuously tracks parameters such as pressure, temperature, and flow rate, ensuring that the operation remains within safe operational limits. Automated shutdown protocols are also implemented to respond to abnormal conditions, such as excessive pressure or temperature spikes, thereby preventing accidents and protecting personnel and equipment.
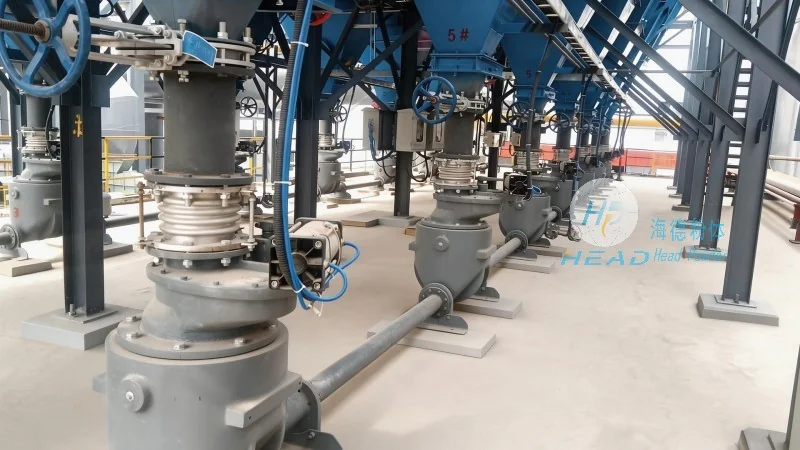
Ammonium nitrate powder handling systems from Shandong HeadPowder Engineering Co., Ltd. are distinguished by several key features that enhance their performance, safety, and adaptability. First, the systems are engineered for high efficiency and low material loss. Optimized conveying velocities and appropriate equipment selection reduce the risk of material degradation and ensure that the majority of the ammonium nitrate reaches its intended destination without spillage or contamination. This efficiency is further improved by the use of precise control mechanisms that adjust flow rates based on real-time demand, minimizing waste and maximizing throughput.
Second, the systems prioritize safety through multiple layers of protection. This includes the use of explosion-proof motors and electrical components, as well as the incorporation of intrinsically safe systems that prevent electrical sparks from igniting dust clouds. Additionally, the design incorporates features such as grounding and bonding to eliminate static electricity buildup, a common hazard with powders like ammonium nitrate. The system's monitoring capabilities, including real-time pressure and temperature sensors, provide early warnings of potential issues, allowing for proactive maintenance and reducing the risk of catastrophic failures.
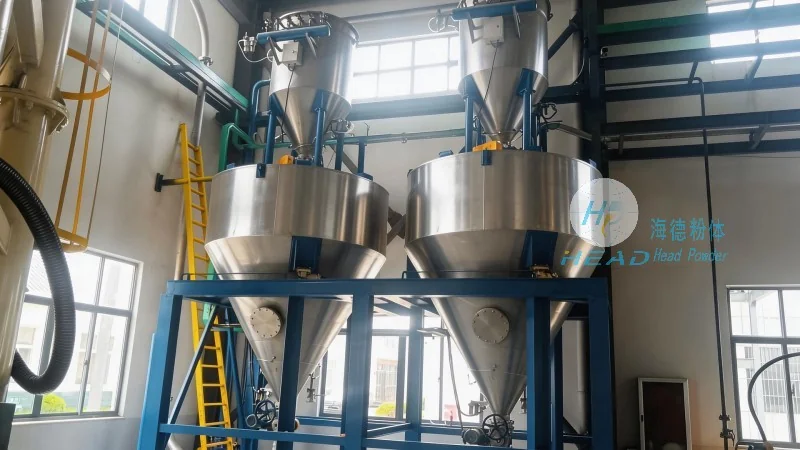
Third, the systems are highly customizable and modular, enabling them to adapt to a wide range of industrial requirements. Whether the application involves short-distance transport within a fertilizer plant or long-distance delivery to a storage facility, the system can be configured with the appropriate equipment and controls. The modular design allows for easy expansion or modification as production needs evolve, providing flexibility and cost-effectiveness over the long term. This adaptability also extends to the handling of different particle sizes or moisture contents, as the system can be adjusted to maintain optimal flow characteristics.
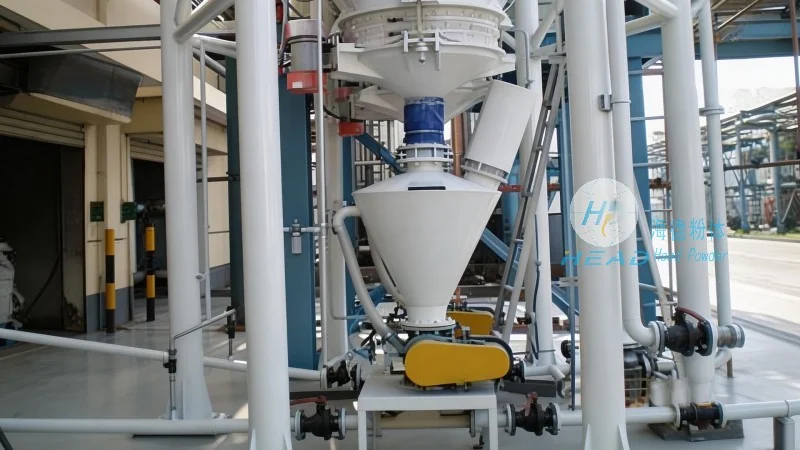
Fourth, the systems are built with durability and low maintenance in mind. Materials such as stainless steel or corrosion-resistant alloys are used for components that come into direct contact with the ammonium nitrate, ensuring resistance to wear and corrosion. The design minimizes points of friction and wear, reducing the frequency of maintenance and extending the system's service life. Additionally, the system incorporates easy-to-access maintenance points and diagnostic tools, allowing for quick troubleshooting and repairs, which further enhances operational reliability.
In conclusion, the working principle and features of ammonium nitrate powder handling systems from Shandong HeadPowder Engineering Co., Ltd. reflect a comprehensive approach to addressing the unique challenges of handling this critical chemical. By combining advanced engineering with rigorous safety standards and adaptability, these systems provide a reliable solution for industries that rely on ammonium nitrate, ensuring that material transport is conducted efficiently while minimizing risks to personnel, equipment, and the environment. The result is a system that not only meets current industrial demands but also supports long-term operational success and compliance with safety regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top