Calcite powder conveying systems are essential for the efficient handling and transportation of calcite powder in industrial applications. These systems are designed to manage the unique properties of calcite, such as its fine particle size and potential for dust generation, ensuring safe and reliable operation. The following sections will explore the working principle and key features of such systems, providing a comprehensive understanding of their functionality and benefits.
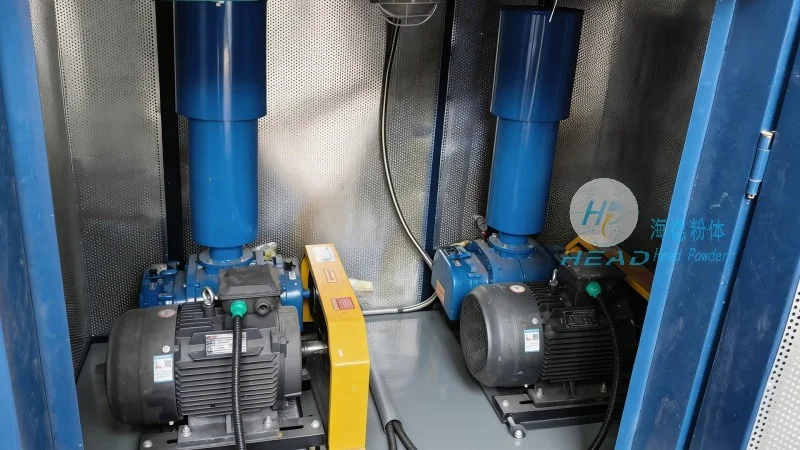
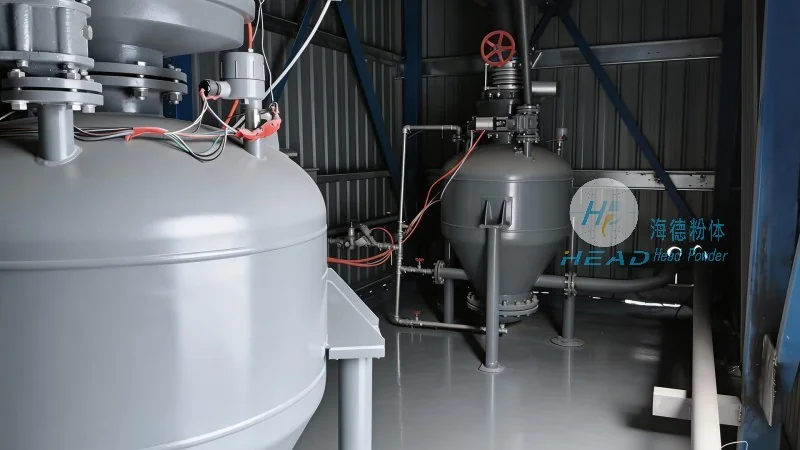
The working principle of a calcite powder conveying system centers on the integration of feeding, conveying, and discharge mechanisms tailored to the unique characteristics of calcite powder. The process typically starts with the material being introduced into a hopper or bulk feeder, where it is stored and prepared for transport. The feeder ensures a consistent flow rate by regulating the amount of powder entering the system, preventing overloading or underflow. From the feeder, the powder is transferred to the conveying component, which can be either pneumatic or mechanical. Pneumatic conveying systems utilize compressed air to create a flow that carries the powder through a pipeline. In this method, the powder is suspended in the air stream and transported to the destination. The system may employ either suction or pressure modes, depending on the layout and distance of the conveying line. For longer distances or higher material volumes, pressure systems are often preferred, as they can maintain a consistent flow without the need for additional vacuum equipment. Mechanical conveying systems, such as screw conveyors or bucket elevators, rely on mechanical force to move the powder. Screw conveyors use rotating screws to push the material forward, while bucket elevators use buckets attached to a chain or belt to lift and transport the powder vertically. These mechanical systems are particularly effective for handling materials with higher bulk densities or those that are more prone to clogging. After the powder is conveyed to the destination, it is discharged into a storage silo or processing unit. The discharge mechanism is designed to ensure a smooth and controlled release of the material, preventing spillage or blockages. The entire system is often equipped with sensors and control panels that monitor parameters such as pressure, flow rate, and temperature, allowing for real-time adjustments and maintenance. This integrated approach ensures that the calcite powder is handled safely and efficiently, minimizing downtime and maximizing productivity.
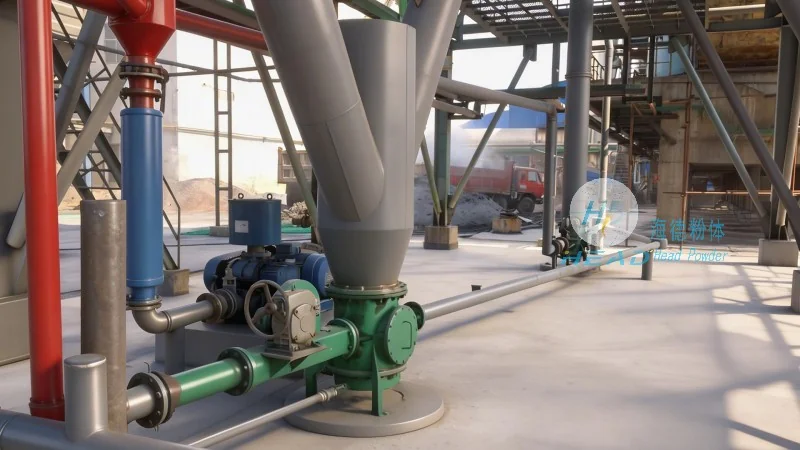
Calcite powder conveying systems are distinguished by a range of features that enhance their performance, reliability, and adaptability. One of the most critical features is their ability to handle fine, cohesive powders without causing blockages or agglomeration. The systems incorporate specialized components such as flexible hoses, wear-resistant liners, and anti-static coatings to prevent material buildup and ensure smooth flow. These features are particularly important for calcite, which can be prone to sticking to surfaces due to its fine particle size and moisture content. Another key feature is the system's energy efficiency. Advanced designs, such as variable speed drives and optimized air flow, reduce energy consumption while maintaining high throughput. This not only lowers operational costs but also aligns with environmental sustainability goals. The systems are also designed for easy maintenance and cleaning, with features like quick-release fittings and removable components that allow for routine inspections and cleaning without extensive downtime. Additionally, the equipment is constructed from high-quality materials, including stainless steel and corrosion-resistant alloys, ensuring durability and resistance to the chemical properties of calcite. These materials also contribute to the system's longevity, reducing the need for frequent replacements and repairs. Furthermore, the systems are equipped with safety features that comply with industrial standards, such as emergency stop buttons, overpressure relief valves, and dust suppression systems. These features protect both operators and the environment from potential hazards, ensuring a safe working environment. The combination of these features makes calcite powder conveying systems highly effective in industrial settings, where consistent and reliable material handling is essential for operational success.
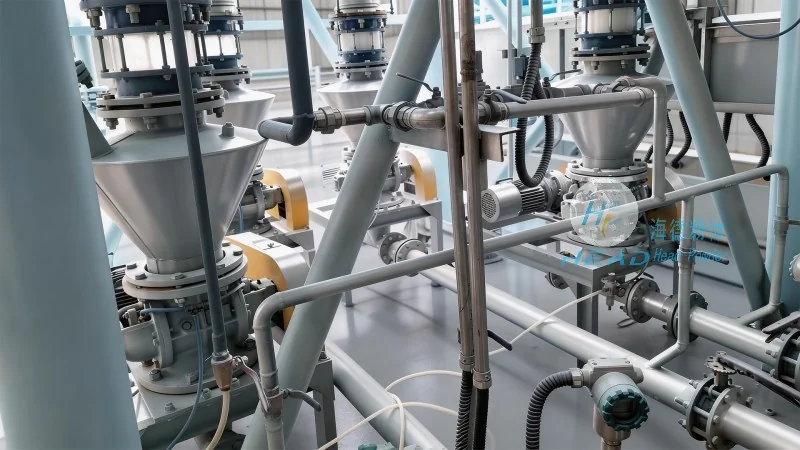
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced powder handling solutions. The company specializes in the design, development, and installation of conveying systems for various industrial applications, with a particular focus on calcite and other fine powders. Headpowder's headquarters and manufacturing facilities are located in Shandong, China, where it operates a state-of-the-art production facility equipped with modern machinery and skilled workforce. The company's team of engineers and technicians brings extensive experience in powder technology, ensuring that each system is tailored to meet the specific requirements of clients. By leveraging cutting-edge technology and rigorous quality control processes, headpowder delivers systems that are reliable, efficient, and cost-effective. The company's commitment to innovation is evident in its continuous research and development efforts, which focus on improving system performance, reducing energy consumption, and enhancing safety features. Headpowder also provides comprehensive after-sales support, including installation, training, and maintenance services, ensuring that clients receive long-term value from their investment. With a strong reputation for quality and customer satisfaction, headpowder has established itself as a trusted partner in the powder handling industry, serving clients across various sectors including mining, chemicals, and food processing. The company's dedication to excellence and customer-centric approach has enabled it to maintain a competitive edge in the market, making it a preferred choice for businesses seeking reliable and efficient calcite powder conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top