Feed powder conveying systems are essential in the agricultural and animal feed industries, designed to efficiently transport bulk feed powders from storage to processing or feeding points. Understanding the working principle and key features of such systems is crucial for optimizing operational efficiency and ensuring reliable material handling. This article provides an in-depth look at the mechanics behind these systems and the attributes that define their performance, with a focus on the solutions offered by Shandong HeadPowder Engineering Co., Ltd. (headpowder).
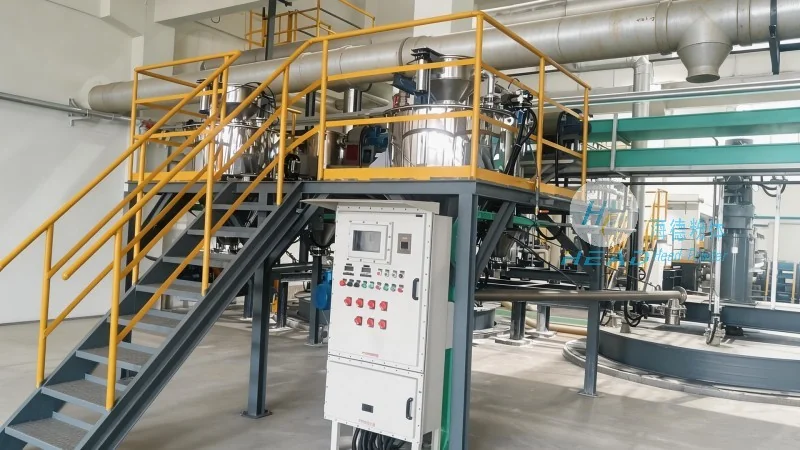
The core working principle of feed powder conveying systems revolves around the use of mechanical or pneumatic methods to move dry, free-flowing feed powders. These systems typically consist of components like hoppers, conveyors, and control mechanisms that work in tandem to ensure smooth material flow. In mechanical systems, such as screw conveyors or belt conveyors, the feed is moved by rotating parts that create a continuous flow path. The hoppers collect the feed powder, and the conveyor transports it to the desired location. Pneumatic systems, on the other hand, utilize air pressure to transport the feed powder through pipes, where the material is carried by air currents. Both methods are engineered to handle the specific characteristics of feed powders, including their density, moisture content, and flowability, to prevent issues like clogging or degradation.
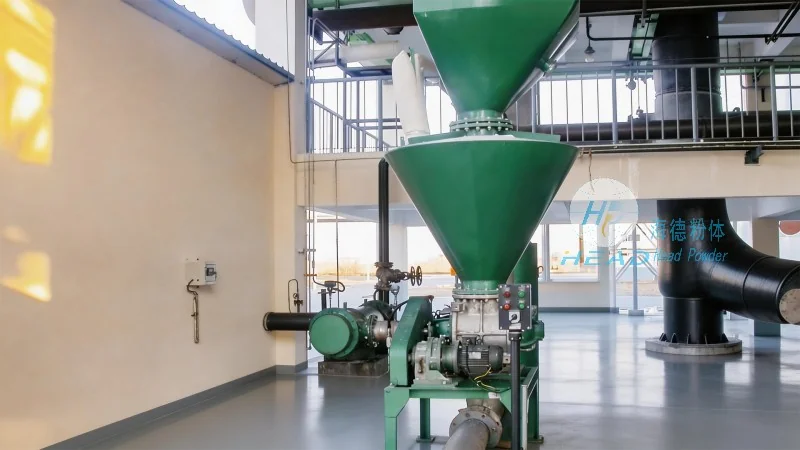
Several key features distinguish effective feed powder conveying systems, each contributing to their overall performance and reliability. One of the primary features is the ability to handle varying feed characteristics, such as different particle sizes and moisture levels, without compromising efficiency. This adaptability is achieved through adjustable components like variable speed drives and customizable hopper designs. Another critical feature is the system's durability and resistance to wear and tear, as feed powders can be abrasive and cause mechanical stress on equipment. High-quality materials, such as stainless steel or corrosion-resistant alloys, are often used in the construction of these systems to ensure longevity. Additionally, modern feed powder conveying systems incorporate advanced control technologies, including sensors and automation, to monitor flow rates, detect blockages, and adjust operations in real-time. This integration enhances operational safety and reduces downtime. Energy efficiency is also a notable feature, with many systems designed to minimize power consumption while maintaining optimal performance. The design of these systems also prioritizes hygiene and easy maintenance, with features like easy-to-clean surfaces and accessible components that facilitate regular upkeep.
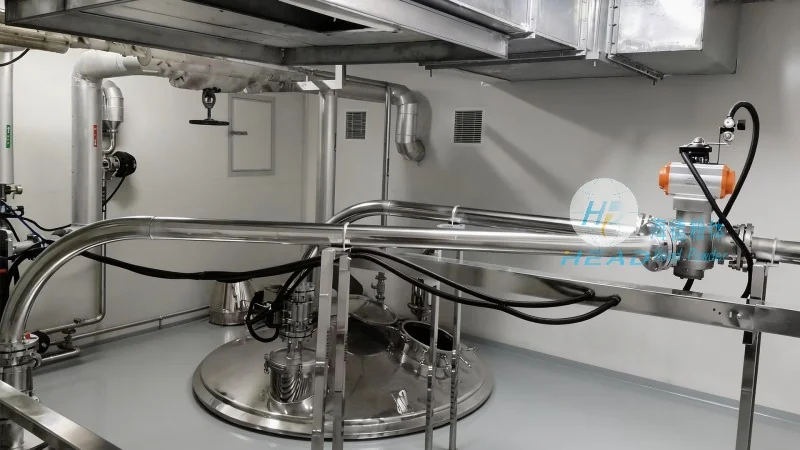
Feed powder conveying systems are widely used in various stages of feed production, from raw material handling to final product distribution. In raw material storage, these systems help move bulk feed ingredients, such as grains and pellets, from silos or storage bins to processing lines. During the processing stage, they transport intermediate products, like mixed feed or pelleted feed, to packaging or feeding stations. The systems are also integral in animal feed operations, where they deliver feed to livestock or poultry houses. The adaptability of these systems allows them to be integrated into existing feed production lines, either as standalone units or as part of larger automated systems. This integration ensures seamless material flow and reduces manual handling, which can be labor-intensive and prone to errors. The reliability of feed powder conveying systems is essential for maintaining consistent feed quality and meeting production targets. By efficiently transporting feed powders, these systems contribute to the overall productivity and profitability of feed manufacturing operations.
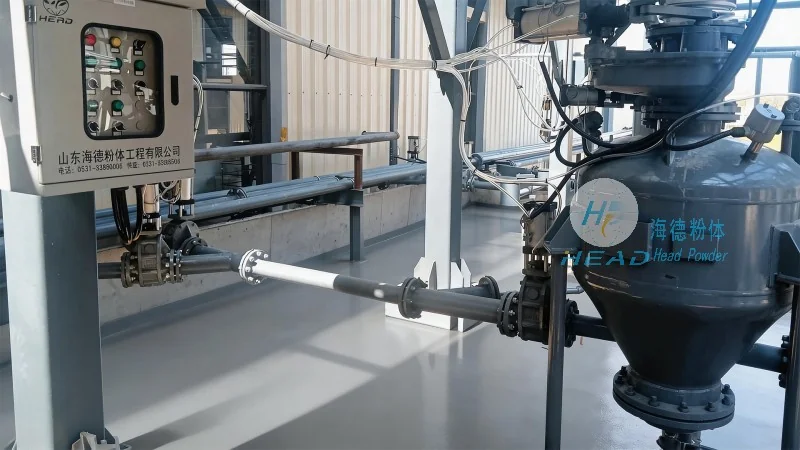
Implementing feed powder conveying systems offers numerous advantages for feed producers. The most significant advantage is the improvement in operational efficiency, as these systems can handle large volumes of feed powder with minimal labor input. This efficiency translates to cost savings and increased productivity. Another advantage is the reduction in material loss and contamination, as the enclosed design of many systems prevents dust and spillage, which can affect feed quality and safety. The systems also enhance safety in the workplace by minimizing manual handling of heavy or bulky feed powders, reducing the risk of accidents and injuries. Furthermore, the durability and low maintenance requirements of modern systems mean fewer breakdowns and lower repair costs over time. The ability to customize systems to specific feed characteristics ensures optimal performance and extends the lifespan of the equipment. These advantages make feed powder conveying systems a valuable investment for feed manufacturers looking to enhance their operations and maintain high standards of feed quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top