When it comes to the efficient and reliable transportation of sodium bicarbonate powder, understanding the underlying mechanisms and key features of the handling systems is crucial. This article delves into the working principle and characteristics of sodium bicarbonate powder conveying solutions, providing insights into how these systems operate and the advantages they offer in industrial applications.
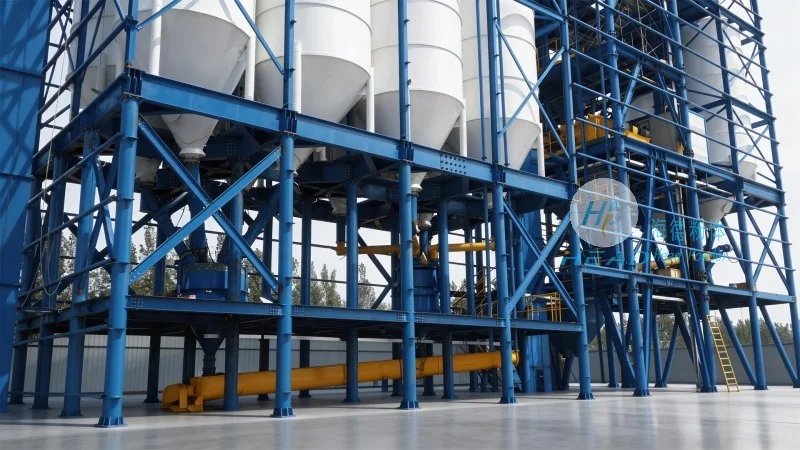
Sodium bicarbonate, commonly known as baking soda, is a widely used chemical compound in various industries, including food processing, pharmaceuticals, and chemical manufacturing. The need for effective powder handling and conveying systems arises from the challenges associated with transporting fine powders like sodium bicarbonate, which can be prone to issues such as caking, segregation, and dust generation. To address these challenges, specialized powder handling solutions are employed, ensuring safe, efficient, and cost-effective material movement within industrial processes.
The working principle of sodium bicarbonate powder handling systems typically involves the use of either pneumatic (air-driven) or mechanical (mechanical-driven) conveying methods. Pneumatic conveying systems utilize compressed air to transport the powder through a network of pipes, while mechanical systems rely on screw conveyors, belt conveyors, or bucket elevators to move the material. For sodium bicarbonate, which is a relatively light and fine powder, pneumatic conveying is often preferred due to its ability to handle high volumes with minimal equipment and reduced risk of product degradation.
In pneumatic conveying, the powder is introduced into a hopper or feeder, where it is then drawn into a pipeline by the pressure differential created by the compressed air. The air and powder mixture travels through the pipeline, with the air providing the necessary force to move the powder. The system may include components such as rotary valves, filters, and dust collectors to ensure proper flow control and to prevent dust emissions. Mechanical conveying systems, on the other hand, use rotating screws or belts to push the powder along a fixed path, which is particularly suitable for applications requiring direct contact with the material or for handling larger quantities of bulk material.
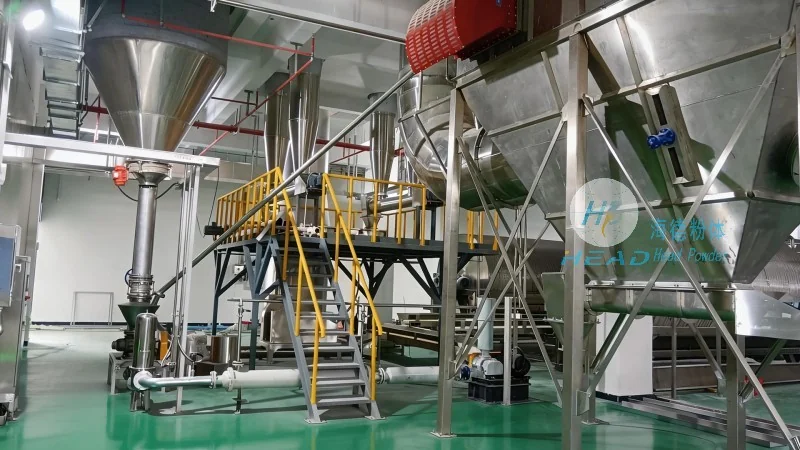
Effective sodium bicarbonate powder handling solutions exhibit several key characteristics that make them suitable for industrial applications. Firstly, they are designed to minimize product degradation, ensuring that the chemical properties of sodium bicarbonate are preserved during transportation. This is achieved through the use of gentle handling mechanisms, such as low-speed screw conveyors or air cushioning in pneumatic systems, which prevent excessive friction or impact that could alter the powder's quality.
Secondly, these systems are engineered for high efficiency and low energy consumption. By optimizing the flow rates and pressure differentials in pneumatic systems or the speed and torque of mechanical components, the overall operational costs are reduced. Additionally, the ability to handle large volumes of powder in a continuous manner enhances production throughput, making the systems ideal for high-demand industrial processes.
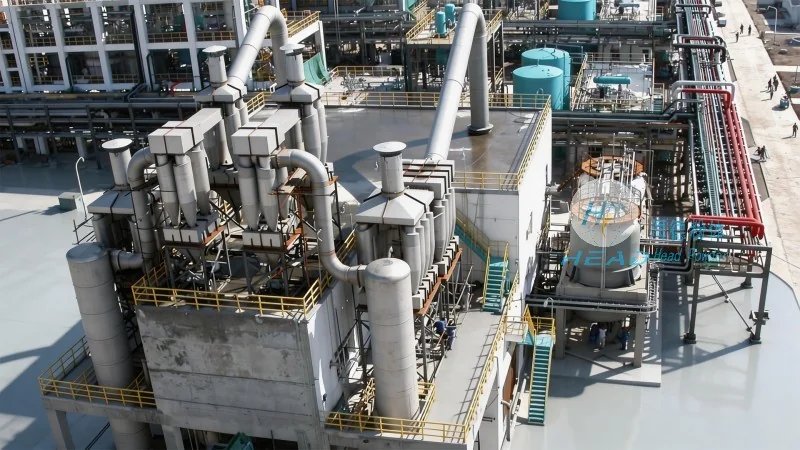
Thirdly, sodium bicarbonate powder handling systems are built with safety and environmental considerations in mind. Dust containment measures, such as sealed hoppers and dust collectors, are integrated to prevent airborne dust from contaminating the environment or posing health risks to personnel. The systems also often include explosion-proof designs, as sodium bicarbonate is a combustible material under certain conditions, ensuring compliance with safety regulations and minimizing the risk of accidents.
Sodium bicarbonate powder handling solutions are widely used across various industries due to their versatility and effectiveness. In the food industry, for example, these systems are employed to transport sodium bicarbonate used as a leavening agent or pH adjuster in baking and food processing. In pharmaceutical manufacturing, the systems ensure the safe and hygienic handling of sodium bicarbonate used in drug formulations, maintaining product purity and quality. Additionally, in chemical manufacturing, the systems are utilized for the transportation of sodium bicarbonate in production lines, supporting the synthesis of other chemical compounds and ensuring smooth operational flow.
Understanding the working principle and characteristics of sodium bicarbonate powder handling systems is essential for optimizing industrial processes and ensuring the efficient movement of this vital chemical compound. The combination of pneumatic and mechanical conveying technologies, along with advanced design features, enables the reliable and safe handling of sodium bicarbonate powder in various applications. As a leading provider of powder handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in developing customized systems tailored to the specific needs of clients, leveraging years of expertise in the field to deliver high-quality, efficient, and cost-effective solutions for sodium bicarbonate powder transportation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top