High-calcium powder, often used in industrial applications such as food processing, pharmaceutical manufacturing, and construction materials, requires specialized handling due to its unique physical properties. The efficient and safe transportation of these powders is crucial for maintaining product quality and operational efficiency. This article explores the working principle and key characteristics of high-calcium powder conveying systems, providing insights into their design, functionality, and practical applications.
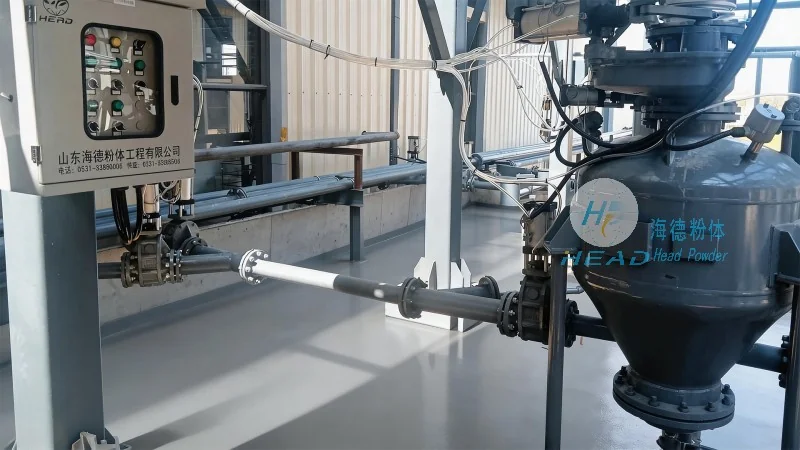
High-calcium powder conveying systems typically operate on the principle of mechanical or pneumatic transport, depending on the specific requirements of the material and the system design. Mechanical conveyors, such as screw conveyors, belt conveyors, and bucket elevators, use mechanical energy to move the powder through a closed or open system. These systems are particularly effective for materials with moderate to high bulk density and are commonly used in industries where continuous flow is essential.
Pneumatic conveying systems, on the other hand, utilize air or other gases to transport the powder through a pipeline network. This method is ideal for materials that are sensitive to moisture or contamination, as the enclosed system minimizes exposure to external factors. The working principle involves generating a pressure differential to move the powder, with options ranging from low-pressure (trunk and branch) to high-pressure (positive displacement) systems. The choice of system depends on factors like material flow rate, distance, and the need for dust control.
Several key characteristics define high-calcium powder conveying systems, each tailored to address the specific challenges of handling such materials. One of the primary characteristics is the ability to maintain a consistent flow rate, which is critical for process control and product quality. The systems are designed to minimize material degradation, such as caking or agglomeration, which can occur due to moisture absorption or temperature changes.
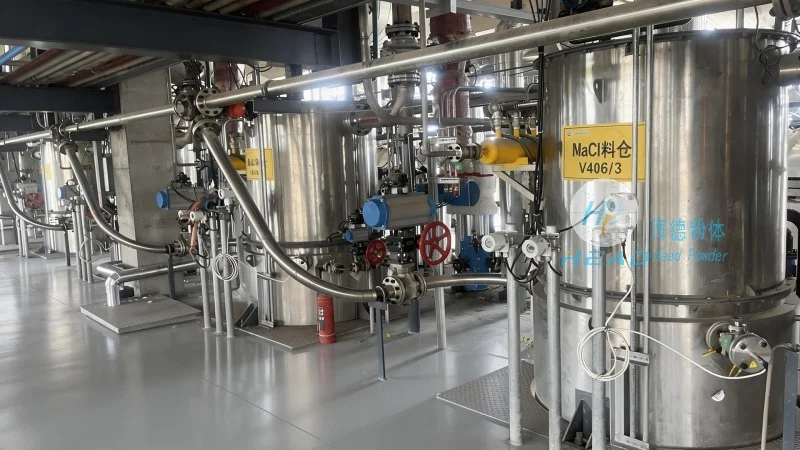
Another important characteristic is the system's adaptability to different operating conditions. High-calcium powders may vary in particle size, density, and moisture content, requiring flexible conveying solutions. Modern systems often incorporate variable speed drives and adjustable feed mechanisms to accommodate these variations, ensuring smooth and reliable operation.
Dust control is a critical characteristic, as high-calcium powders can be fine and generate significant dust during handling. Conveying systems are equipped with dust collection and filtration systems to comply with environmental regulations and ensure workplace safety. The design of the system, including sealed components and proper ventilation, helps to minimize dust emissions and maintain a clean working environment.
The technical aspects of high-calcium powder conveying systems involve several components that work in harmony to achieve efficient transport. The feed system, which may include hoppers, feeders, or rotary valves, ensures a consistent material supply to the conveyor. The conveyor itself, whether mechanical or pneumatic, must be designed to handle the specific properties of the powder, such as its abrasiveness or tendency to stick to surfaces.
Material handling components, such as chutes and transition pieces, are crucial for directing the powder flow and preventing blockages or material degradation. The system's control system, which may include sensors, controllers, and monitoring devices, allows for real-time adjustments to maintain optimal performance. For example, level sensors can detect changes in material levels and adjust the feed rate accordingly, while pressure sensors monitor the system's performance and alert operators to potential issues.
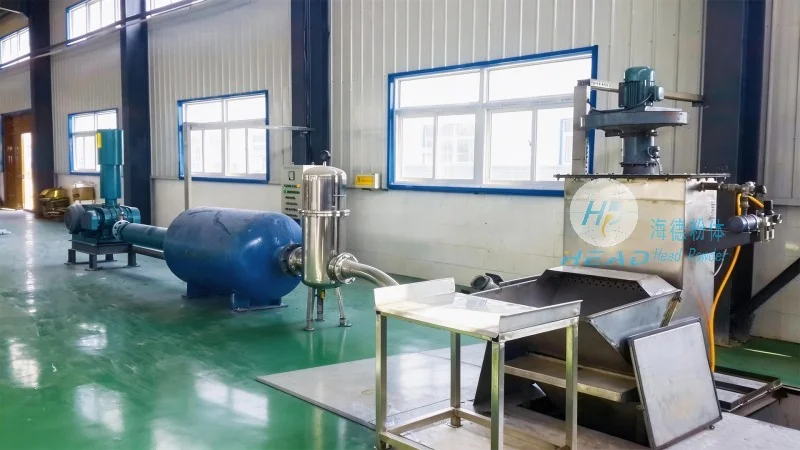
Application considerations also include the scale of operation and the specific industry requirements. For large-scale industrial applications, such as in the food or pharmaceutical sectors, the system must meet stringent quality and safety standards. This includes compliance with regulations like FDA or GMP, which may require additional features like stainless steel construction and easy cleaning.
In conclusion, high-calcium powder conveying systems are essential for the efficient and safe handling of these materials in various industrial applications. The working principle, characterized by mechanical or pneumatic transport, and the key characteristics, including flow consistency, dust control, and adaptability, make these systems reliable solutions for maintaining product quality and operational efficiency.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. With a focus on innovation and customer needs, the company provides tailored solutions for high-calcium powder conveying, ensuring that clients receive systems that meet their specific requirements and industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top