Coal and coke powder conveying systems are essential in industrial applications where fine particulate materials need to be transported efficiently and safely. These systems are designed to handle materials like coal and coke powders, which are commonly used in various industrial processes such as power generation, metallurgy, and chemical manufacturing. The effectiveness of these systems directly impacts the overall productivity and operational efficiency of the facilities they serve.
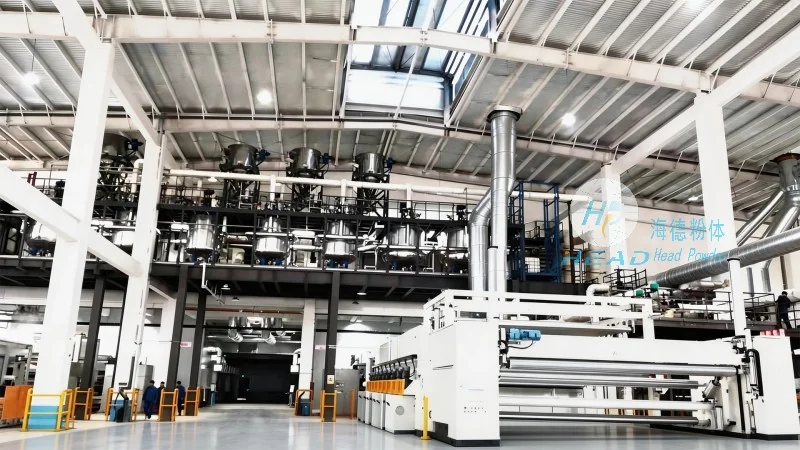
The working principle of coal and coke powder conveying systems typically involves the use of specialized equipment to transport fine particulate materials from one location to another. These systems often rely on mechanisms such as pneumatic conveying, mechanical conveying, or a combination of both, depending on the specific requirements of the application. Pneumatic conveying systems utilize air or gas to move the material through pipelines under pressure, while mechanical systems may employ screws, belts, or buckets to transfer the material along a defined path.
In pneumatic conveying, the material is first fed into a hopper or feeder, where it is then mixed with air and transported through pipelines. The pressure differential between the feeding point and the discharge point ensures the material moves smoothly through the system. Mechanical conveying systems, on the other hand, use rotating components to push or pull the material along a conveyor. For example, screw conveyors use a rotating screw to move material forward, while bucket elevators use buckets attached to a chain to lift and transport material vertically.
One of the primary characteristics of coal and coke powder conveying systems is their ability to handle large volumes of material with minimal human intervention. This automation reduces labor costs and minimizes the risk of human error, leading to more consistent and reliable material transport. Additionally, these systems are designed to maintain the integrity of the powder during transport, preventing issues such as dusting, caking, or degradation that can occur with traditional handling methods.
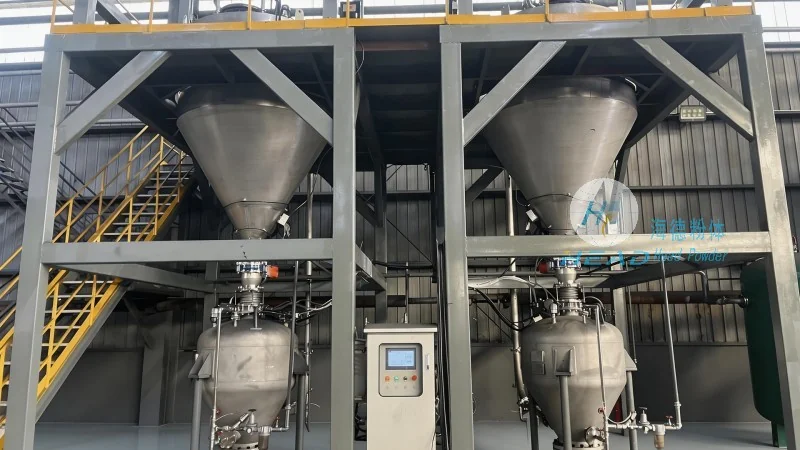
Another important characteristic is the flexibility and adaptability of these systems. They can be easily integrated into existing production lines and customized to meet specific operational needs, such as varying material flow rates or handling different particle sizes. This flexibility allows facilities to adjust their conveying systems as production demands change, ensuring optimal performance at all times.
Efficiency is a critical factor in coal and coke powder conveying systems, as the goal is to minimize downtime and maximize throughput. Advanced systems incorporate features such as real-time monitoring, automatic control, and predictive maintenance to ensure smooth operation. These features help identify potential issues before they become major problems, reducing maintenance costs and increasing the overall lifespan of the equipment.
Safety is also a top priority in these systems, especially when handling materials that may be hazardous or produce dust. Proper design and implementation of the conveying system, including dust collection and explosion-proof measures, are essential to protect workers and comply with regulatory standards. Shandong HeadPowder Engineering Co., Ltd. specializes in designing systems that meet stringent safety requirements, ensuring that facilities operate in a secure and compliant manner.
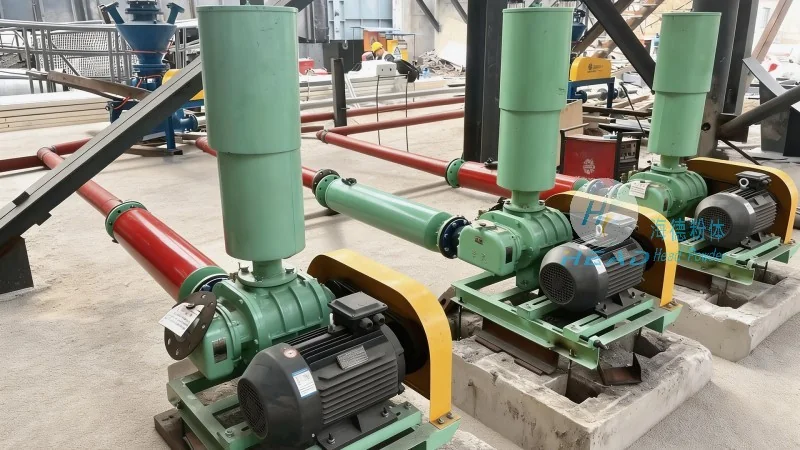
As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. understands that every coal and coke processing facility has unique requirements. The company specializes in the design, manufacturing, and implementation of advanced powder conveying solutions tailored to the specific needs of its clients. With a focus on innovation and customer satisfaction, HeadPowder leverages cutting-edge technology to develop systems that enhance productivity, reduce costs, and improve safety.
The company’s team of experts works closely with clients to assess their operational needs, identify challenges, and develop customized solutions. Whether it's a new plant setup or an upgrade to an existing system, HeadPowder provides comprehensive support from initial design through to installation and maintenance. This approach ensures that the final system is not only efficient but also aligned with the client's long-term goals.
In conclusion, coal and coke powder conveying systems play a vital role in the efficiency and safety of industrial operations. The right system can significantly enhance productivity, reduce costs, and ensure compliance with industry standards. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner for facilities seeking reliable and effective powder conveying solutions. By combining advanced technology with customer-centric design, HeadPowder helps its clients achieve optimal performance in their coal and coke processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top