Calcined ash powder conveying is a critical process in industrial applications, particularly in power plants and waste management facilities where efficient handling of calcined ash is essential. This article provides an in-depth exploration of the working principle and key characteristics of calcined ash powder conveying systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider based in Shandong, China.
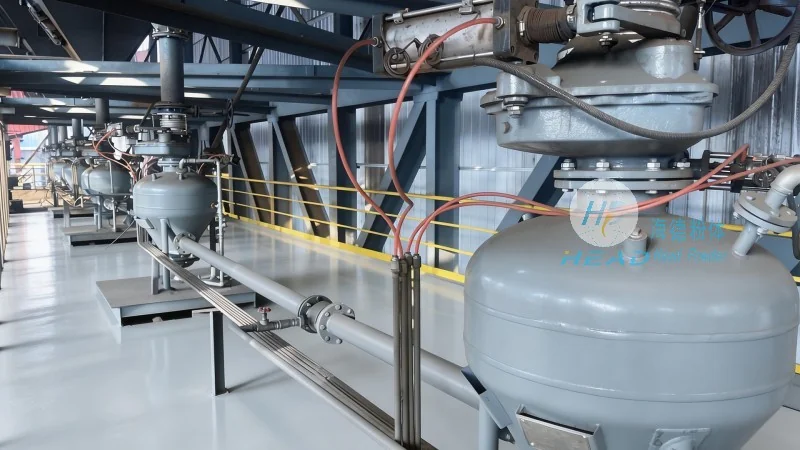
The working principle of calcined ash powder conveying is based on the fundamental physics of fluidization and pneumatic transport. In this process, calcined ash particles are introduced into a pipeline where they are entrained by a high-velocity air stream generated by a blower or compressor. The air flow creates a pressure differential that propels the ash particles through the system. The key components of a typical calcined ash powder conveying system include a hopper for material storage, a rotary valve or feeder to control the discharge rate, a conveying line (often made of stainless steel or plastic to resist corrosion), and a receiver for the discharged ash. The air flow is carefully regulated to maintain a consistent velocity, typically ranging from 15 to 30 meters per second, which is sufficient to keep the ash particles suspended without causing excessive wear on the pipeline. The system may also include a filter or cyclone to separate the ash from the air at the receiver, ensuring that the air is clean before release. This principle allows for the efficient and safe transport of calcined ash, even in environments where dust control is critical.
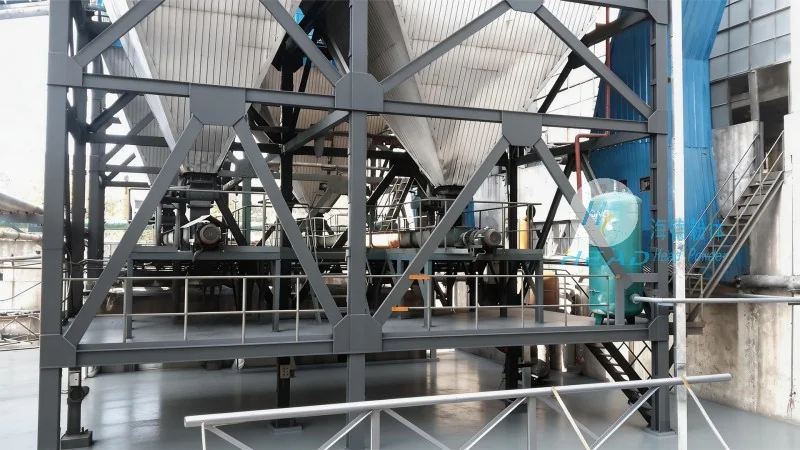
Calcined ash powder conveying systems possess several distinct characteristics that set them apart from other material handling methods. One of the most significant characteristics is their ability to handle fine, abrasive powders with minimal degradation or loss. The pneumatic design minimizes direct contact between the ash particles and the conveying equipment, reducing the risk of clogging and extending the lifespan of the system components. This is particularly important for calcined ash, which can be highly abrasive due to its composition. Another characteristic is the flexibility in layout, as the conveying lines can be arranged vertically, horizontally, or in a combination of both, allowing for adaptation to complex plant geometries. The systems are also energy-efficient, as the air flow can be optimized to achieve the required transport velocity with minimal power consumption. This efficiency is crucial for long-term operational costs and environmental sustainability. Additionally, the sealed pipeline design prevents dust emissions, which is essential for compliance with environmental regulations and maintaining a safe working environment. The systems are designed to be robust and reliable, with features such as automatic cleaning mechanisms and real-time monitoring to ensure continuous operation. This reliability is vital for industrial applications where downtime can result in significant production losses.
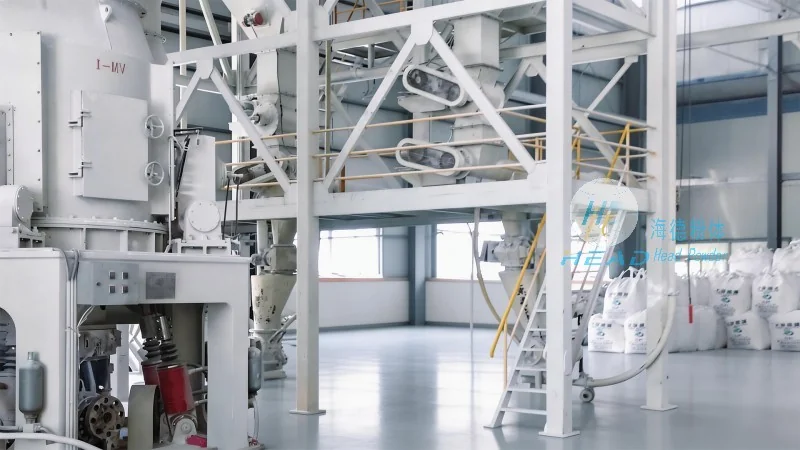
In industrial settings, calcined ash powder conveying systems demonstrate high efficiency and performance, making them a preferred choice for power plants and waste management facilities. The ability to transport large volumes of ash over long distances reduces the need for manual handling and transportation, which not only improves safety but also reduces labor costs. The systems are designed to operate continuously, with minimal downtime for maintenance, ensuring that production processes are not interrupted. The consistent flow rate and particle size distribution achieved by these systems contribute to the quality of downstream processes, such as ash utilization or disposal. For example, in power plants, the efficient conveying of calcined ash allows for its reuse in cement production or other industrial applications, reducing waste and enhancing sustainability. The scalability of the systems is another advantage, as they can be adjusted in capacity to meet changing production demands. This adaptability makes them suitable for both new and existing facilities, providing a cost-effective solution for ash management. The integration of advanced control systems, such as variable frequency drives (VFDs) and real-time monitoring sensors, further enhances the performance and reliability of the conveying process. These systems allow for precise control of the air flow and material discharge, optimizing the operation based on real-time conditions. Moreover, the use of stainless steel or corrosion-resistant materials in the pipeline construction ensures durability, even in harsh environments where calcined ash may contain acidic components. Overall, calcined ash powder conveying systems offer a comprehensive solution for efficient, safe, and environmentally friendly handling of calcined ash, aligning with the operational needs of modern industrial facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top