Wheat flour pneumatic conveying systems are critical components in modern food processing facilities, enabling the efficient and hygienic transfer of bulk wheat flour from storage silos to processing lines. These systems leverage air as the primary conveying medium, offering significant advantages over traditional mechanical conveyors. By utilizing air to lift and transport flour particles, the systems reduce the risk of contamination, enhance operational safety, and provide greater flexibility in material handling. This technology is particularly valuable in industries where maintaining product purity and minimizing downtime is paramount.
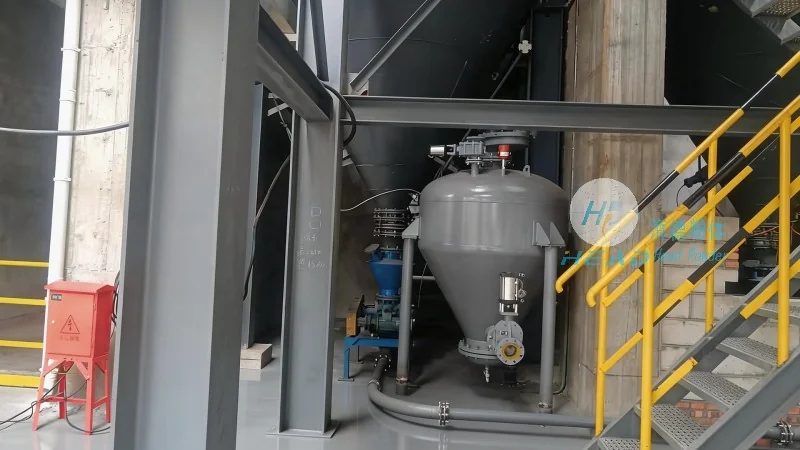
The fundamental principle behind wheat flour pneumatic conveying systems is the creation of a pressure differential that drives the movement of material. The system operates by introducing air into the conveying line, either through a positive pressure blower or a negative pressure vacuum pump. In positive pressure systems, air is forced through the line, carrying the flour particles forward. The air pressure is maintained at a level sufficient to overcome the gravitational force of the flour and any friction within the line. In negative pressure systems, a vacuum is created at the receiving end, drawing the flour into the line as it is pulled by the reduced pressure. The design of the system includes key components such as airlock valves, which control the flow of material into the conveying line, and cyclone separators, which separate the flour from the air at the receiving end. These components work in tandem to ensure efficient material transfer and product integrity.
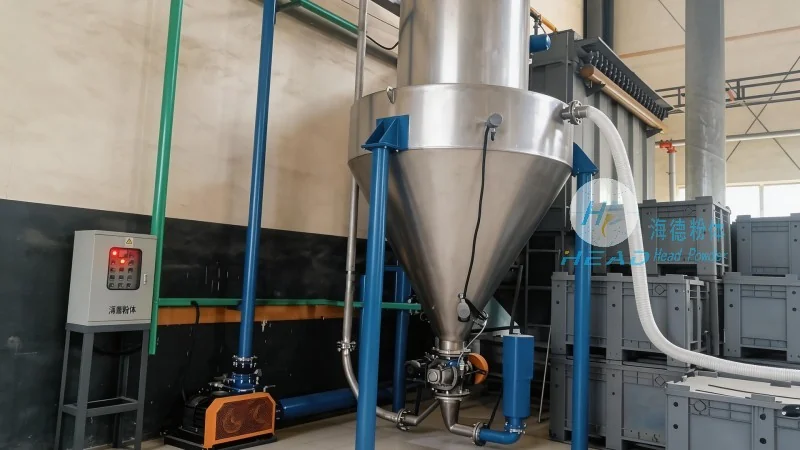
Several critical components are integral to the performance of a wheat flour pneumatic conveying system. The blower or fan is the primary source of air, providing the necessary pressure or vacuum to drive the conveying process. Airlock valves, typically located at the material hopper and receiving vessel, prevent backflow and maintain a consistent flow of material. The conveying line, often made of stainless steel or other food-grade materials, is designed to withstand the pressure and temperature of the operation while ensuring minimal material buildup. Cyclone separators are crucial for separating the flour from the air, using centrifugal force to direct the heavier flour particles to the collection chamber. Filter systems, such as bag filters or cartridge filters, further purify the air, removing any residual flour particles and ensuring compliance with hygiene standards. These components are carefully selected and integrated to optimize the system's efficiency and reliability.
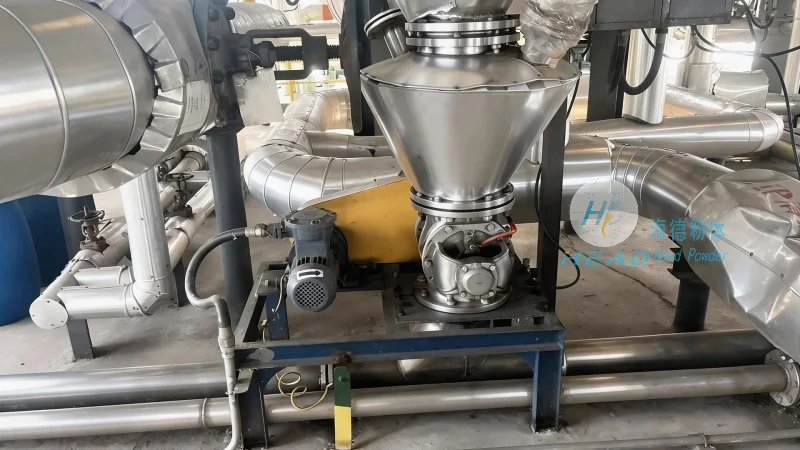
The operation of a wheat flour pneumatic conveying system follows a systematic sequence to ensure continuous and efficient material transfer. The process begins with the charging of the material hopper with wheat flour. The airlock valve at the hopper opening is then activated, allowing the flour to enter the conveying line as the airflow is initiated. The blower starts, generating the required pressure or vacuum, and the flour particles are lifted and transported through the line. The system continuously monitors the flow rate and pressure, adjusting the air volume as needed to maintain optimal conveying performance. At the receiving end, the cyclone separator separates the flour from the air, directing the flour into the receiving vessel, such as a processing silo or mixer. The air, now free of flour particles, is either vented to the atmosphere or recirculated through the system. The system may also include a cleaning cycle, where compressed air is used to clear any material buildup in the conveying line and airlock valves, ensuring that the system remains hygienic and operational. This cycle is typically automated and scheduled to prevent clogging and maintain product quality.
Wheat flour pneumatic conveying systems offer several advantages over traditional mechanical conveyors. The most significant benefit is the reduced risk of product contamination, as the flour is enclosed within the conveying line and separated from external environments. This is particularly important in food processing, where maintaining product purity is a regulatory requirement. Additionally, pneumatic systems are more hygienic and easier to clean, as they do not involve moving parts that can trap material or harbor bacteria. The systems also provide greater flexibility in material handling, allowing for vertical, horizontal, or inclined conveying, and can be easily integrated with other processing equipment. Another advantage is the ability to handle a wide range of flour types and particle sizes, from fine to coarse, without the need for additional processing steps. The systems are also relatively compact, requiring less floor space compared to mechanical conveyors, making them suitable for facilities with limited space.
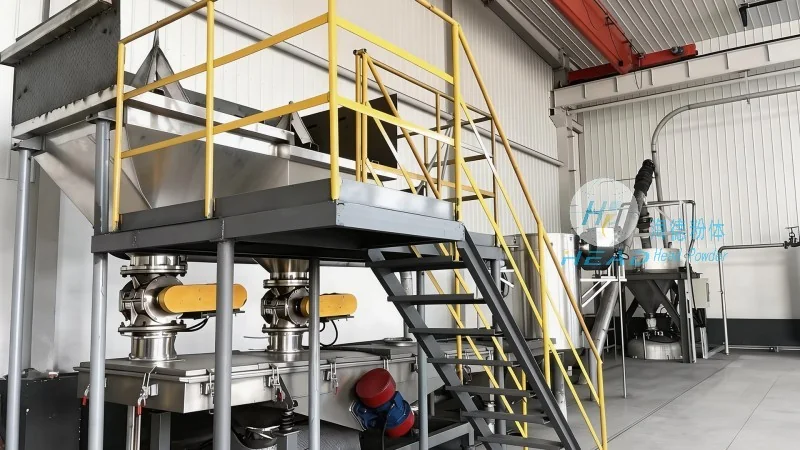
Wheat flour pneumatic conveying systems are widely used in various stages of wheat flour processing. In storage facilities, the systems transfer flour from bulk storage silos to processing lines, ensuring a continuous supply of material. During the milling process, the systems can convey raw wheat or intermediate products between grinding and sifting stages. In packaging operations, the systems move flour from processing equipment to packaging machines, maintaining a consistent flow rate and preventing product spillage. The systems are also used in quality control processes, where flour samples are taken from the conveying line for testing and analysis. The versatility of pneumatic conveying makes it suitable for both large-scale industrial operations and smaller processing facilities, providing a reliable solution for material handling in wheat flour production.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced pneumatic conveying systems for the food industry. With over [years] of experience in the field, the company specializes in designing and installing customized solutions tailored to the specific needs of wheat flour processing facilities. HeadPowder's systems are engineered with precision and adherence to industry standards, ensuring that they meet the stringent hygiene and performance requirements of food processing. The company's team of engineers and technicians works closely with clients to understand their operational challenges and provide innovative solutions that enhance efficiency and product quality. HeadPowder's commitment to quality, customer satisfaction, and technological advancement has established it as a trusted partner in the industry, helping facilities achieve optimal performance and compliance with regulatory standards.
Wheat flour pneumatic conveying systems are essential for efficient and hygienic material handling in the food processing industry. By leveraging air as the conveying medium, these systems offer significant advantages over traditional methods, including reduced contamination risk, enhanced safety, and operational flexibility. The working principle, operation process, and key components of these systems are carefully designed to ensure optimal performance and product integrity. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing advanced solutions that meet the evolving needs of the industry, helping facilities maintain high standards of quality and efficiency in wheat flour processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top