Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted provider of solutions tailored to the unique needs of various industries, including pharmaceuticals, food processing, and chemical manufacturing. This article delves into the working principle and key features of nitrogen-protected material pneumatic conveying systems, highlighting how these systems enhance operational efficiency and product integrity.
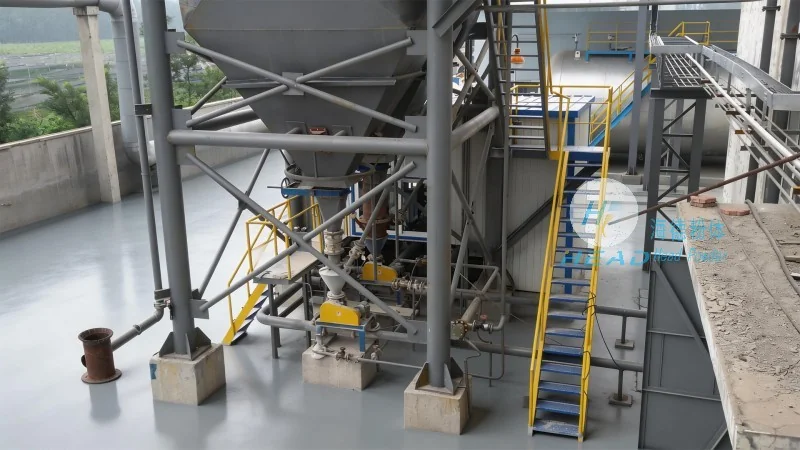
The core of a nitrogen-protected material pneumatic conveying system lies in its ability to transport bulk materials through an enclosed pipeline using a combination of air and nitrogen gas. Unlike conventional pneumatic systems that rely solely on air, this specialized approach incorporates nitrogen to create an inert atmosphere, which is crucial for applications where oxidation, moisture, or contamination must be strictly avoided. The system operates by first introducing the material into a hopper or feeder, where it is then fed into a pipeline. Compressed air or nitrogen is then introduced to create a flow of gas that propels the material through the system. The use of nitrogen ensures that the material remains in a stable, non-reactive state throughout the conveying process, preserving its quality and preventing degradation.
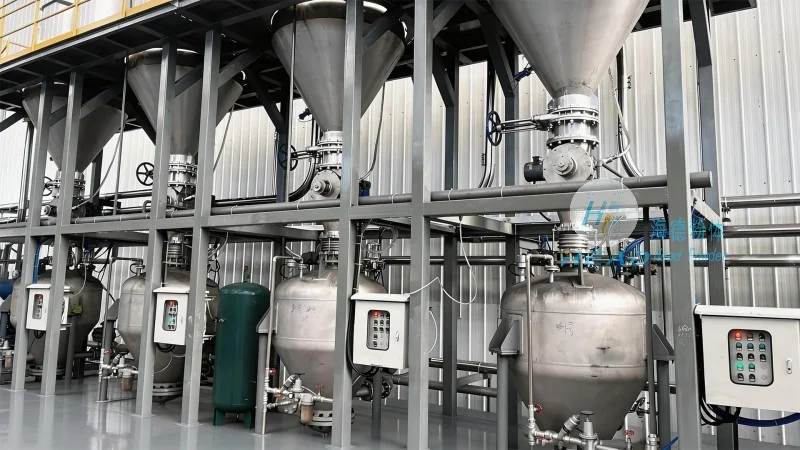
One of the primary advantages of nitrogen-protected material pneumatic conveying systems is their ability to maintain a controlled environment for sensitive materials. By using nitrogen as the carrier gas, the system eliminates the risk of oxygen exposure, which is critical for products such as pharmaceuticals, food ingredients, and certain chemicals that are prone to oxidation or spoilage. This feature not only preserves the material's quality but also extends its shelf life and ensures compliance with industry regulations. Additionally, the enclosed design of the system minimizes dust emissions and cross-contamination, contributing to a cleaner and safer working environment. The system's flexibility in handling a wide range of materials, from fine powders to bulk solids, makes it suitable for diverse applications. Furthermore, the use of nitrogen allows for precise control over the conveying velocity and pressure, ensuring efficient and reliable material transport. The system's design also incorporates features such as automatic shut-off valves and pressure relief mechanisms to enhance safety and prevent system failures.
Shandong HeadPowder Engineering Co., Ltd. offers customized nitrogen-protected material pneumatic conveying systems tailored to the specific requirements of each client. The company's engineers work closely with clients to understand their operational needs, material characteristics, and environmental constraints, ensuring that the final solution is optimized for performance and cost-effectiveness. For example, in the pharmaceutical industry, where product purity is paramount, the nitrogen-protected system provides a sterile and contamination-free environment, meeting stringent regulatory standards. In the food processing sector, the system helps maintain the freshness and nutritional value of ingredients by preventing moisture absorption and microbial growth. The system's adaptability also allows for integration with existing production lines, minimizing downtime and facilitating seamless transitions. Furthermore, the company provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure the long-term reliability of the system.
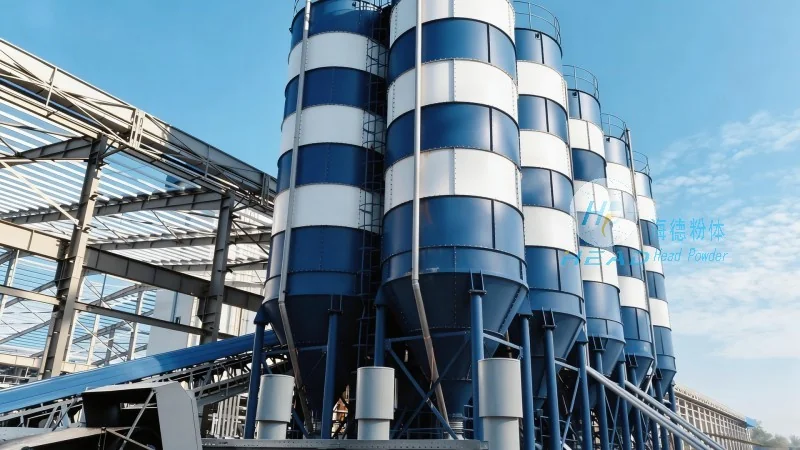
Nitrogen-protected material pneumatic conveying systems represent a sophisticated solution for industries that require the safe and efficient transport of sensitive materials. By leveraging the inert properties of nitrogen and advanced pneumatic technology, these systems offer significant advantages over traditional conveying methods. Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing high-quality, customized solutions that meet the evolving needs of modern industries. With its commitment to excellence and customer satisfaction, the company remains a leading provider of nitrogen-protected material pneumatic conveying systems, helping businesses achieve higher operational efficiency and maintain the highest standards of product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top