Calcite, a common calcium carbonate mineral, is widely utilized across industries including construction, pharmaceuticals, and chemical manufacturing. The efficient and reliable transportation of calcite powder is essential for industrial processes, and pneumatic conveying technology has become a key solution. This article explores the principles, applications, and future trends of calcite pneumatic conveying technology, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
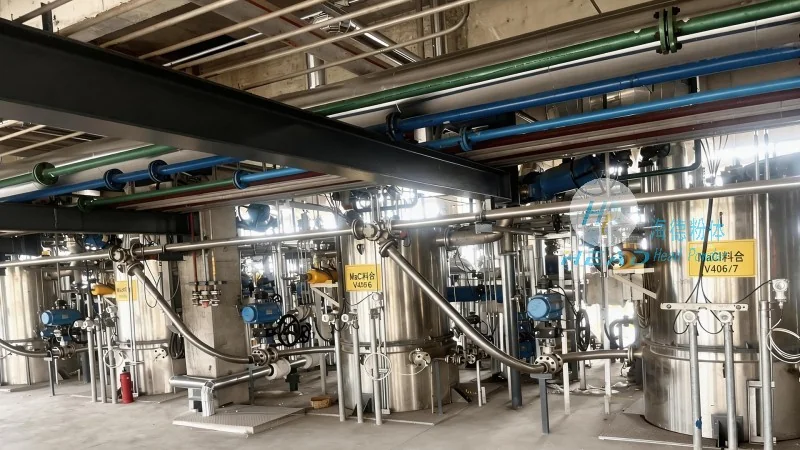
Pneumatic conveying, also known as air conveying, involves transporting bulk materials like calcite powder through pipelines using compressed air. The core principle is creating an air flow that lifts and moves material particles. Two main system types exist: dilute-phase and dense-phase. Dilute-phase systems use low air velocity to suspend material, while dense-phase systems employ higher velocity and pressure for more compact transport. For calcite, system selection depends on particle size, moisture content, and transportation distance. The HeadPowder team designs tailored systems to meet these specific requirements, ensuring optimal performance and minimal material degradation.
Calcite pneumatic conveying technology is extensively applied in industrial settings where fine powder handling is critical. In construction, calcite serves as a filler in cement and concrete, with pneumatic conveying enabling seamless transfer from storage to production lines. The pharmaceutical industry uses calcite as an excipient in drug formulations, and the technology ensures sterile, contamination-free transport. Additionally, in chemical manufacturing, calcite is used in coating and pigment production, where precise powder flow control is vital. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying solutions for these applications, improving efficiency and reducing operational costs for clients.
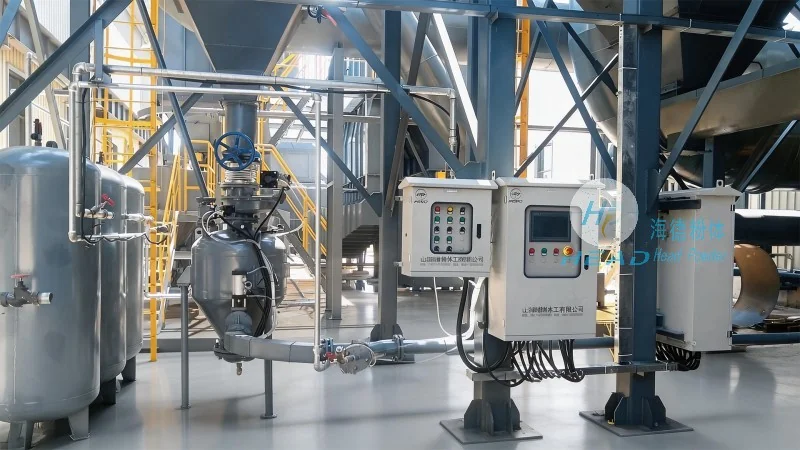
Designing an effective calcite pneumatic conveying system requires careful consideration of several factors. Particle size and density are primary determinants, as they affect the air velocity needed for suspension. Moisture content is another critical factor, as high moisture can cause agglomeration and blockages. HeadPowder engineers conduct thorough material analysis to determine optimal conveying parameters. Furthermore, pipeline layout—including diameter, bends, and silos—must be planned to minimize pressure drop and energy consumption. The company's expertise in fluid dynamics and material science allows for customized solutions that address these challenges effectively.
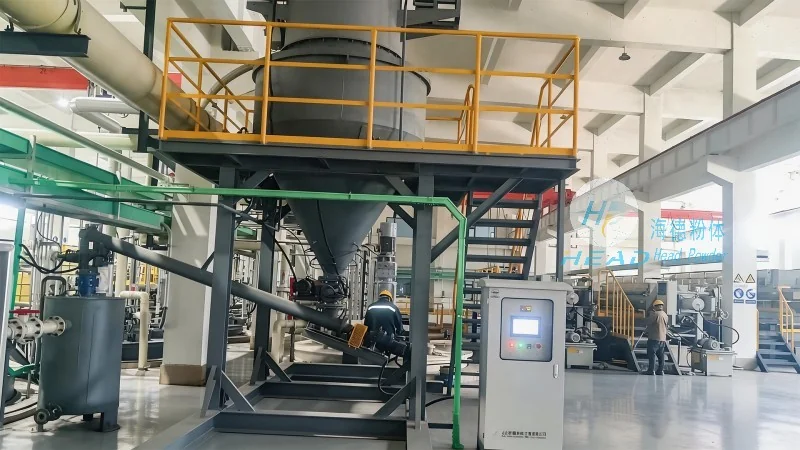
The field of calcite pneumatic conveying is continuously evolving, with advancements aimed at improving efficiency and sustainability. Modern systems incorporate advanced control technologies like variable frequency drives to optimize air usage and reduce energy consumption. Integration of sensors and monitoring systems enables real-time tracking of material flow and system performance, allowing for proactive maintenance. Additionally, there is a growing focus on sustainable practices, with companies like Shandong HeadPowder Engineering Co., Ltd. exploring renewable energy sources to power conveying systems. The future of calcite pneumatic conveying lies in developing more intelligent and energy-efficient systems that adapt to changing industrial demands.
Calcite pneumatic conveying technology plays a vital role in efficiently handling this essential mineral. Through a deep understanding of material properties and system design, companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of providing reliable and effective solutions. As industrial demands evolve, continuous innovation in pneumatic conveying systems will ensure safe and efficient calcite transport, supporting the growth of various industries. The expertise and experience of HeadPowder make them a trusted partner for businesses seeking to optimize their calcite handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top