Shandong HeadPowder Engineering Co., Ltd. specializes in advanced mineral particle pneumatic conveying solutions, offering a comprehensive understanding of the technology's principles, practical applications, and future trends. Pneumatic conveying is a critical process in material handling, enabling the efficient transport of bulk materials like minerals, powders, and granules through a pressurized or vacuum system. This technology has revolutionized industries such as mining, chemical processing, and food production by providing a flexible, cost-effective, and safe method for material transport.
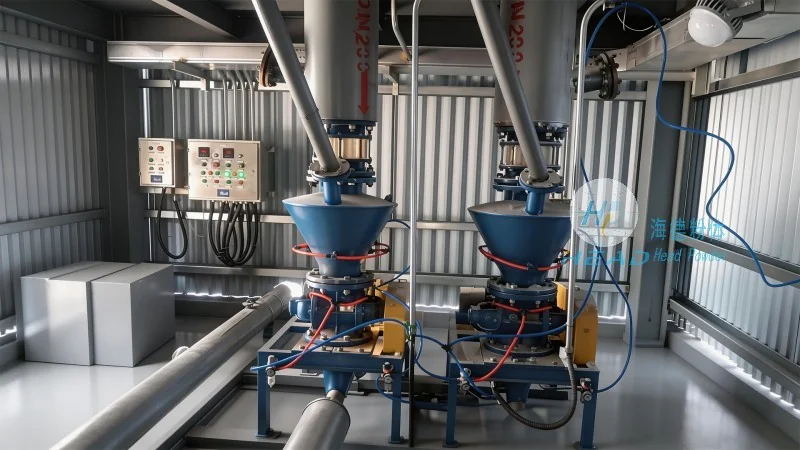
The core principle of pneumatic conveying involves using air or gas to move solid particles through a pipeline. There are two primary types of systems: pressure and vacuum. In pressure systems, compressed air is used to push material from a hopper or silo into the conveying line, while vacuum systems use a fan or blower to draw material from a source into the pipeline. The design of the system, including the type of air flow (e.g., dilute-phase or dense-phase), the material's properties (e.g., particle size, density, and moisture content), and the system's layout, all influence the efficiency and effectiveness of the conveying process. Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering to optimize these parameters, ensuring reliable and consistent performance for various mineral particle applications.
Pneumatic conveying technology is widely applied in the mineral processing industry for tasks such as ore transport from mines to processing plants, material transfer between different processing stages (e.g., crushing, grinding, and classification), and the delivery of finished products to storage or packaging facilities. The technology is particularly advantageous for handling fine powders and granules, which are often difficult to transport using traditional methods like belt conveyors or bucket elevators. For example, in the mining sector, pneumatic systems can efficiently convey crushed ore from a crusher to a grinding mill, reducing downtime and improving overall plant throughput. In chemical processing, the technology is used to transport raw materials and intermediates, ensuring a continuous and controlled flow of materials. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying solutions for various mineral applications, including coal, limestone, and metal ores, demonstrating the technology's versatility and reliability.
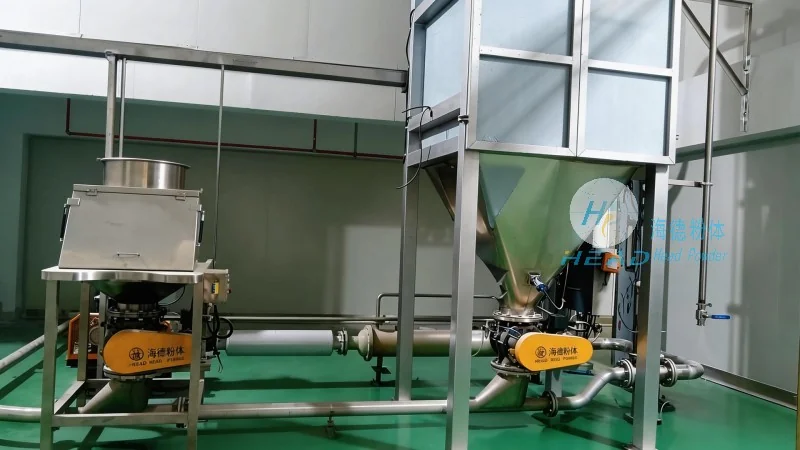
Compared to traditional material handling methods, pneumatic conveying offers several key advantages for mineral processing operations. First, it provides a dust-free and enclosed transport system, which enhances workplace safety and reduces environmental contamination. This is particularly important for handling mineral powders that may be hazardous or cause respiratory issues. Second, pneumatic systems are flexible and can be easily reconfigured to accommodate changes in production processes or material types. The ability to adjust the air flow rate and pressure allows for precise control over the conveying speed and material flow, minimizing material degradation and loss. Third, the technology is energy-efficient, as it uses less power compared to mechanical conveyors, especially for long-distance or high-volume transport. Shandong HeadPowder Engineering Co., Ltd. emphasizes these benefits in its solutions, ensuring that clients achieve optimal performance while maintaining cost-effectiveness and operational safety.
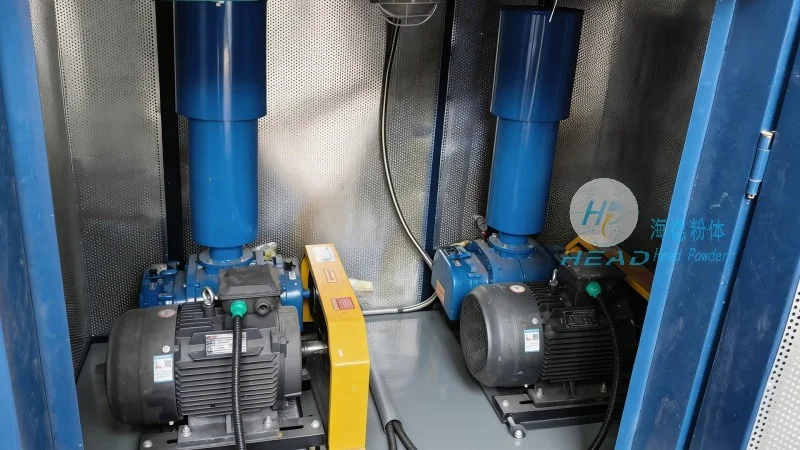
The field of pneumatic conveying continues to evolve, with ongoing research and development focused on improving system efficiency, reducing maintenance costs, and enhancing material handling capabilities. Recent advancements include the integration of automation and control systems, which allow for real-time monitoring and adjustment of conveying parameters. This automation helps optimize energy usage and prevent system failures, leading to increased operational reliability. Additionally, the development of new materials and components, such as high-strength pipelines and advanced air filtration systems, has extended the lifespan of pneumatic conveying equipment and improved its performance under harsh conditions. Shandong HeadPowder Engineering Co., Ltd. stays at the forefront of these technological developments, incorporating the latest innovations into its solutions to meet the evolving needs of the mineral processing industry. The future of pneumatic conveying technology is likely to involve more sustainable and eco-friendly designs, with a focus on reducing energy consumption and minimizing environmental impact.
Mineral particle pneumatic conveying technology remains a vital component of modern material handling, offering efficient, safe, and flexible solutions for the mineral processing industry. Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in engineering and design to provide tailored pneumatic conveying systems that meet the specific requirements of its clients. By understanding the principles, applications, and trends of this technology, companies can enhance their operational efficiency, reduce costs, and improve overall productivity. With a commitment to innovation and quality, Shandong HeadPowder Engineering Co., Ltd. continues to be a leader in providing advanced pneumatic conveying solutions for the global mineral processing market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top