Urea, a crucial nitrogen fertilizer, is widely used in agricultural and industrial applications. Efficient and reliable transportation of urea is essential for maintaining supply chain integrity and operational efficiency. This article provides a comprehensive overview of urea pneumatic conveying systems, focusing on their design, functionality, and practical applications. Developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), these systems are engineered to meet the stringent demands of the fertilizer industry, ensuring optimal performance and durability.
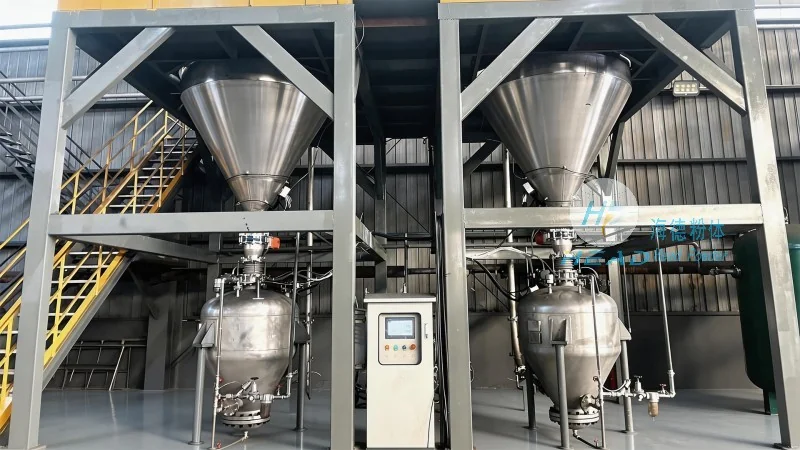
Urea pneumatic conveying systems typically consist of several core components that work in tandem to transport urea powder. The primary components include a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with a blower or compressor to generate air pressure), and a receiver or discharge unit. Each component plays a critical role in ensuring smooth and consistent urea transport. The hopper is designed to hold a large quantity of urea, preventing material bridging and ensuring a steady feed. The feeder, such as a rotary valve or screw feeder, regulates the amount of urea released into the conveying line, maintaining optimal flow rates. The blower or compressor generates the necessary air pressure to move the urea particles through the pipeline. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of urea and prevent material buildup. The receiver or discharge unit collects the urea at the destination, allowing for safe and controlled unloading.
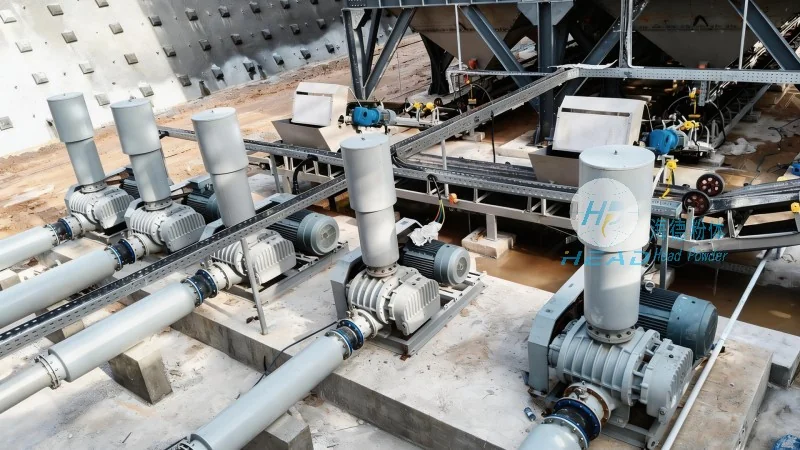
There are two main types of urea pneumatic conveying systems: pressure and vacuum systems. Pressure systems use a blower or compressor to create positive pressure in the conveying line, pushing the urea particles forward. These systems are suitable for short to medium distances and can handle higher flow rates. Vacuum systems, on the other hand, use a vacuum pump to create negative pressure, drawing the urea particles into the line. Vacuum systems are ideal for longer distances and can handle more complex layouts, including vertical lifts and multiple branches. The choice between pressure and vacuum systems depends on factors such as the distance to be covered, the required flow rate, and the layout of the facility. For instance, a pressure system might be preferred for a short-distance transfer from a storage silo to a processing plant, while a vacuum system could be used for a longer-distance transport from a warehouse to a distribution center.
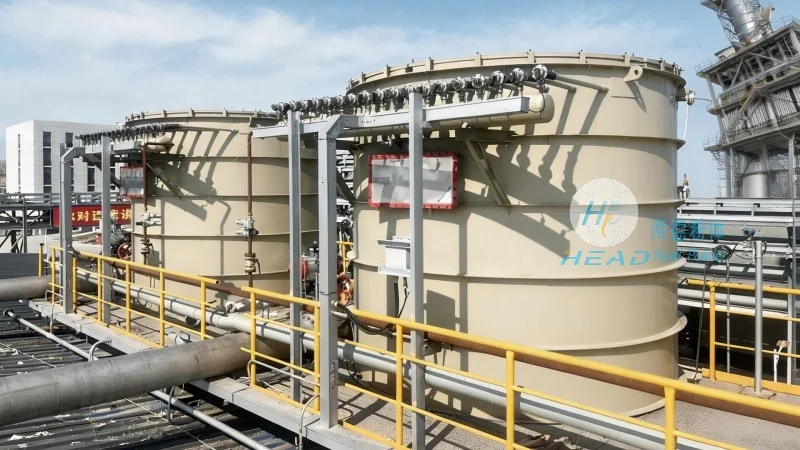
Urea pneumatic conveying systems offer several advantages over traditional bulk material handling methods. One of the key benefits is the ability to transport urea in a dust-free environment, reducing the risk of inhalation and improving workplace safety. This is particularly important in agricultural settings where workers are exposed to urea dust. Additionally, pneumatic conveying systems can handle urea with a high moisture content, preventing clumping and ensuring consistent flow. The systems are also highly flexible, allowing for easy integration with existing infrastructure and the ability to add or modify conveying lines as needed. Another advantage is the reduced need for manual handling, which minimizes the risk of accidents and improves operational efficiency. Overall, urea pneumatic conveying systems provide a reliable, efficient, and safe method for transporting urea, making them a preferred choice for many industries.
Urea pneumatic conveying systems are widely used in various industries, including agriculture, chemical manufacturing, and food processing. In agriculture, these systems are commonly used to transport urea from storage silos to application equipment, such as spreaders or sprayers. This allows for precise and uniform application of nitrogen fertilizer, improving crop yields and reducing waste. In chemical manufacturing, urea is used as a raw material for producing other products, such as adhesives, plastics, and pharmaceuticals. Pneumatic conveying systems are used to transport urea from storage to processing units, ensuring a continuous supply of raw material. In food processing, urea is used as a preservative or flavor enhancer in some products. The systems help maintain the quality and consistency of the urea during transport, ensuring that the final product meets safety and quality standards. Regardless of the industry, urea pneumatic conveying systems play a critical role in ensuring the efficient and safe handling of urea.
The successful operation of a urea pneumatic conveying system depends on proper installation and regular maintenance. During installation, it is essential to ensure that all components are properly aligned and connected, with no leaks in the conveying line. The hopper and feeder should be positioned to allow for smooth material flow, and the blower or compressor should be sized appropriately for the required flow rate and distance. Regular maintenance is crucial to prevent system downtime and ensure long-term performance. This includes checking for wear and tear on components, such as the feeder and conveying line, and replacing parts as needed. The air filter and compressor should also be cleaned or replaced regularly to maintain optimal performance. Additionally, the system should be inspected for any signs of corrosion or damage, especially in areas where urea may come into contact with metal surfaces. Proper maintenance can extend the life of the system and reduce the risk of breakdowns, ensuring consistent and reliable urea transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top