Phosphate fertilizer is a critical component in modern agriculture, providing essential nutrients for plant growth. The efficient handling and transportation of phosphate powders are vital for maintaining production efficiency and ensuring product quality. This article explores the operation process and working principle of a phosphate powder pneumatic conveying system, highlighting its key components, operational procedures, and the technical advantages it offers to industries involved in fertilizer production and distribution.
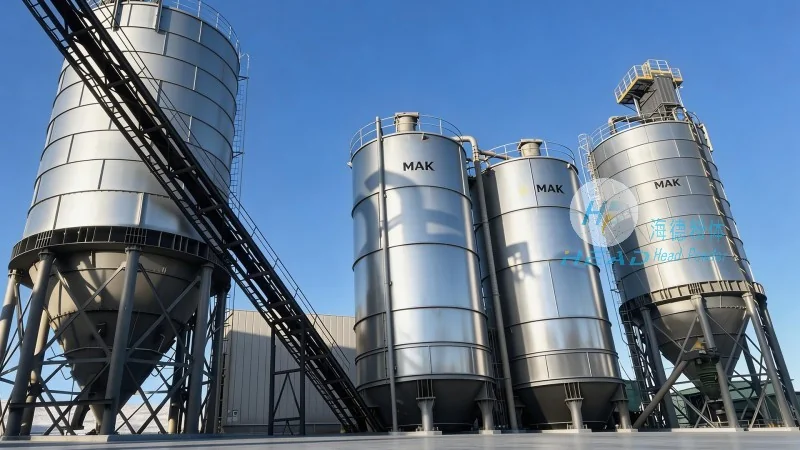
The phosphate powder pneumatic conveying system consists of several essential components that work in tandem to achieve effective material transport. These include the hopper for material storage, a rotary valve for controlled discharge, a conveyor pipeline system, a blower or air compressor to generate the conveying air, a filter system to remove dust and particles from the air, and a discharge unit for delivering the material to the destination. Each component plays a crucial role in the overall system performance, ensuring smooth and reliable operation.
The operation of the phosphate powder pneumatic conveying system is based on the principle of air suspension, where the phosphate powder is suspended in a stream of air and transported through the pipeline. The process begins with the material being fed into the hopper from a storage silo or bagging area. The rotary valve then regulates the flow of powder into the conveyor pipeline, ensuring a consistent feed rate. The blower or air compressor generates high-pressure air, which is introduced into the pipeline, creating a flow that lifts and transports the phosphate powder particles. As the powder travels through the pipeline, it is kept in suspension by the air flow, preventing clogging and ensuring uniform transport. The filter system captures any fine particles or dust from the air, maintaining air quality and preventing contamination. Finally, the material is discharged at the receiving end, where it is collected in a storage bin or directly fed into processing equipment.
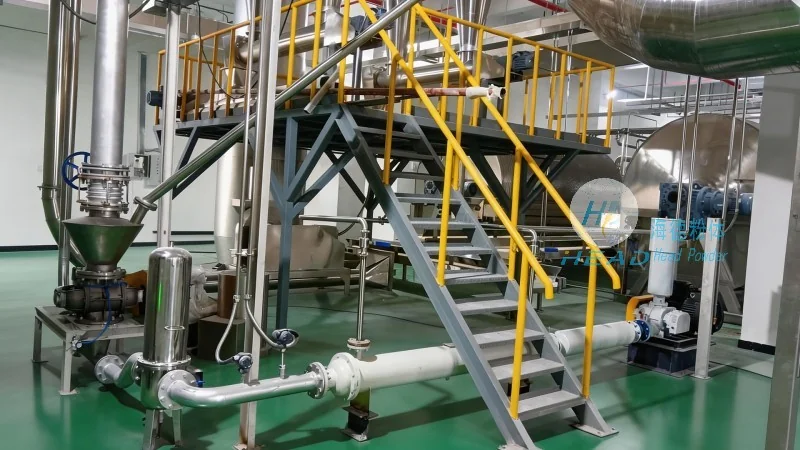
The operation of the phosphate powder pneumatic conveying system follows a systematic process to ensure optimal performance and material handling. The steps include: 1. Material Loading: The phosphate powder is loaded into the hopper from the storage area, with the rotary valve controlling the initial feed rate. 2. Air Supply Activation: The blower or air compressor is started, generating the necessary air pressure to initiate the conveying process. 3. Conveying Start: The rotary valve opens, allowing the powder to enter the pipeline as the air flow begins to transport it. 4. Continuous Transport: The system maintains a steady air flow and powder feed rate, ensuring consistent material movement through the pipeline. 5. Filter Maintenance: The filter system continuously removes dust and particles, maintaining air quality and preventing system blockages. 6. Discharge and Collection: The material is discharged at the receiving end, where it is collected for further processing or storage. Each step is carefully controlled to optimize efficiency and minimize downtime, ensuring the system operates reliably and efficiently.
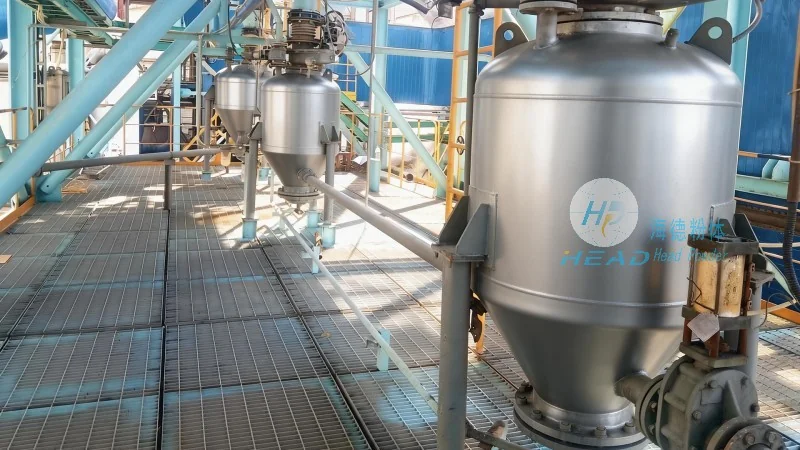
The phosphate powder pneumatic conveying system offers several technical advantages that make it an ideal solution for handling phosphate fertilizers. These include high transport efficiency, as the system can move large quantities of material over long distances with minimal energy consumption. The system also provides excellent material containment, reducing dust emissions and improving workplace safety. Additionally, the flexible pipeline design allows for easy integration into existing production lines and facility layouts. The system is widely used in the fertilizer industry for transporting phosphate powders from storage to processing units, from processing to packaging, and for interplant material transfer, making it a versatile and essential component in modern agricultural production.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. With a focus on innovation and quality, the company specializes in designing and manufacturing customized solutions for the fertilizer and chemical industries. Headpowder's expertise in material handling technology ensures that their systems are reliable, efficient, and tailored to meet the specific needs of their clients. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, providing high-quality equipment and comprehensive support to ensure optimal performance and long-term operation of their systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top