Pneumatic conveying systems have become indispensable in modern industrial operations, particularly for handling bulk materials like magnesium oxide. The efficient and reliable transport of such materials is crucial for maintaining production efficiency and ensuring product quality. This article delves into the operation process and working principle of a specialized magnesium oxide pneumatic conveying system, highlighting its design, functionality, and practical application.
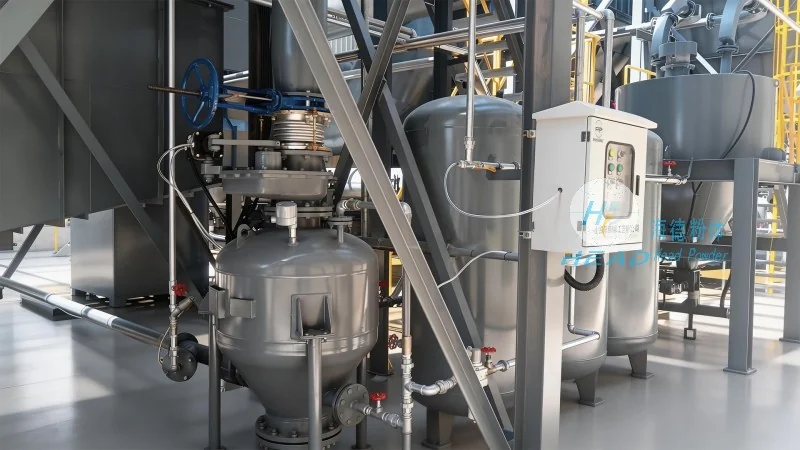
The magnesium oxide pneumatic conveying system typically consists of several core components that work in tandem to achieve effective material transport. These include a material hopper or feeder, a rotary airlock valve, a high-pressure air compressor, a conveying pipeline, and a dust collection system. Each component plays a vital role in the overall operation, ensuring that magnesium oxide is moved safely and efficiently from the source to the destination.
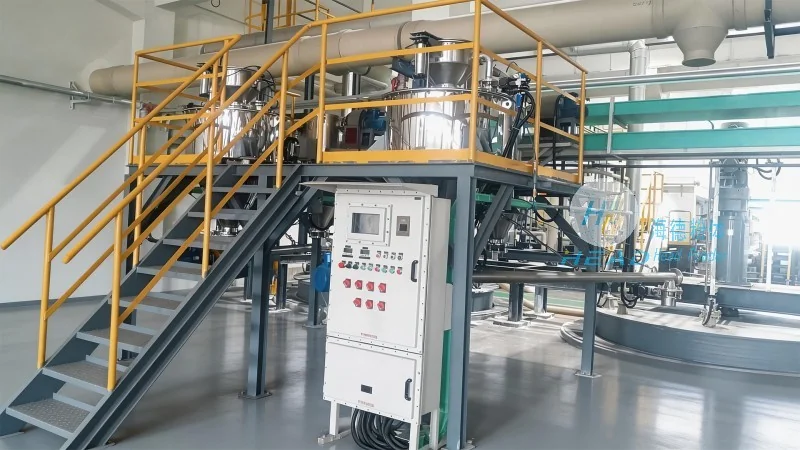
The working principle of the pneumatic conveying system relies on the use of compressed air to create a flow that propels the magnesium oxide particles through the pipeline. When the system is activated, the air compressor generates high-pressure air, which is then directed into the conveying line. The rotary airlock valve controls the flow of magnesium oxide from the hopper into the pipeline, ensuring a consistent and controlled feed. As the air flows through the pipeline, it creates a low-pressure zone that draws the magnesium oxide particles along with it, forming a slurry-like mixture. This mixture travels through the pipeline to the destination point, where it is separated from the air using a cyclone or other separation equipment.
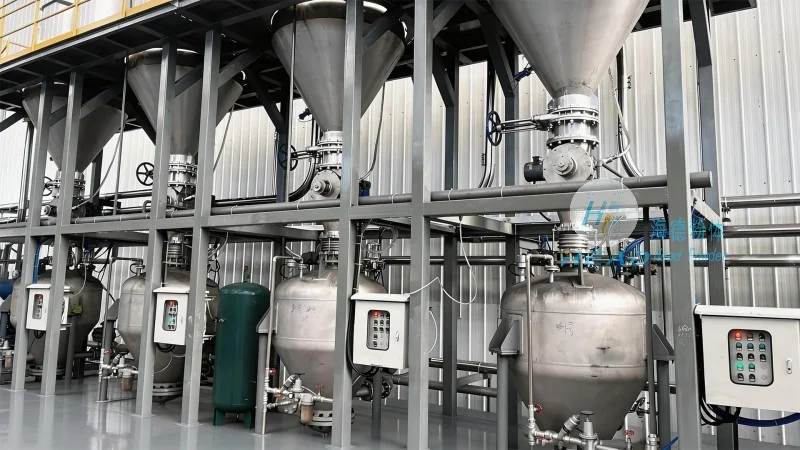
The operation process of the magnesium oxide pneumatic conveying system involves several sequential steps. First, the magnesium oxide is loaded into the material hopper. The rotary airlock valve then opens to allow the material to enter the conveying pipeline as the air compressor starts operating. The high-pressure air is introduced into the pipeline, creating the necessary pressure differential to move the material. The material is then conveyed through the pipeline to the receiving hopper or storage area. At the destination, the air and material are separated, with the magnesium oxide collected and the air either released or recirculated. This process is typically automated, with sensors and controls monitoring the flow rate, pressure, and other parameters to maintain optimal performance.
The pneumatic conveying system offers several advantages for handling magnesium oxide. Firstly, it eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination. Secondly, it provides a dust-free and enclosed transport environment, which is essential for maintaining product purity and ensuring workplace safety. Thirdly, the system can handle varying material flow rates and can be easily scaled to accommodate different production volumes. Additionally, the enclosed design helps in controlling dust emissions, complying with environmental regulations and improving overall operational efficiency.
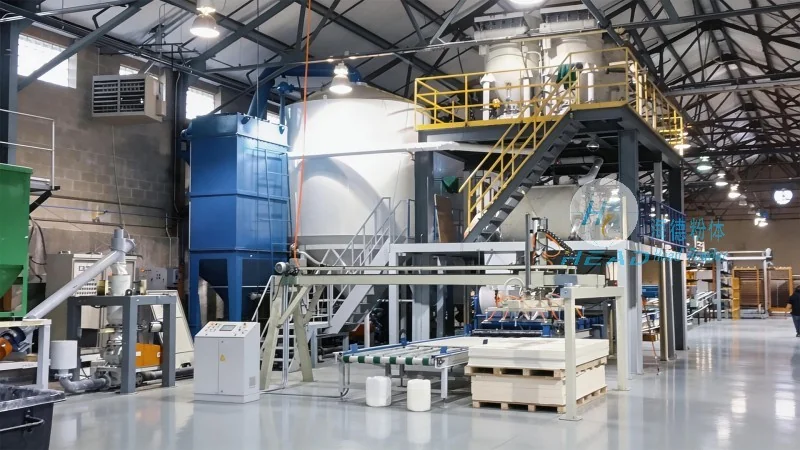
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, reliable solutions tailored to the specific needs of clients. The company's expertise lies in understanding the unique challenges of handling materials like magnesium oxide and providing customized systems that ensure optimal performance and longevity. HeadPowder's commitment to quality and customer satisfaction makes it a trusted partner for businesses seeking efficient and effective material transport solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top