Urea powder conveying systems are essential industrial equipment used in the handling and transportation of urea, a critical fertilizer and chemical raw material. These systems are designed to efficiently move urea powder from storage to processing or distribution points, ensuring safe and reliable operation in various industrial settings. The design of such systems involves careful consideration of material properties, operational requirements, and safety standards to meet the demands of modern industrial processes.
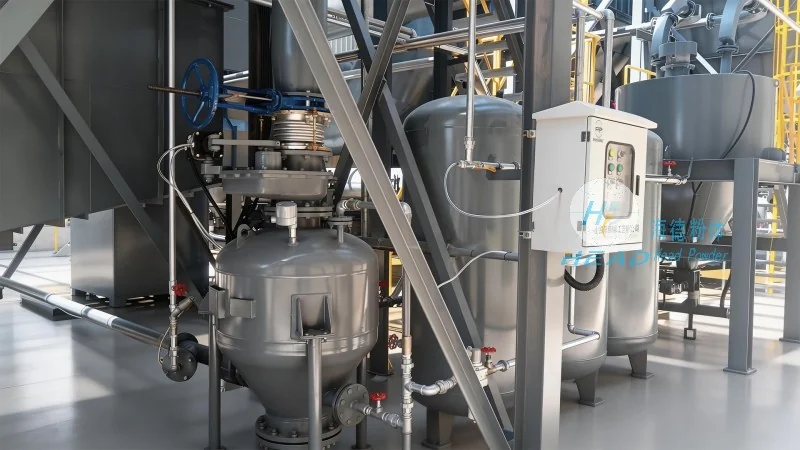
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and supply of advanced powder handling solutions. With a strong focus on innovation and quality, HeadPowder provides comprehensive urea powder conveying systems tailored to meet the specific needs of clients in the agricultural and chemical industries. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-performance equipment.
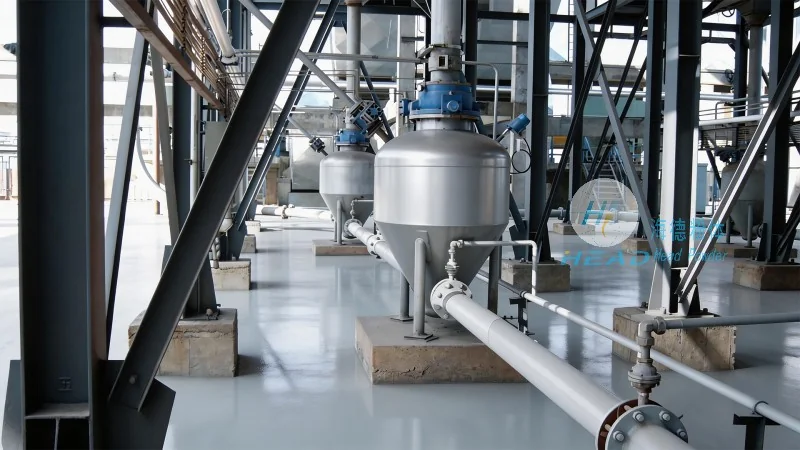
The design of a urea powder conveying system is based on several fundamental principles that ensure optimal performance and safety. Key considerations include the physical properties of urea powder, such as its flowability, moisture content, and potential for caking, which directly impact the system’s design. Engineers must also account for the system’s intended application, whether it is for bulk storage, intermediate handling, or final distribution. The design typically incorporates components like hoppers, feeders, conveyors, and control systems to facilitate the seamless movement of urea powder.
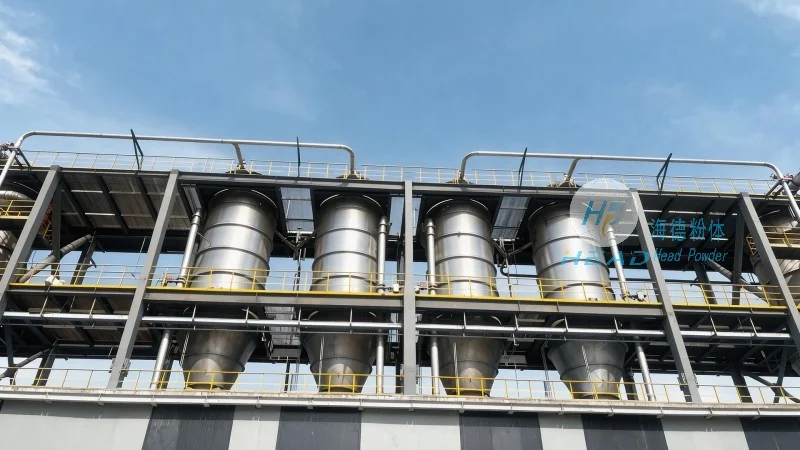
Urea powder conveying systems consist of several critical components, each playing a vital role in the overall operation. The hopper serves as the primary storage and feeding unit, designed to hold a large volume of urea powder while maintaining consistent flow. The feeder, often a rotary or vibratory type, regulates the discharge rate of the powder from the hopper, ensuring a controlled and steady supply to the conveyor. The conveyor itself, which may be a pneumatic or mechanical system, transports the urea powder through the system. Pneumatic conveying systems use air pressure to move the powder, while mechanical conveyors rely on belts or screws. Additionally, control systems and safety features, such as pressure relief valves and dust collection equipment, are integrated to ensure safe and efficient operation.
Urea powder conveying systems offer several advantages that make them indispensable in industrial applications. These systems enhance operational efficiency by reducing labor costs and minimizing material loss during handling. They also improve safety by minimizing direct human contact with the powder, which can be dusty and potentially hazardous. Furthermore, the design of these systems allows for flexibility in layout, enabling integration into existing industrial facilities without significant modifications. The reliability of modern urea powder conveying systems ensures consistent performance, even under varying load conditions, contributing to overall process stability.
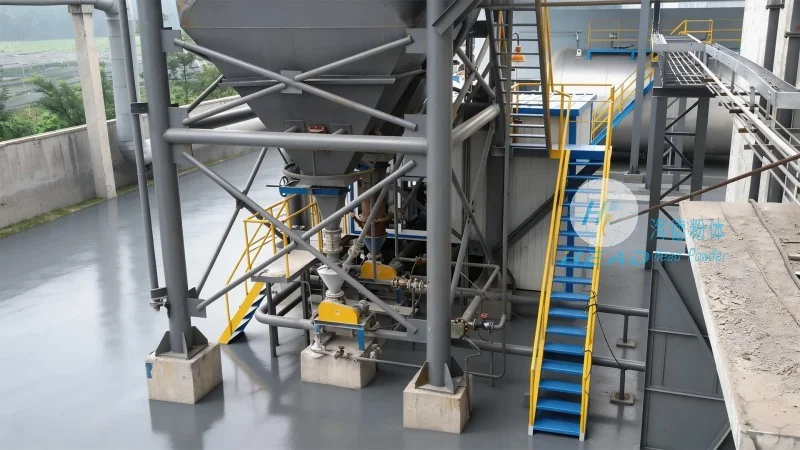
Urea powder conveying systems are widely used in the agricultural sector, where they facilitate the distribution of urea as a fertilizer. In chemical plants, these systems are crucial for transporting urea as a raw material for further processing. The systems are also employed in industrial facilities involved in the production of other nitrogen-based compounds. By ensuring efficient and safe handling of urea powder, these systems contribute to the overall productivity and sustainability of industrial operations. The technology behind urea powder conveying systems continues to evolve, with advancements in materials and control systems improving performance and reducing environmental impact.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top