White powder bulk material handling systems are critical infrastructure in industries that rely on the consistent and safe transport of fine powders. These systems are designed to address the unique challenges posed by white powders, such as their fine particle size, tendency to generate static electricity, and the need for contamination-free processing. In sectors like pharmaceuticals, food processing, and chemical manufacturing, the efficient handling of white powders is essential for maintaining product quality, ensuring regulatory compliance, and optimizing production efficiency. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in designing and supplying advanced white powder bulk material handling systems tailored to meet the specific needs of various industries.
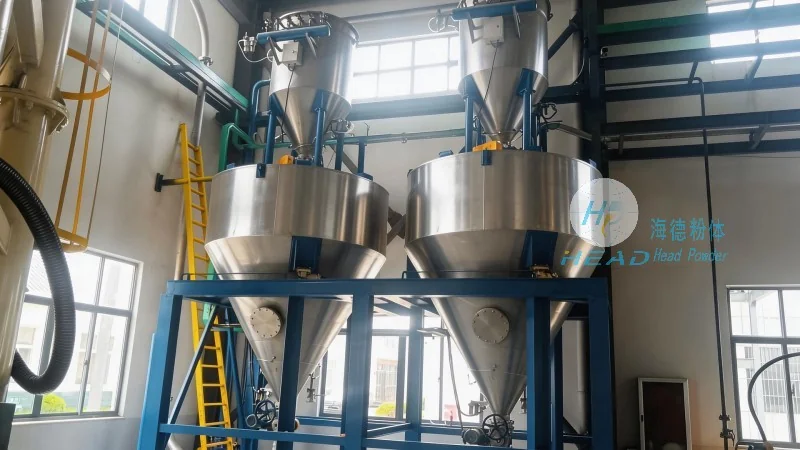
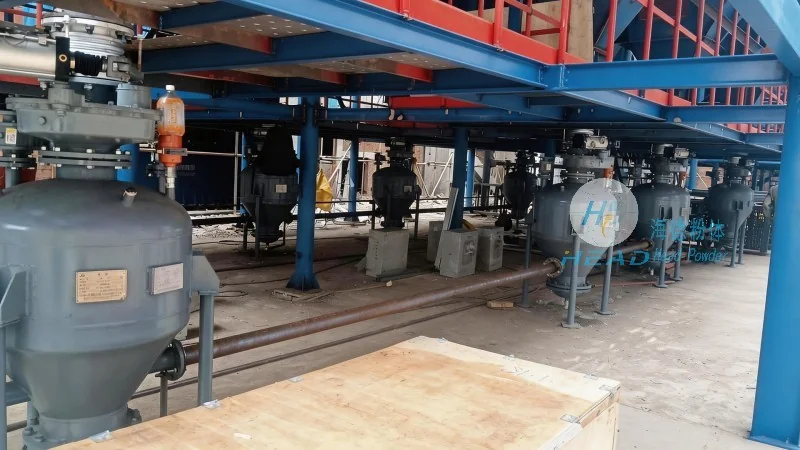
The functionality of a white powder bulk material handling system is built upon several key components, each serving a specific purpose in the material flow process. The primary component is the hopper, which serves as the storage vessel for the white powder. Hoppers are typically designed with smooth, non-porous surfaces and may include anti-static coatings to prevent powder accumulation and static discharge, which can lead to dust explosions. The feeder, often a rotary valve or a screw feeder, is responsible for controlling the flow rate of the powder from the hopper to the subsequent transportation stage. This component ensures a consistent and controlled discharge of the powder, preventing overloading or underflow. The conveyor or pneumatic system then transports the powder to the processing or packaging area. For pneumatic systems, compressed air is used to move the powder through a network of pipes, while mechanical conveyors use belts or chains to transport the material. Finally, the control panel integrates all components, allowing operators to monitor and adjust parameters such as flow rate, pressure, and temperature. This centralized control enhances operational flexibility and ensures precise management of the material handling process.
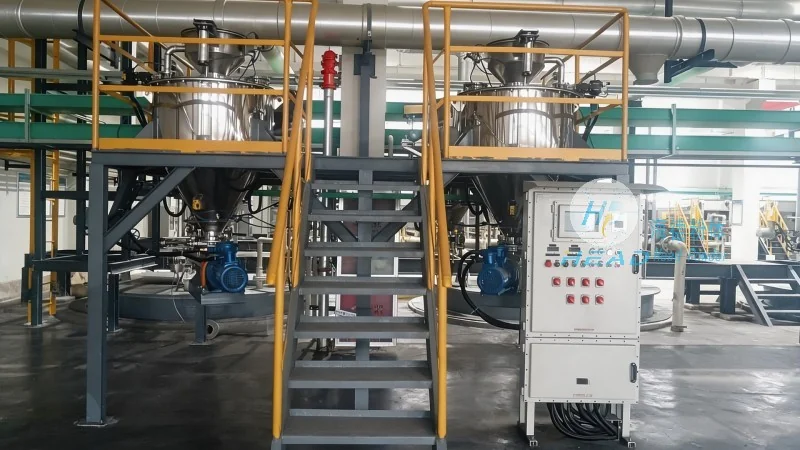
The design of a white powder bulk material handling system is guided by several critical principles that address the inherent properties of white powders and the operational requirements of the industry. The first principle is explosion prevention, which is achieved through the use of explosion-proof components, proper ventilation systems, and grounding to dissipate static electricity. This is particularly important in industries where the powders may be combustible or reactive. The second principle is material compatibility, as the system must be constructed from materials that are resistant to corrosion, wear, and chemical degradation. For example, stainless steel or special alloys may be used for components that come into direct contact with the powder, ensuring durability and preventing contamination. The third principle is ease of cleaning and maintenance, which is crucial in industries like pharmaceuticals and food processing where cross-contamination must be avoided. The system is designed with smooth surfaces and accessible components that can be easily disassembled and cleaned. The fourth principle is energy efficiency, as the system is engineered to minimize power consumption while maintaining performance. This includes optimizing the flow rate, using efficient motors, and reducing air leakage in pneumatic systems. By adhering to these design principles, the system ensures safe, reliable, and cost-effective operation.
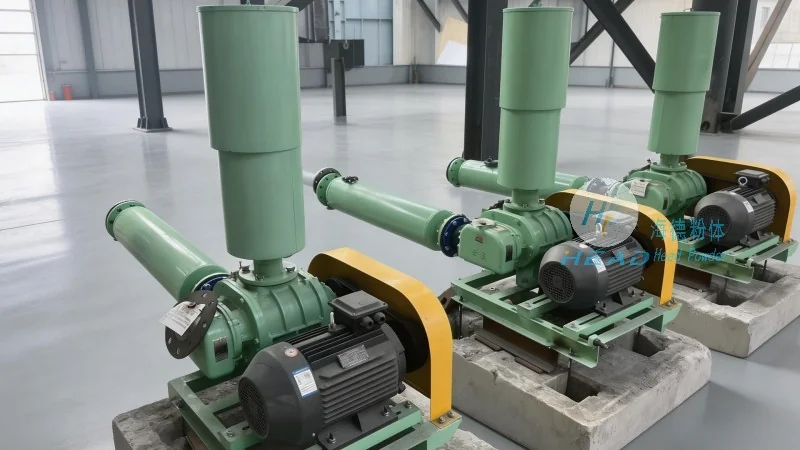
White powder bulk material handling systems find extensive applications across various industries due to their adaptability and effectiveness. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the powders are transported in a sterile and controlled environment. This is critical for maintaining the purity and efficacy of the final drug products. In the food processing industry, they are used to transport ingredients like flour, sugar, and spices, maintaining product quality and preventing contamination. The systems are often designed with sanitary features to meet food safety regulations. In the chemical industry, they are used to transport chemical powders, which may be hazardous or reactive, requiring specialized handling to ensure safety. The ability to customize the system for specific applications makes it suitable for a wide range of processes, from small-scale laboratory operations to large-scale industrial production.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top