For industrial facilities dealing with the handling and transportation of dry ash powders, understanding the technology behind efficient dry ash powder conveying systems is crucial. These systems are engineered to safely and effectively transport fine particulate materials like fly ash, bottom ash, and other industrial powders over long distances or within complex processing plants. The design principles of such systems are rooted in optimizing material flow, minimizing dust emissions, and ensuring operational reliability under various environmental and operational conditions.
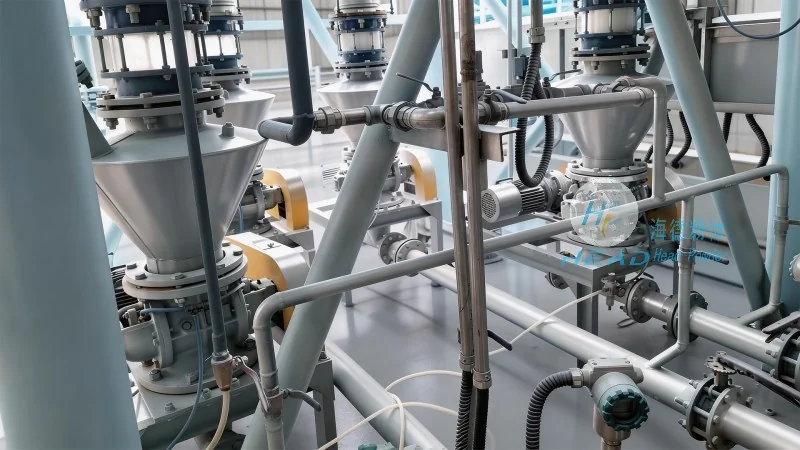
A dry ash powder conveying system is a specialized piece of industrial equipment designed to transport dry, fine particulate materials, typically from power plants or other industrial processes, from one location to another. These systems are essential for managing ash byproducts, which are often generated in large quantities and require proper disposal or reutilization. The core components of a typical dry ash powder conveying system include a hopper for material storage, a conveyor mechanism (such as pneumatic or mechanical), and control systems to regulate flow and pressure. The system’s design must account for the physical properties of the ash, including its particle size, moisture content, and density, to ensure efficient and safe operation.
The design of a dry ash powder conveying system is guided by several critical principles aimed at maximizing performance and minimizing operational issues. First, the system must ensure a consistent and uniform material feed to prevent blockages or uneven flow. This is often achieved through the use of feeders, such as rotary valves or screw conveyors, which control the rate at which ash is introduced into the conveying line. Second, the choice of conveyor type—whether pneumatic (air-assisted) or mechanical (e.g., belt or screw conveyors)—is determined by the material’s characteristics and the distance to be covered. Pneumatic systems are particularly effective for long-distance transport due to their ability to handle high volumes and navigate complex layouts, while mechanical systems may be preferred for shorter distances or where space constraints are a factor.
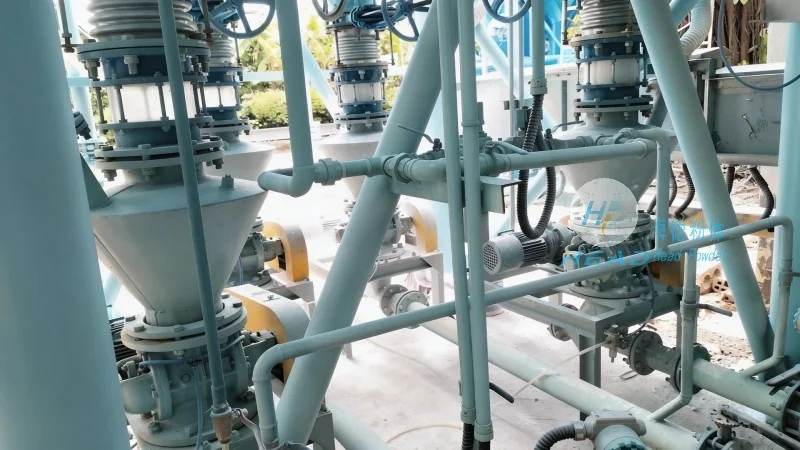
Third, the system’s design incorporates measures to control dust generation and emissions. This is critical for maintaining air quality and complying with environmental regulations. Common solutions include dust collection systems, sealed conveyor components, and the use of low-pressure air in pneumatic systems to minimize particle dispersion. Additionally, the system must be constructed from materials that are resistant to corrosion and abrasion, as ash particles can be highly abrasive and corrosive over time. The use of high-quality stainless steel or specialized coatings on conveyor components helps extend the system’s lifespan and reduce maintenance costs.
At the heart of a dry ash powder conveying system are several key components that work in tandem to ensure smooth operation. The hopper, typically made of heavy-duty steel, serves as the primary storage vessel for the ash, providing a buffer to regulate the flow rate. The feeder, often a rotary valve or a variable-speed screw, controls the discharge of material from the hopper into the conveyor line. For pneumatic systems, the blower or compressor generates the necessary air pressure to move the ash particles through the pipeline. The pipeline itself is usually made of flexible or rigid materials, such as PVC or steel, depending on the system’s requirements. The system may also include check valves, filters, and pressure regulators to maintain consistent airflow and prevent backflow.
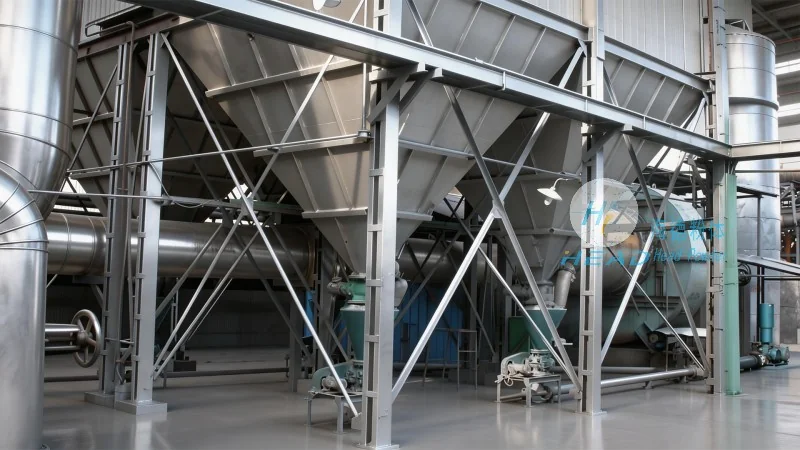
Dry ash powder conveying systems are widely used in power generation, cement production, and other industrial sectors where large volumes of ash need to be transported. In power plants, for example, these systems are used to transport fly ash from the boiler to storage silos or to disposal sites. The benefits of using a well-designed conveying system include improved safety by reducing manual handling of ash, increased efficiency by automating the transport process, and cost savings through reduced labor and maintenance. Additionally, by minimizing dust emissions, these systems help facilities comply with environmental regulations and maintain a healthier working environment for personnel.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing high-quality dry ash powder conveying systems tailored to the needs of various industries. With a focus on innovation and customer satisfaction, the company has built a reputation for delivering reliable, efficient, and environmentally friendly equipment. HeadPowder’s systems are engineered to meet the specific requirements of each client, ensuring optimal performance and long-term durability. The company’s headquarters is located in Shandong, China, where it leverages advanced manufacturing techniques and a team of experienced engineers to develop cutting-edge solutions for ash handling and material transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top