Calcium phosphate powders are widely utilized across various industrial sectors, including pharmaceuticals, food processing, and chemical manufacturing. The efficient and reliable handling of these powders is paramount for maintaining product quality, ensuring process consistency, and optimizing operational efficiency. This article provides an overview of calcium phosphate powder handling systems and explores the core design principles that underpin their functionality.
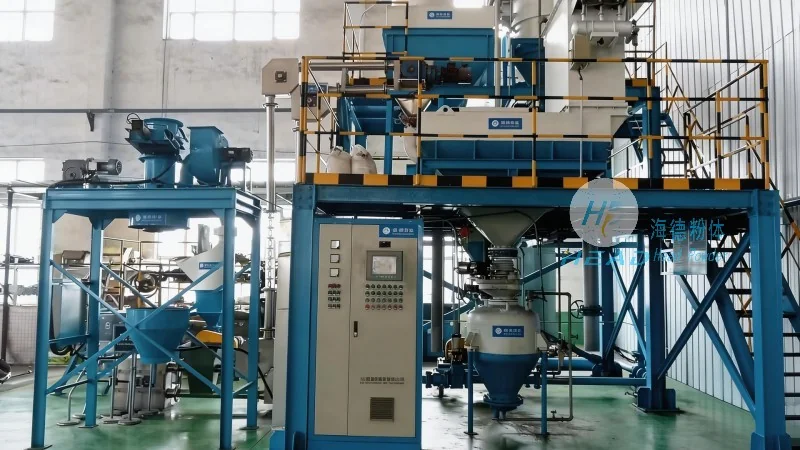
A calcium phosphate powder handling system typically comprises several interconnected components that work together to manage material flow, storage, and transport. Key elements include feeders, conveyors, storage silos, and control systems. Each component is selected and designed to address specific challenges associated with handling cohesive or flowable powders, such as segregation, bridging, and material degradation.
The design of a calcium phosphate powder handling system is guided by several critical principles aimed at maximizing efficiency, safety, and product integrity. One of the primary principles is the minimization of material degradation and segregation. This is achieved through the use of appropriate equipment like rotary valves, screw conveyors, and air slides, which help maintain the uniformity of the powder. Another key principle is the prevention of caking or agglomeration, which can occur due to moisture or particle interactions. Proper aeration and discharge mechanisms are essential to mitigate these issues.
Feeder selection is a critical aspect of system design. For calcium phosphate powders, which can exhibit varying flow characteristics (from free-flowing to cohesive), the choice of feeder (e.g., vibratory feeders, loss-in-weight feeders, or rotary valves) is essential to ensure consistent and controlled material flow. Proper feeder design helps prevent issues like rat-holing, bridging, and uneven discharge, which can lead to process inefficiencies or equipment damage. For cohesive powders, specialized feeders with adjustable vibration or pressure may be required to maintain stable flow rates.
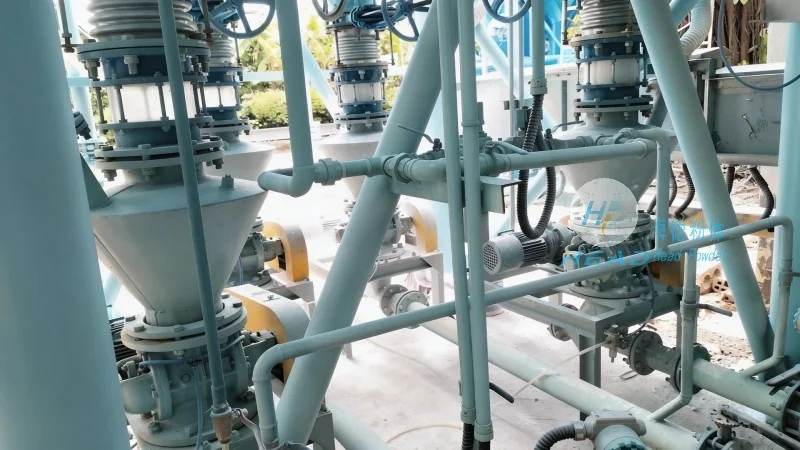
Conveyor systems are responsible for transporting the calcium phosphate powder from one location to another within the facility. Common types include belt conveyors, pneumatic conveying systems, and screw conveyors. The choice of conveyor depends on factors such as the powder's particle size, moisture content, and the distance to be covered. Pneumatic conveying, for example, is often preferred for fine powders due to its ability to handle dust, maintain product cleanliness, and transport materials over longer distances without the need for multiple transfer points. Screw conveyors, on the other hand, are suitable for bulk handling and can be used horizontally or at an incline, making them versatile for various applications.
Storage silos are integral to powder handling systems, providing a means to store large quantities of calcium phosphate powder while preserving its quality. The design of these silos must consider factors like material compatibility (to prevent corrosion or chemical reactions), structural integrity, and the prevention of caking or agglomeration. Proper aeration and discharge mechanisms are also crucial to ensure smooth material release from the silo. Silos may be equipped with internal agitators or vibrators to prevent material from settling and forming compacted layers that could impede discharge.
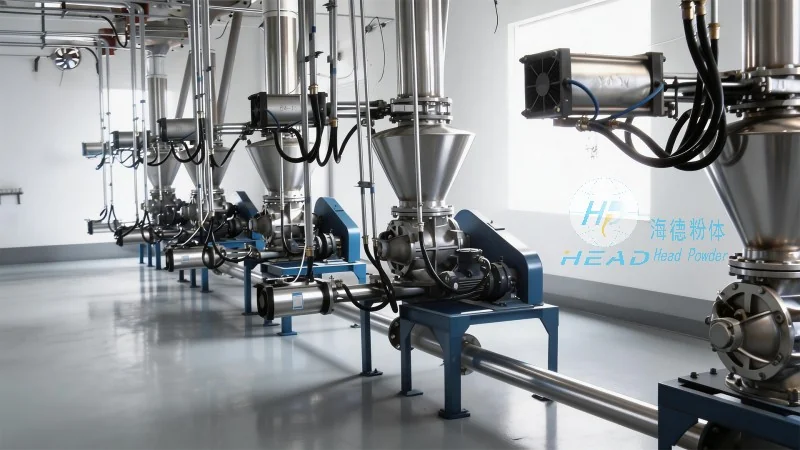
Modern calcium phosphate powder handling systems often incorporate advanced control and automation features to enhance operational efficiency and safety. These systems may include sensors for level monitoring, pressure measurement, and flow control, as well as programmable logic controllers (PLCs) that manage the entire process. Automation helps in maintaining consistent product quality, reducing human error, and improving overall process reliability. Real-time data collection and analysis can also be integrated to enable predictive maintenance and optimize system performance over time.
When integrating a calcium phosphate powder handling system into an existing facility, several factors must be considered to ensure seamless operation. These include space constraints, existing infrastructure, and the need for compatibility with other equipment. Proper system integration ensures that the new handling system works harmoniously with the rest of the production line, minimizing downtime and maximizing productivity. Additionally, adherence to safety standards and regulations is critical, particularly when handling powders that may pose dust explosion risks or other hazards.
Calcium phosphate powder handling systems are essential for the efficient and safe processing of these critical materials. By adhering to the fundamental design principles outlined above, manufacturers can develop systems that optimize performance, maintain product quality, and enhance operational efficiency. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. plays a vital role in designing and implementing such systems, ensuring that industrial processes run smoothly and reliably. With careful consideration of material properties, equipment selection, and system integration, calcium phosphate powder handling systems can deliver consistent results and contribute to the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top