Calcined ash powder conveying systems are specialized industrial equipment designed to handle and transport calcined ash, a byproduct of coal combustion. These systems are crucial in power plants and other industrial facilities where efficient material handling is essential for operational efficiency and safety. The equipment is engineered to ensure the reliable and safe transport of calcined ash from storage areas to processing or disposal sites, minimizing dust emissions and optimizing material flow. Calcined ash is a fine, dry powder with specific bulk density and flowability, which requires specialized equipment to handle effectively. The systems are designed to address the challenges associated with transporting such materials, including dust generation, material segregation, and the need for low maintenance.
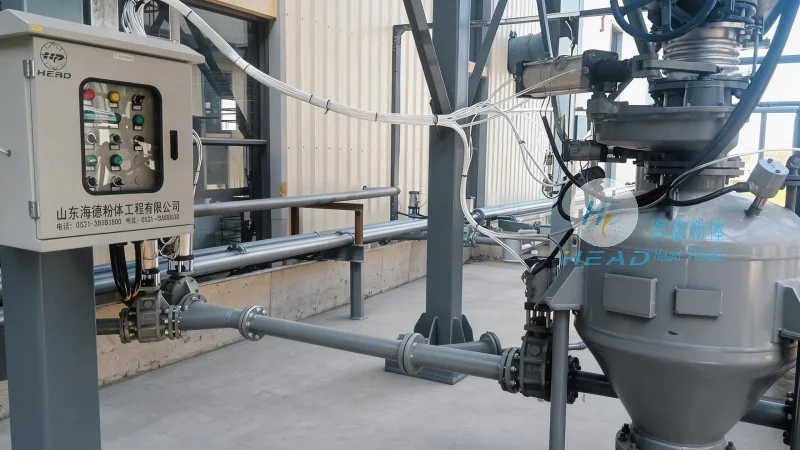
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of calcined ash powder conveying systems. The company has a strong reputation for delivering high-quality, reliable equipment that meets the demanding requirements of industrial clients. With a team of experienced engineers and technicians, HeadPowder develops customized solutions that are tailored to the specific needs of each project. The company's facilities in Shandong are equipped with advanced manufacturing capabilities, ensuring that the equipment is produced to the highest standards of quality and durability.
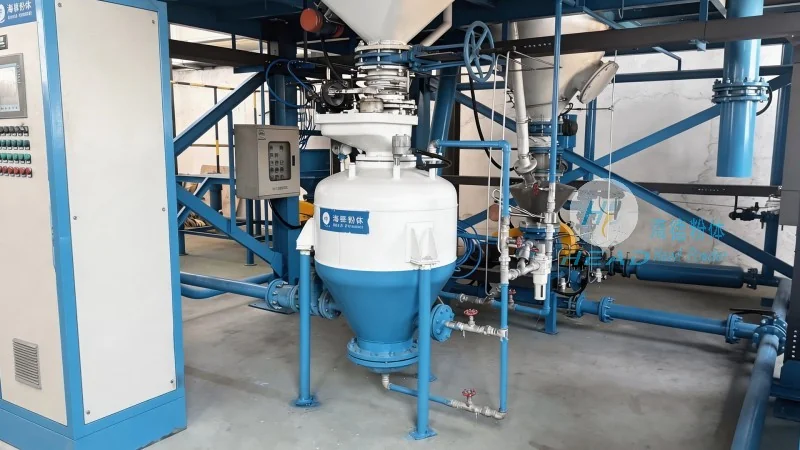
The design principles of calcined ash powder conveying systems are based on a thorough understanding of the material's properties and the operational requirements of the application. Engineers at HeadPowder conduct detailed analyses of the ash's characteristics, including its particle size distribution, moisture content, and bulk density. These parameters are critical in determining the most suitable conveying method. For example, if the ash has a high moisture content, a pneumatic system with a drying function may be preferred to prevent clogging and ensure smooth flow. If the ash is very fine and prone to dusting, a closed system with proper sealing is essential to maintain material integrity and prevent environmental contamination.
Another key design consideration is the conveying distance and layout of the system. The choice between pneumatic and mechanical conveyors depends on the distance and the need for flexibility. Pneumatic systems are ideal for long-distance transport and complex layouts, as they can navigate changes in direction and elevation with ease. Mechanical systems, such as screw conveyors, are more suitable for shorter distances and horizontal transport, offering a cost-effective solution for simple applications. The design also takes into account the energy consumption and operational costs, with the goal of minimizing both to enhance overall efficiency. HeadPowder's engineers use advanced computational fluid dynamics (CFD) and simulation tools to optimize the system design, ensuring that the final product meets the client's performance and cost targets.
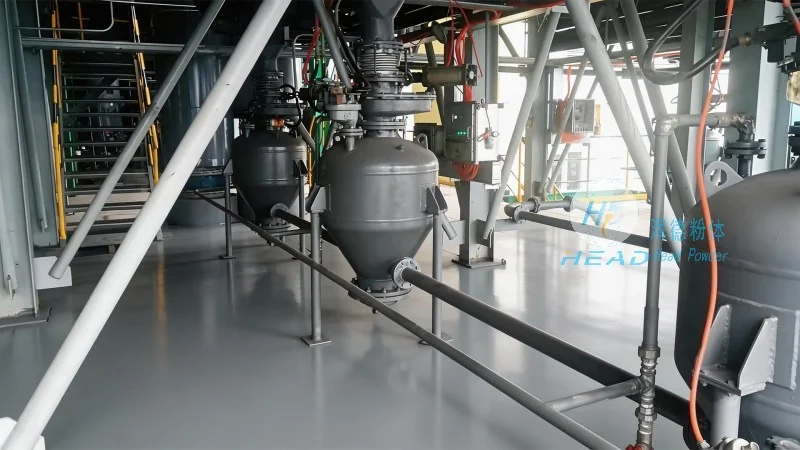
Key components of a calcined ash powder conveying system include the hopper, feeder, conveyor, control system, and auxiliary equipment. The hopper is a critical component that stores the calcined ash and feeds it to the conveyor. It is typically made of high-strength materials, such as stainless steel or carbon steel, to withstand the abrasive nature of the ash. The hopper is designed with a sloped bottom and a discharge opening that allows the ash to flow smoothly into the feeder. The feeder, often a rotary valve or a star feeder, regulates the flow rate of the ash into the conveyor, ensuring a consistent and controlled discharge. The feeder is also equipped with a seal to prevent dust leakage and maintain a clean environment. The conveyor itself, whether pneumatic or mechanical, is responsible for transporting the ash through the system. Pneumatic conveyors use air pressure to move the material through pipelines, while mechanical conveyors use rotating parts to push the material forward. The control system monitors and adjusts the operation of the components, ensuring smooth and safe operation. It includes sensors for flow rate, pressure, and temperature, as well as control panels for manual operation. Auxiliary equipment, such as dust collectors and filters, may be included to capture and remove any dust generated during the conveying process, ensuring compliance with environmental regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top