Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of pneumatic conveying technology. Based in Shandong, China, our company specializes in the design, manufacturing, and implementation of advanced coal ash particle pneumatic conveying systems. This article delves into the fundamental principles of such systems and highlights the key characteristics of their operational environments.
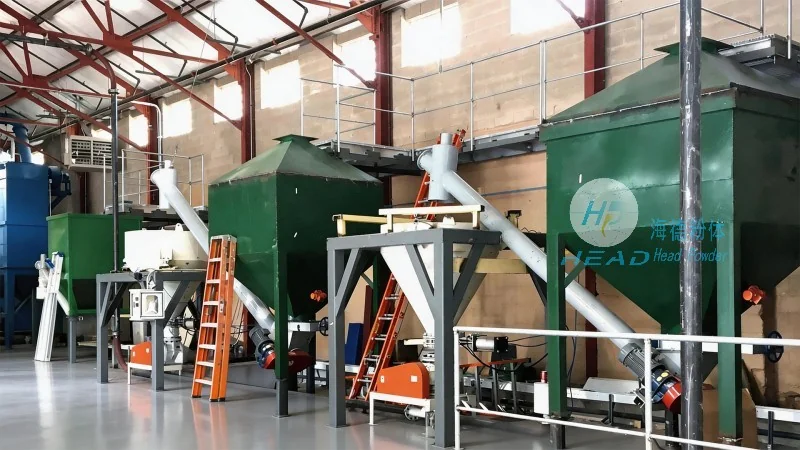
Shandong HeadPowder Engineering Co., Ltd. is dedicated to delivering high-efficiency and reliable solutions for material handling, particularly in the processing of coal ash. With a strong focus on pneumatic conveying systems, our company leverages decades of industry experience to develop tailored solutions that meet the specific needs of our clients. Our headquarters are located in Shandong, China, where we maintain state-of-the-art facilities for research, development, and production. We pride ourselves on our commitment to quality, innovation, and customer satisfaction, ensuring that every system we deliver is built to the highest standards.
The core principle of coal ash particle pneumatic conveying systems is the use of compressed air or gas to transport solid particles through a pipeline. This method, known as pneumatic conveying, involves creating a pressure differential that propels the material from the source to the destination. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The compressed air is introduced into the system, creating a flow that entrains the coal ash particles and transports them efficiently. This process eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs while improving safety in handling potentially hazardous materials.
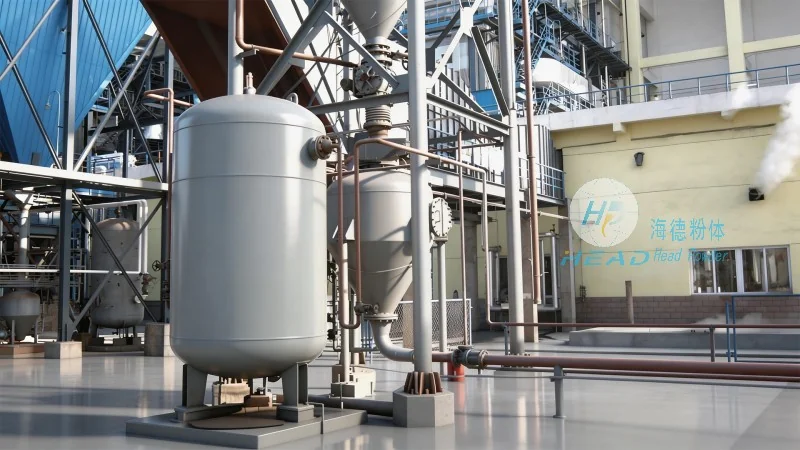
The operational environment of coal ash particle pneumatic conveying systems is characterized by several distinct features that influence system design and performance. Firstly, the material being conveyed—coal ash—often has specific properties such as high moisture content, abrasive nature, or varying particle sizes. These characteristics require specialized equipment to ensure efficient and reliable transport. Secondly, the systems are commonly used in industrial settings, including power plants, waste management facilities, and construction sites, where large volumes of material need to be moved over short to medium distances. The working scene may involve multiple transfer points, requiring flexible and adaptable system configurations. Additionally, the systems operate under varying pressure conditions, ranging from low to high pressure, depending on the distance and material characteristics. This adaptability allows for customization to meet the unique demands of each application.
Coal ash particle pneumatic conveying systems offer numerous advantages over traditional material handling methods. The primary benefit is the elimination of mechanical wear and tear, as there are no moving parts in direct contact with the material. This results in lower maintenance costs and longer system lifespans. Additionally, the systems provide a closed-loop operation, which helps in controlling dust emissions and maintaining environmental compliance. The flexibility of pneumatic conveying allows for easy integration with existing infrastructure, making it suitable for retrofitting in existing facilities. In coal ash handling, these systems are widely used for transporting ash from boilers to storage silos, or for moving ash to disposal sites. The ability to handle large volumes of material at high speeds makes them ideal for high-throughput applications, contributing to increased productivity in industrial operations.
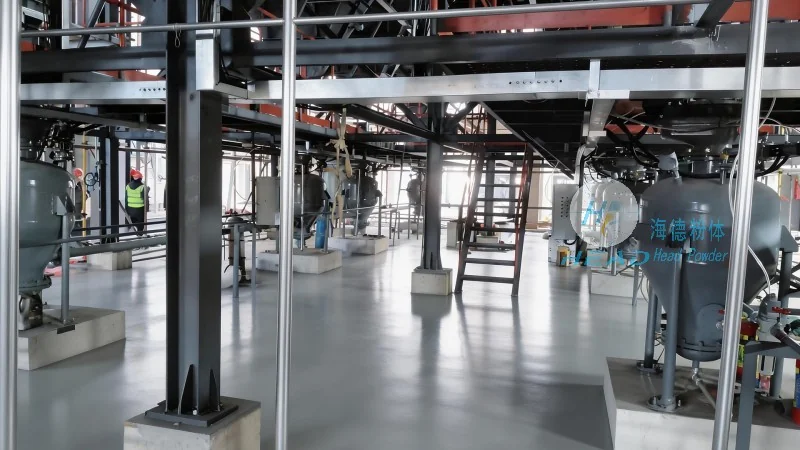
At Shandong HeadPowder Engineering Co., Ltd., we understand that each project has unique requirements. Therefore, our approach to designing coal ash particle pneumatic conveying systems involves a thorough analysis of the material properties, operational conditions, and client objectives. We work closely with clients to develop customized solutions that optimize performance and efficiency. Technical considerations include selecting the appropriate air pressure, determining the optimal conveying velocity, and ensuring the system’s compatibility with the existing infrastructure. Our team of engineers employs advanced computational fluid dynamics (CFD) and material flow analysis to simulate system performance, ensuring that the final design meets all safety and operational standards. This comprehensive approach guarantees that the delivered system is not only efficient but also reliable and durable.
In conclusion, coal ash particle pneumatic conveying systems represent a sophisticated and efficient solution for material handling in industrial applications. The fundamental principles of pneumatic conveying, combined with specialized design considerations, enable these systems to handle the unique challenges of coal ash transport. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing innovative and reliable systems that meet the evolving needs of the industry. As demand for efficient and sustainable material handling solutions continues to grow, our company is committed to advancing the technology and delivering solutions that enhance operational performance and environmental responsibility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top