High-temperature fine powder pneumatic conveying systems represent a sophisticated solution for transporting fine powders in industrial settings where elevated temperatures are prevalent. These systems are engineered to handle materials that are sensitive to heat or require efficient, dust-free transfer, making them indispensable in sectors such as cement production, power generation, and chemical processing. The technology leverages the principles of fluid dynamics and mechanical engineering to create a reliable and safe material handling process.
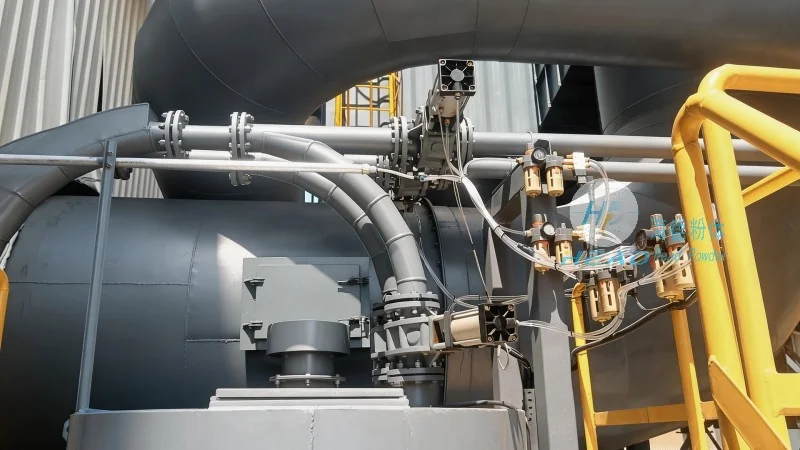
Shandong HeadPowder Engineering Co., Ltd. is a prominent manufacturer based in Shandong, China, specializing in the design, development, and implementation of pneumatic conveying systems. The company has built a strong reputation for delivering high-performance solutions tailored to the unique needs of various industries. With its headquarters located in Shandong, China, the firm leverages local industrial expertise and resources to provide innovative engineering services. HeadPowder focuses on creating systems that enhance operational efficiency, reduce maintenance costs, and ensure compliance with environmental regulations. The company's commitment to quality and customer satisfaction has positioned it as a leading provider in the pneumatic conveying industry.
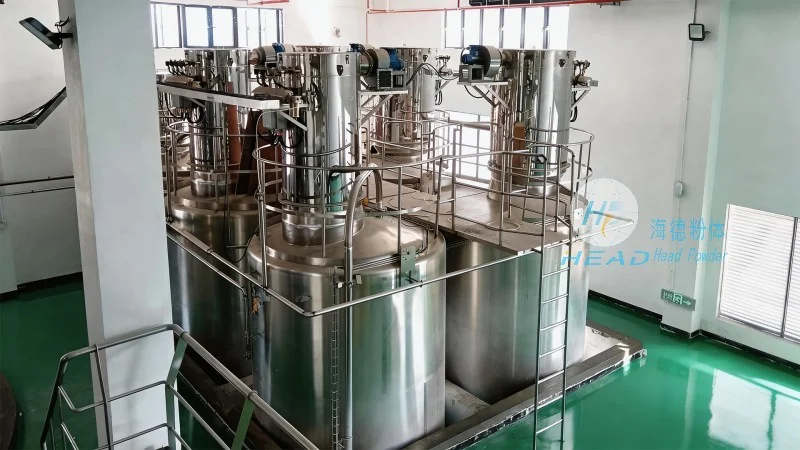
The fundamental principle of high-temperature fine powder pneumatic conveying systems is the use of pressurized air or gas to transport fine powders through a pipeline. The system operates by creating a flow of air that lifts and transports the powder particles. In high-temperature applications, specialized components are employed to withstand the heat, ensuring the system's durability and efficiency. The process typically involves several key components: a material feeder to introduce the powder into the system, a compressor to generate the necessary air pressure, a mixing chamber where the powder and air are combined, and a pipeline that transports the mixture to the destination. The design of the system is optimized to maintain the temperature of the powder while minimizing energy consumption and ensuring consistent flow rates. Advanced control systems are often integrated to regulate air pressure, flow rate, and temperature, allowing for precise operation and adaptability to varying material conditions.
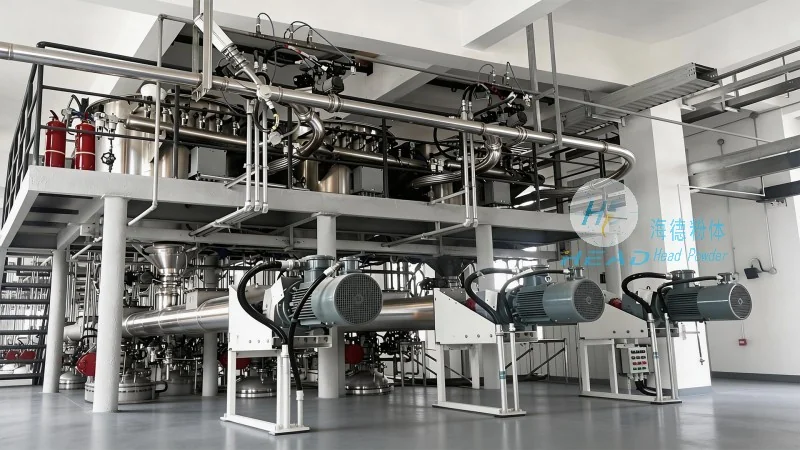
High-temperature fine powder pneumatic conveying systems are widely utilized in diverse industrial environments, each with distinct characteristics and requirements. In cement plants, these systems are critical for transporting raw materials such as limestone and clay, which are processed at high temperatures during the calcination stage. The systems must be capable of handling abrasive and heat-resistant materials while maintaining low dust emissions to meet environmental standards. In power plants, they are employed to convey fly ash and other fine powders generated during combustion, ensuring safe and efficient removal from the boiler and subsequent handling. The chemical industry also relies on these systems for transporting reactive powders, catalysts, and other materials that require controlled temperature and environment. The working scene characteristics include the need for robust equipment capable of withstanding harsh conditions, such as high temperatures, abrasive particles, and corrosive substances. The systems are designed with features like heat-resistant seals, corrosion-resistant materials (e.g., stainless steel, ceramics), and automated control mechanisms to enhance reliability and performance. Additionally, the systems are often integrated with dust collection and filtration systems to minimize environmental impact and ensure workplace safety.
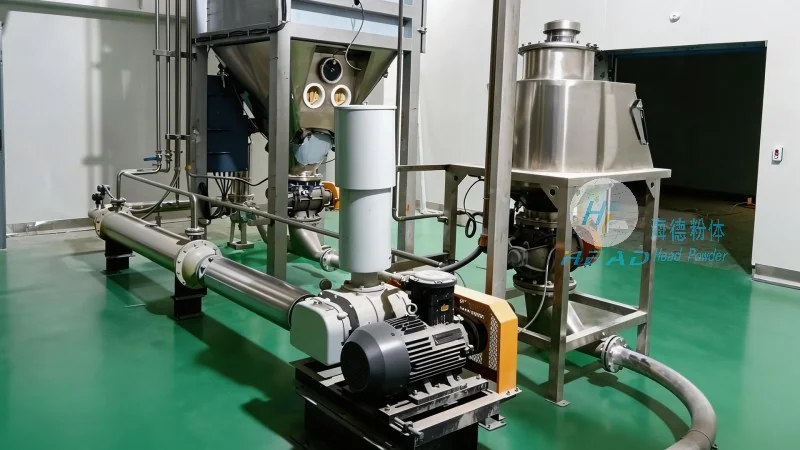
High-temperature fine powder pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the primary benefits is their ability to handle fine powders efficiently without the need for mechanical components that can cause blockages or wear. The systems are designed to maintain a consistent flow rate, reducing the risk of material buildup and ensuring smooth operation. Another key advantage is space efficiency, as they can transport materials over long distances without the need for multiple transfer points, which is particularly beneficial in large industrial facilities. The use of air as the conveying medium also reduces the risk of contamination and improves safety compared to methods involving direct contact with the material. Key features include adjustable air pressure and flow rate controls, temperature monitoring systems with real-time feedback, and automated shutdown mechanisms to prevent overheating or system failure. These features collectively contribute to the system's reliability, energy efficiency, and long-term operational performance. Furthermore, the systems are designed to minimize maintenance requirements through the use of durable materials and modular components, reducing downtime and operational costs for industrial users.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top