HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and implementation of efficient maltose pneumatic conveying systems. This article explores the fundamental principles behind these systems and highlights key application scenarios where they excel in material handling.
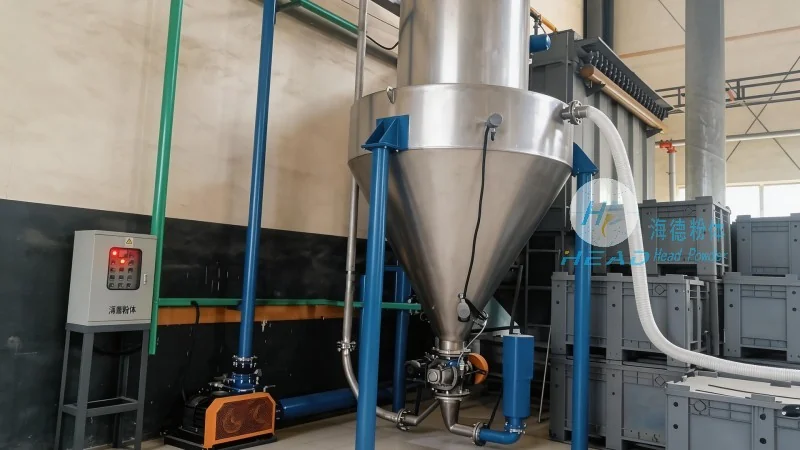
Maltose pneumatic conveying systems operate by transporting dry maltose powder or granules through a pipeline using a pressurized air or gas stream. The process involves several critical components that work in tandem to ensure reliable and efficient material movement. At the heart of the system is a blower or compressor that generates the necessary air pressure to create a flow within the pipeline. This air is then introduced into the conveying line, where it picks up the maltose particles and propels them to the destination point. The system typically includes a hopper for material storage, a rotary valve or feeder to control the flow rate, and a receiver or silo for the discharged material. The design of the pipeline, including the use of bends, elbows, and expansion joints, is crucial for minimizing pressure losses and preventing material buildup or blockages. The choice of air velocity and pressure is tailored to the specific properties of maltose, such as its particle size, density, and moisture content, to ensure optimal conveying efficiency and prevent product degradation.
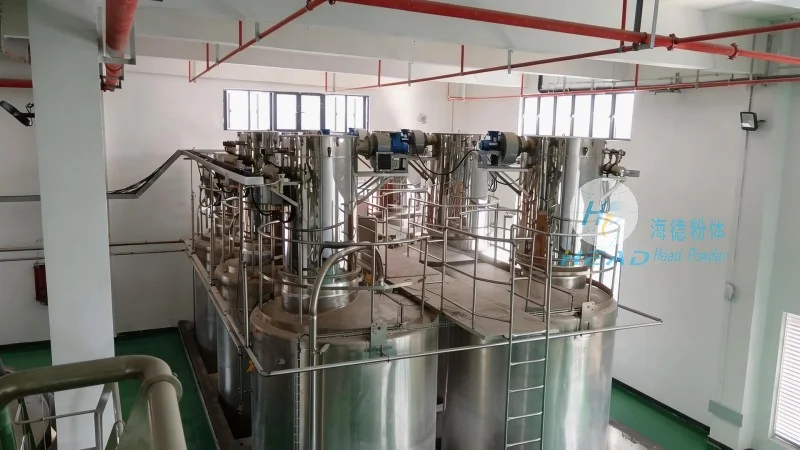
Maltose pneumatic conveying systems are widely used in various industrial settings due to their ability to handle delicate and hygroscopic materials like maltose. One primary application is in the food and beverage industry, where these systems are employed in the production of maltose-based products, such as syrups, candies, and baked goods. The systems are also utilized in pharmaceutical manufacturing, where the hygienic design and contamination control features are essential for handling maltose used as a sweetener or excipient. In the chemical industry, maltose is sometimes used as a raw material or intermediate, and pneumatic conveying systems facilitate its transfer between processing units. Additionally, in the agricultural sector, maltose produced from malted grains may be conveyed for further processing or packaging. The versatility of these systems allows them to adapt to different production scales, from small-scale laboratory operations to large-scale industrial plants.
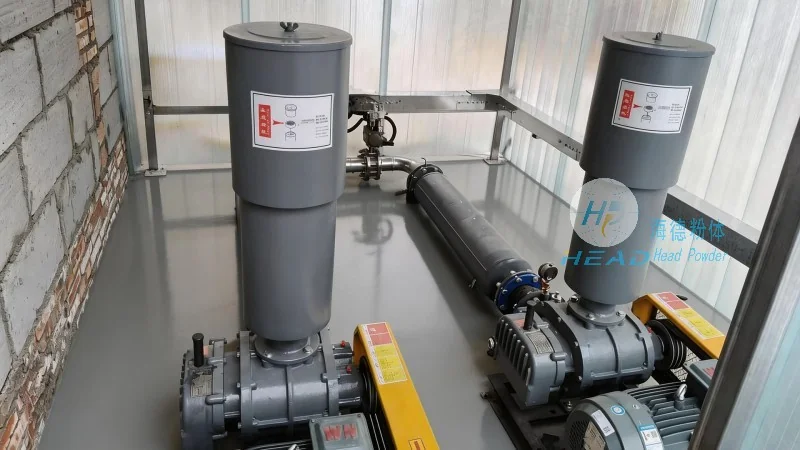
HeadPowder's maltose pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the most significant benefits is the ability to handle hygroscopic and sensitive materials without causing degradation or clumping. The enclosed pipeline design prevents exposure to moisture and contaminants, maintaining product quality throughout the conveying process. Additionally, these systems are highly efficient in terms of energy consumption, as the air pressure can be optimized to minimize energy usage while ensuring reliable material transport. The compact design of the system reduces floor space requirements, making it suitable for installations in limited areas. Furthermore, the systems are easy to clean and maintain, with features like CIP (Clean-In-Place) capabilities that allow for thorough sanitation without disassembling the equipment. The flexibility of the system allows for easy integration with existing production lines and the ability to adjust conveying rates based on production demands.
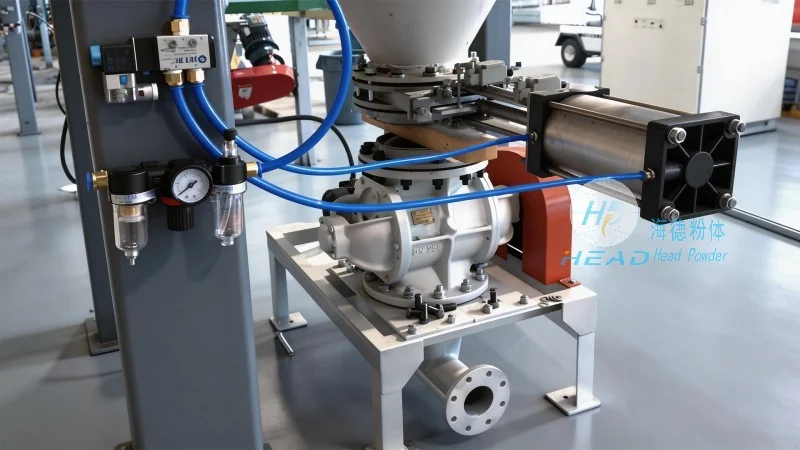
HeadPowder, with its headquarters in Shandong, China, provides tailored solutions for maltose pneumatic conveying systems that meet the specific needs of each client. The company's engineering team works closely with customers to assess their material handling requirements, production volumes, and operational constraints to design a system that maximizes efficiency and minimizes downtime. Customization options include the selection of appropriate blower types, pipeline materials (such as stainless steel or food-grade plastics), and control systems to ensure compliance with industry standards. HeadPowder also offers comprehensive after-sales support, including installation, commissioning, and ongoing maintenance services, to ensure the long-term performance and reliability of the conveying systems. By leveraging their expertise in pneumatic conveying technology, HeadPowder helps clients optimize their production processes and improve overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top