For industrial operations that require efficient and reliable material handling, dilute phase pneumatic conveying equipment stands out as a sophisticated solution. This technology, developed and manufactured by Shandong HeadPowder Engineering Co., Ltd., based in China, offers a versatile approach to transporting bulk materials through a pressurized air system. The following sections delve into the fundamental principles, operational characteristics, and practical applications of this equipment, highlighting its role in modern material handling processes.
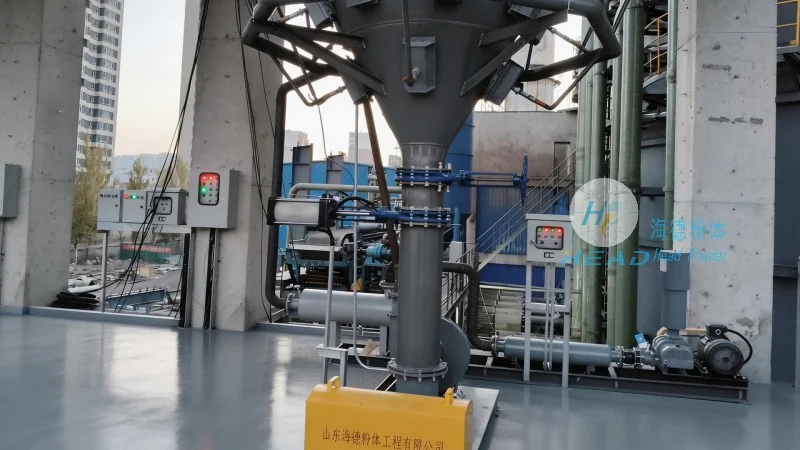
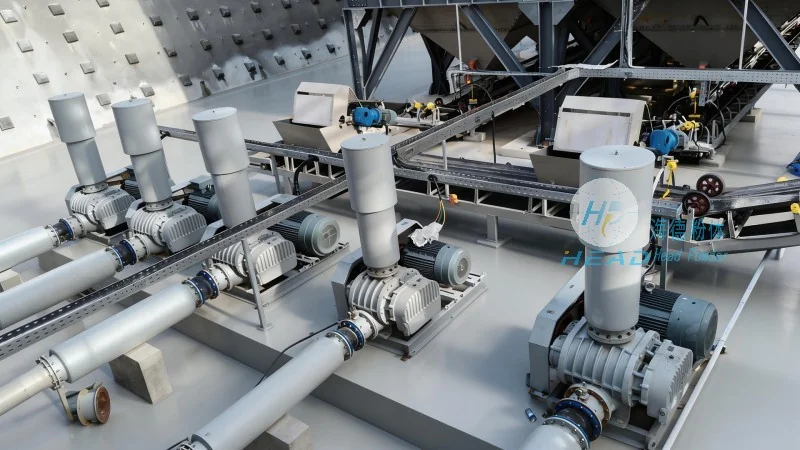
Dilute phase pneumatic conveying operates on the principle of transporting particulate materials in a low concentration within a carrier gas stream. Unlike dense phase systems, where material is conveyed in a more compact form, dilute phase systems rely on the momentum of the air to move particles through the pipeline. The process typically involves a positive pressure system, where air is compressed and introduced into the conveying line at a pressure higher than the ambient environment. As the air flows through the pipeline, it entrains the material particles, creating a suspension that travels to the destination point. The key to efficient operation lies in maintaining an optimal air-to-material ratio, which ensures consistent flow and minimizes pressure drop along the conveying line. Shandong HeadPowder Engineering Co., Ltd. specializes in designing systems that balance this ratio to achieve maximum throughput while preserving material integrity.
The versatility of dilute phase pneumatic conveying makes it suitable for a wide range of industrial applications. In the chemical industry, it is commonly used to transport powders such as polymers, pigments, and pharmaceuticals, where maintaining product purity and preventing contamination is critical. The food industry also benefits from this technology, as it allows for the safe and hygienic transfer of dry ingredients like flour, sugar, and spices. Additionally, in the mining sector, dilute phase systems are employed to move bulk materials like coal, ores, and minerals from processing plants to storage or shipping facilities. The equipment's ability to handle fine powders and abrasive materials without causing wear or degradation makes it a preferred choice in these sectors. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented dilute phase systems in various plants across China, demonstrating its adaptability to different material types and operational requirements.
One of the primary advantages of dilute phase pneumatic conveying is its ability to transport materials over long distances with minimal maintenance. Unlike mechanical conveyors, which require regular cleaning and replacement of components, pneumatic systems operate with fewer moving parts, reducing downtime and operational costs. The system's flexibility also allows for easy integration with existing infrastructure, making it a cost-effective upgrade for many facilities. Furthermore, dilute phase conveying offers superior control over material flow, enabling precise dosing and batching. This is particularly valuable in processes where consistent material quality is essential, such as in pharmaceutical manufacturing or food processing. Shandong HeadPowder Engineering Co., Ltd. emphasizes the importance of proper system design and maintenance to maximize the lifespan and efficiency of dilute phase equipment. Their engineering team provides comprehensive support, from initial system design to on-site installation and troubleshooting, ensuring that clients achieve optimal performance and reliability.
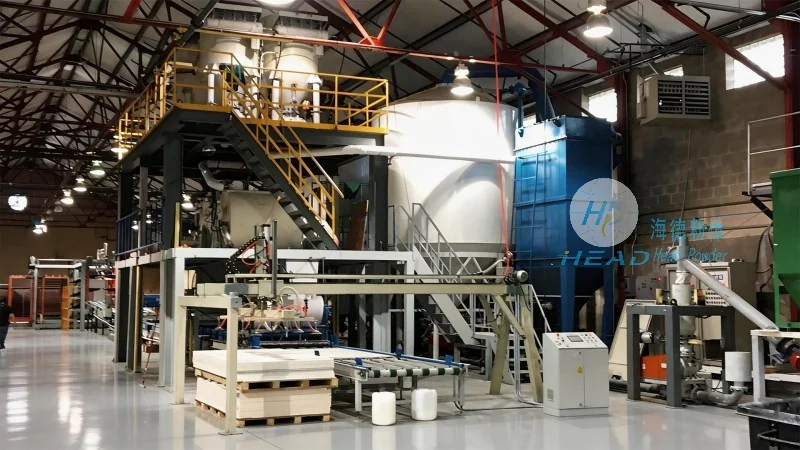
In summary, dilute phase pneumatic conveying equipment, as offered by Shandong HeadPowder Engineering Co., Ltd., represents a cutting-edge solution for efficient material handling in various industrial sectors. By leveraging the principles of air-based transport, this technology provides a reliable, flexible, and cost-effective method for moving bulk materials. The company's expertise in system design, manufacturing, and installation ensures that clients receive tailored solutions that meet their specific operational needs. With operations based in China, Shandong HeadPowder Engineering Co., Ltd. continues to serve industries worldwide, delivering high-quality dilute phase pneumatic conveying systems that enhance productivity and operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top