HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for calcite processing applications. This article delves into the fundamental principles behind these systems and highlights the key working scenario characteristics that make them ideal for calcite handling in various industrial settings.
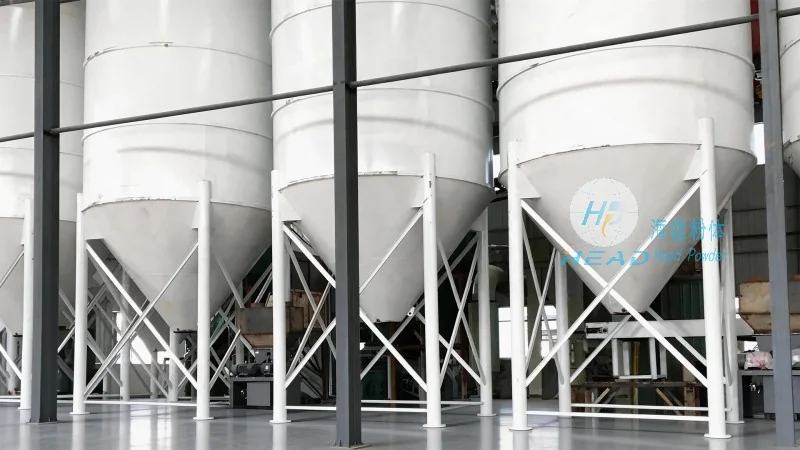
Calcite, a common calcium carbonate mineral, is widely used in industries such as construction, pharmaceuticals, and chemical manufacturing. Efficient and reliable material transport is crucial for optimizing production processes, and pneumatic conveying systems offer a solution that minimizes material degradation and operational costs. HeadPowder's expertise lies in developing customized systems that address the unique challenges associated with calcite, ensuring smooth and consistent material flow from source to destination.
Pneumatic conveying systems operate on the principle of using air or gas to transport bulk materials through a pipeline. In the case of calcite, the system typically employs a positive pressure or negative pressure (vacuum) method to move the material. The positive pressure system forces air through the pipeline, carrying the calcite particles, while the negative pressure system draws the material into the pipeline using a vacuum. HeadPowder's engineers design these systems to maintain optimal air velocity and pressure to prevent material segregation, caking, or degradation, which are critical for preserving the quality of calcite.
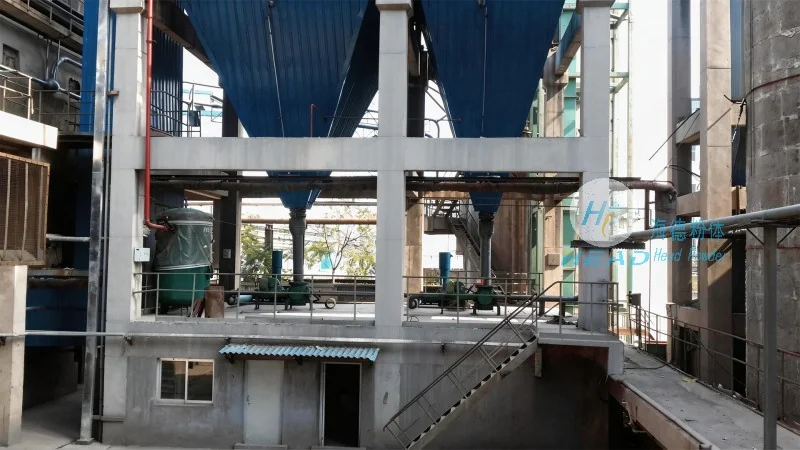
The effectiveness of a calcite pneumatic conveying system is heavily influenced by its working scenario characteristics. These include the material's physical properties, such as particle size, density, and moisture content, as well as the system's operational parameters like air flow rate, pressure, and pipeline configuration. HeadPowder's systems are engineered to accommodate varying calcite characteristics, ensuring consistent performance across different production scales. For instance, in large-scale calcite processing plants, the system may feature multiple inlets and outlets to handle high material throughput, while in smaller applications, a compact design is utilized to fit into limited space.
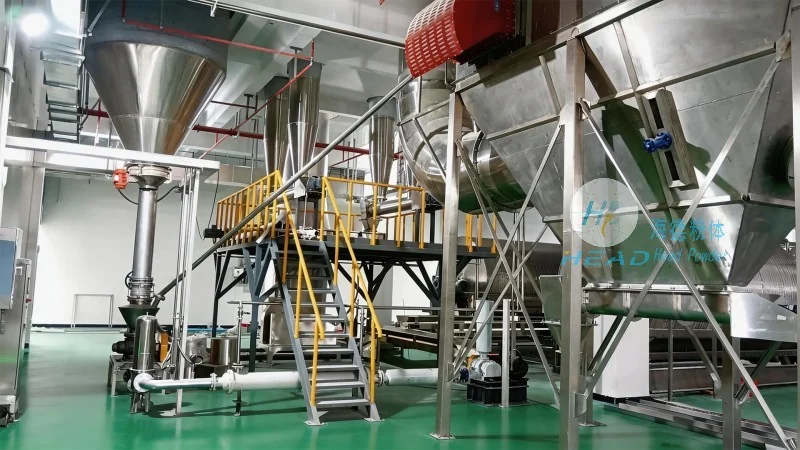
HeadPowder's calcite pneumatic conveying systems are equipped with several features that enhance their performance and reliability. These include advanced control systems for precise air pressure and flow management, high-efficiency filters to maintain air quality, and robust pipeline materials resistant to calcite's corrosive properties. The systems also incorporate safety mechanisms to prevent blockages and ensure smooth operation. By leveraging these features, HeadPowder's solutions provide significant advantages over traditional conveying methods, such as reduced labor costs, lower maintenance requirements, and improved material handling efficiency.
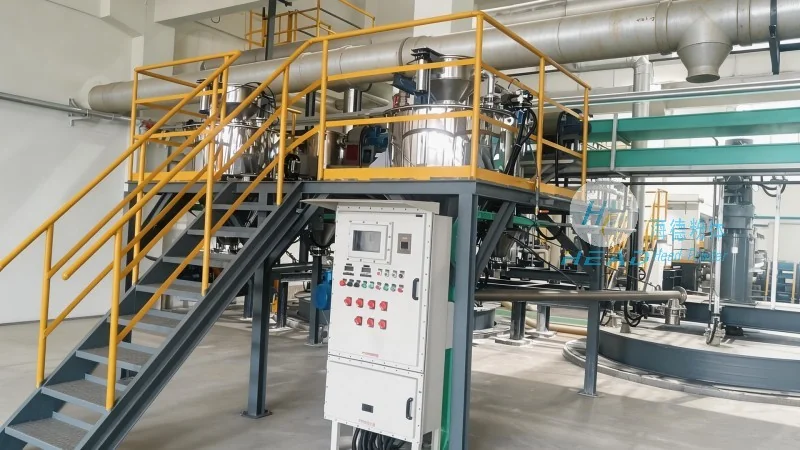
HeadPowder has successfully implemented calcite pneumatic conveying systems in various industrial applications. For example, in a construction material plant, the system was used to transport calcite from storage silos to grinding mills, achieving a 30% increase in production efficiency compared to traditional belt conveyors. In a pharmaceutical facility, the system ensured the safe and hygienic transport of calcite used in drug formulations, meeting stringent regulatory standards. These case studies demonstrate the versatility and effectiveness of HeadPowder's systems in different working scenarios, making them a preferred choice for calcite handling across industries.
HeadPowder's calcite pneumatic conveying systems represent a sophisticated solution for efficient material transport in calcite processing. By adhering to the core principles of pneumatic conveying and incorporating tailored working scenario characteristics, these systems offer reliable performance and cost savings. As technology advances, HeadPowder continues to innovate, developing systems that adapt to evolving industrial needs, ensuring that calcite handling remains efficient, safe, and sustainable. With a strong presence in Shandong, China, HeadPowder remains committed to providing high-quality engineering solutions that meet the demands of the calcite industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top