Phosphorus pentachloride (PCl₅) is a highly reactive and corrosive chemical widely used in the production of various industrial chemicals. The safe and efficient handling of PCl₅ is crucial due to its hazardous nature. Pneumatic conveying systems offer a reliable solution for transporting PCl₅ from storage to processing units, ensuring minimal exposure to personnel and reducing operational risks. This article explores the fundamental principles behind PCl₅ pneumatic conveying systems and highlights the key working scene characteristics that define their application in industrial settings.
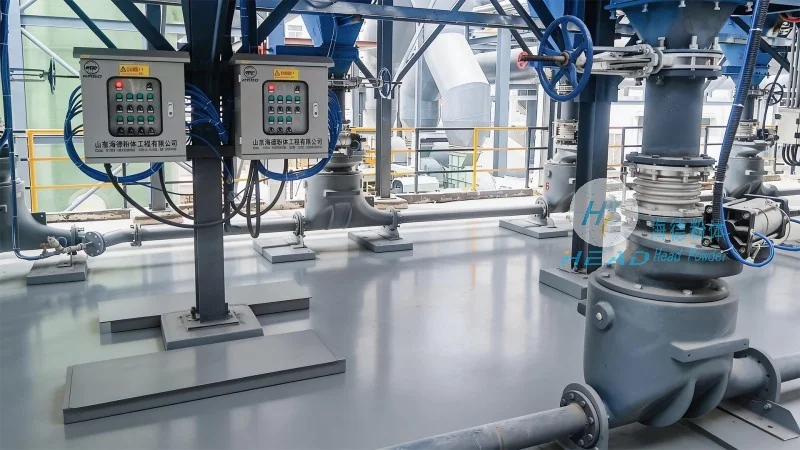
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in engineering solutions for chemical handling and processing. With a strong focus on safety, efficiency, and innovation, HeadPowder provides customized pneumatic conveying systems tailored to the unique needs of industrial clients. The company’s expertise in handling hazardous materials, such as phosphorus pentachloride, has established it as a trusted partner in the chemical industry. HeadPowder’s facilities are located in Shandong, China, where it leverages advanced technology and rigorous quality control to deliver high-performance conveying solutions.
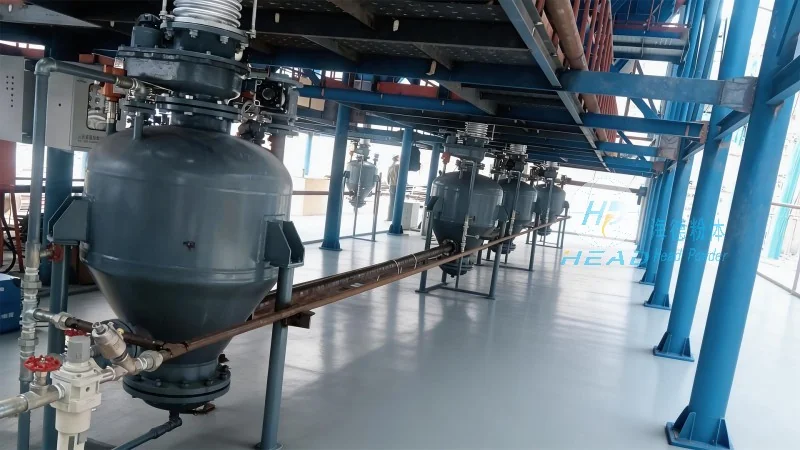
The core principle of a pneumatic conveying system for PCl₅ involves the use of compressed air to transport the solid material through a pipeline. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. The PCl₅ is fed into the hopper, where it is then metered by the rotary valve into the conveying line. Compressed air is introduced at the inlet of the line, creating a high-velocity flow that lifts and transports the PCl₅ particles. The velocity of the air must be sufficient to overcome the gravitational force and the frictional resistance of the particles, ensuring stable and continuous transport. The system may use either positive or negative pressure, depending on the specific application and the distance the material needs to travel. Positive pressure systems are commonly used for short-distance conveying, while negative pressure (or vacuum) systems are preferred for longer distances or when handling fine powders that are prone to dust dispersion.
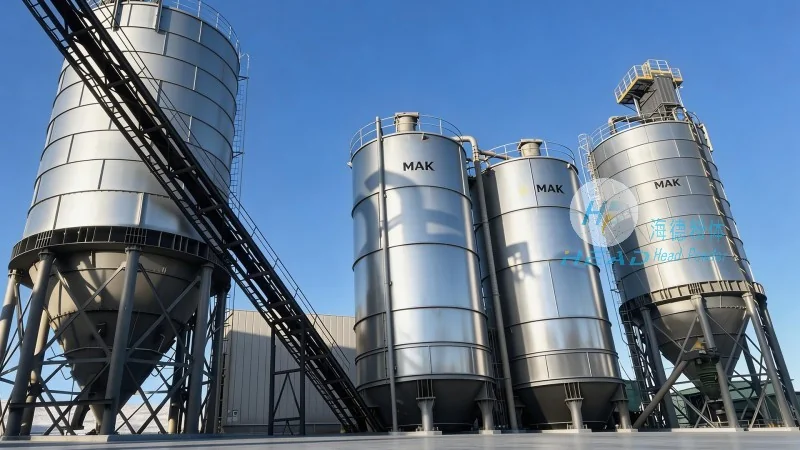
The working scene characteristics of PCl₅ pneumatic conveying systems are tailored to the specific requirements of industrial processes. These systems are designed to operate in environments where safety and efficiency are paramount. Key characteristics include:
PCl₅ pneumatic conveying systems are widely used in various industrial applications, including the production of pharmaceuticals, agrochemicals, and specialty chemicals. The primary operational benefits of these systems include:
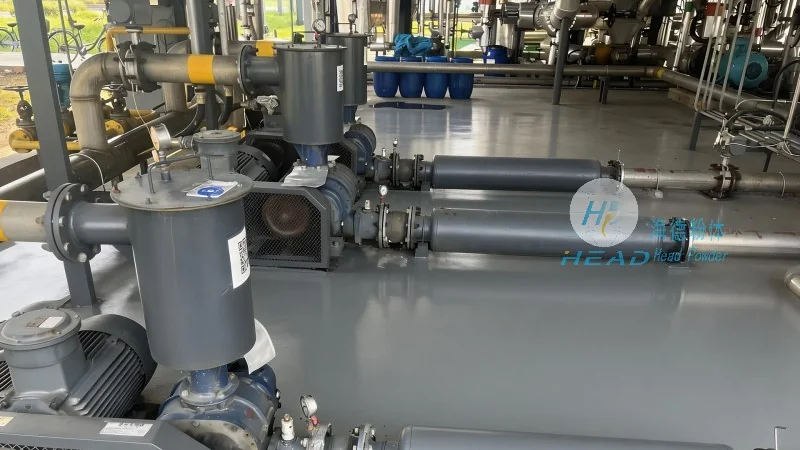
Phosphorus pentachloride pneumatic conveying systems, provided by Shandong HeadPowder Engineering Co., Ltd., represent a reliable and efficient solution for handling this hazardous chemical. By adhering to the fundamental principles of pneumatic transport and incorporating advanced safety and control features, these systems ensure safe and effective operation in industrial settings. The working scene characteristics, including corrosion resistance, temperature control, and dust suppression, are critical to maintaining the integrity of the system and protecting personnel and the environment. As a leading manufacturer in the field, HeadPowder continues to innovate and provide customized solutions that meet the evolving needs of the chemical industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top