Understanding the fundamental principles of airflow conveying is essential for optimizing material handling processes in various industrial applications. This article explores the core mechanisms of airflow conveying systems and highlights key operational characteristics across different working scenarios.
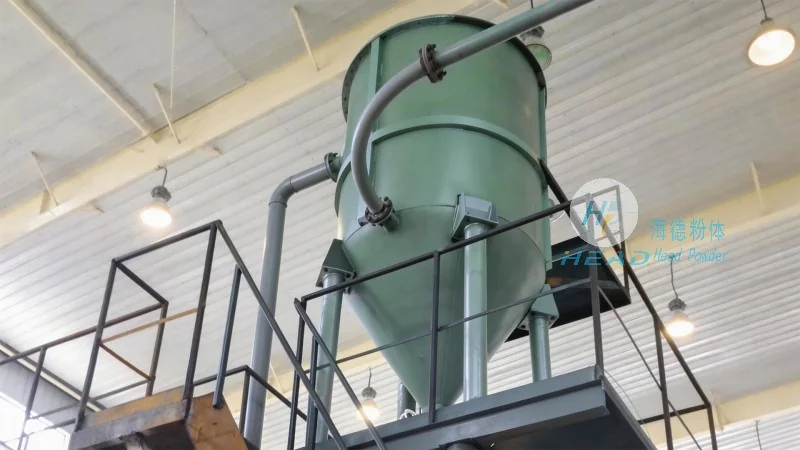
HeadPowder, a leading provider of material handling solutions, specializes in the design, manufacturing, and implementation of advanced airflow conveying systems. With a strong presence in China, particularly in Shandong province, the company leverages decades of industry expertise to deliver tailored solutions for diverse material handling challenges.
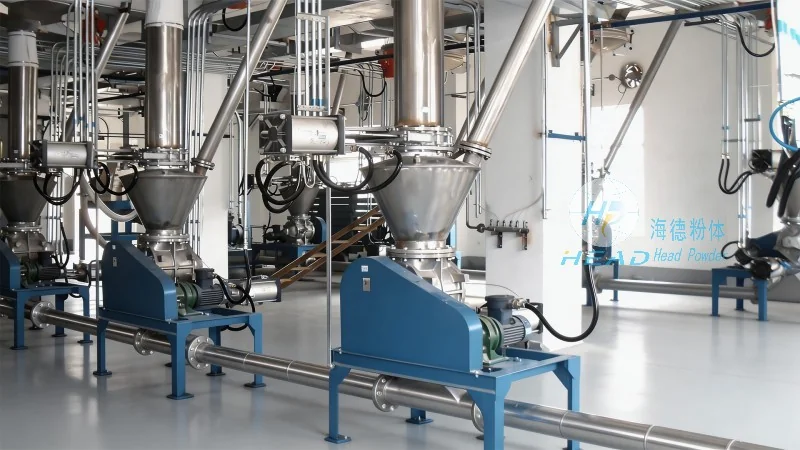
Airflow conveying, also known as pneumatic conveying, operates by transporting bulk materials through a pipeline using compressed air or other gases. The system typically consists of a hopper for material storage, a conveyor line with appropriate fittings, and a control system to regulate air pressure and flow. The primary mechanisms include pressure and vacuum conveying, each tailored to specific material properties and process requirements. Pressure conveying uses positive pressure to push material through the system, while vacuum conveying employs negative pressure to draw material into the pipeline. The choice between these methods depends on factors such as material density, particle size, and the distance over which material needs to be transported.
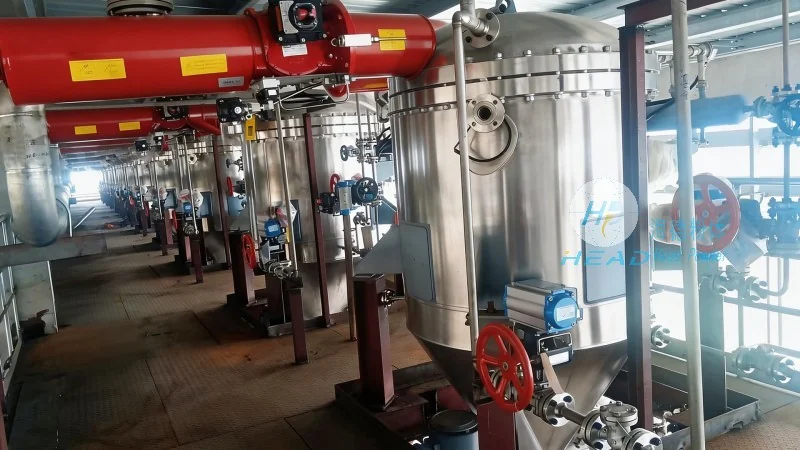
The effectiveness of airflow conveying systems is significantly influenced by the specific working scenarios in which they are deployed. For instance, in high-volume industrial settings, such as cement plants or chemical manufacturing facilities, the system's ability to handle large quantities of bulk materials efficiently is critical. The design of the conveyor line, including the selection of appropriate pipe diameters and the use of specialized fittings, directly impacts the system's capacity and reliability. In contrast, in smaller-scale applications like pharmaceutical or food processing industries, the focus shifts to maintaining product purity and preventing contamination. This often requires the use of closed systems with filtration and cleaning mechanisms to ensure compliance with regulatory standards.
Real-world applications of airflow conveying span a wide range of industries, from mining and mining-related processing to food and beverage production. In mining operations, the system is used to transport raw minerals from processing plants to storage facilities, where it must handle abrasive materials and varying particle sizes. The performance metrics, such as conveying velocity and pressure drop, are carefully monitored to ensure optimal operation and minimize energy consumption. In the food industry, the system is employed to transport ingredients like flour or sugar, where hygiene and product integrity are paramount. The use of stainless steel components and sealed systems helps maintain high standards of cleanliness, while the system's flexibility allows for easy integration into existing production lines.
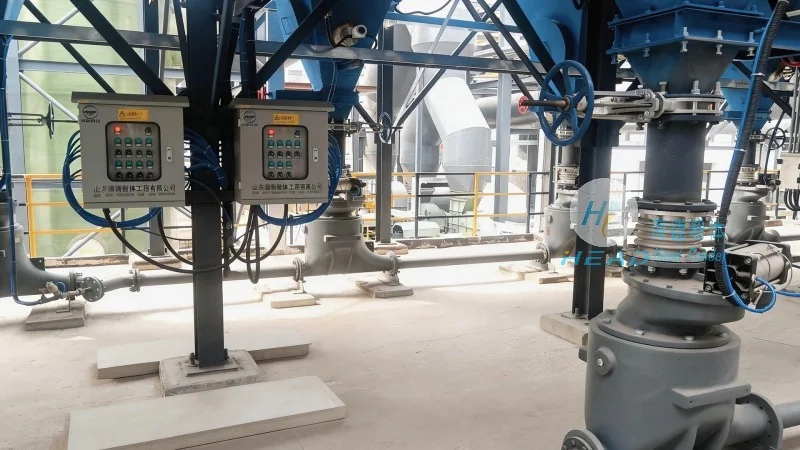
HeadPowder Engineering continues to innovate in the field of airflow conveying, offering customized solutions that address the unique challenges of each application. By combining advanced engineering with practical experience, the company ensures that its systems not only meet but exceed industry standards. With a strong commitment to quality and customer satisfaction, HeadPowder remains a trusted partner for businesses seeking reliable and efficient material handling solutions in China and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top