Understanding the fundamental principles and operational characteristics of pneumatic ash conveying is crucial for industries that rely on efficient waste management and material transport. This article delves into the core mechanisms of pneumatic ash conveying, highlighting its technical advantages and typical application environments. By exploring the underlying physics and practical implementation, we aim to provide a comprehensive overview that caters to professionals seeking reliable solutions for ash handling and transportation.
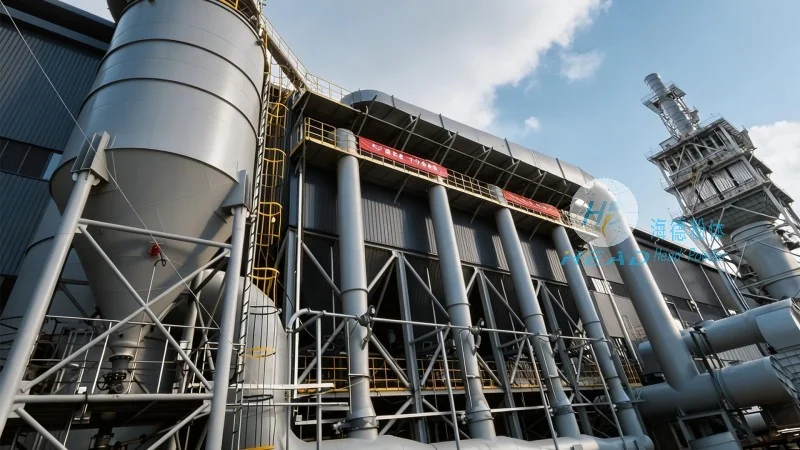
Pneumatic ash conveying operates on the principle of using compressed air to transport solid materials, such as fly ash, through a pipeline system. The process involves creating a pressure differential between the inlet and outlet of the conveying line, which propels the ash particles forward. Key components include the air compressor, dust collector, and conveying pipeline, each playing a vital role in ensuring smooth and efficient material movement. The system’s effectiveness is determined by factors like air velocity, particle size, and pipeline length, all of which must be optimized for specific operational conditions.
Pneumatic ash conveying is widely utilized across various industrial sectors, including power generation, metallurgy, and chemical processing. In power plants, for instance, it is employed to transport fly ash from boiler ash hoppers to storage silos or disposal sites. The system’s flexibility allows it to handle different ash types, from fine to coarse particles, making it adaptable to diverse plant configurations. Additionally, its ability to operate in both positive and negative pressure modes enables it to serve as a versatile solution for both ash removal and material recovery processes.
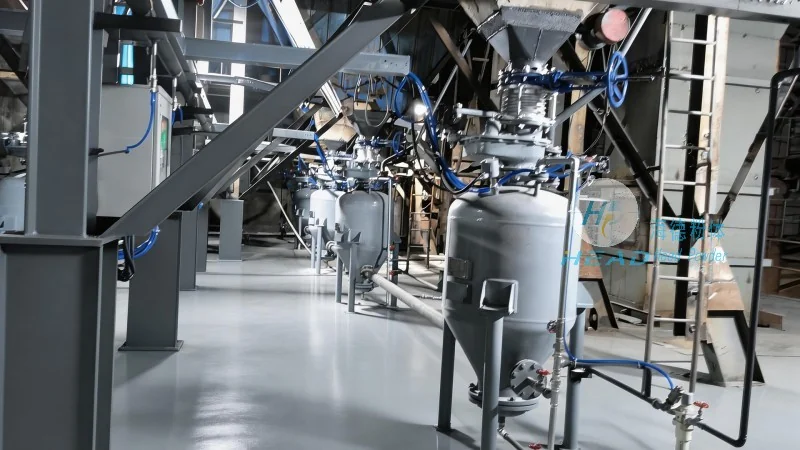
Compared to traditional mechanical conveying methods, pneumatic ash conveying offers several distinct advantages. It eliminates the need for moving parts, reducing maintenance requirements and operational downtime. The system’s compact design allows for easy integration into existing plant layouts, minimizing space constraints. Furthermore, it provides a dust-tight and enclosed environment, enhancing safety and environmental compliance. These benefits make pneumatic ash conveying an attractive choice for industries prioritizing efficiency, reliability, and cost-effectiveness.
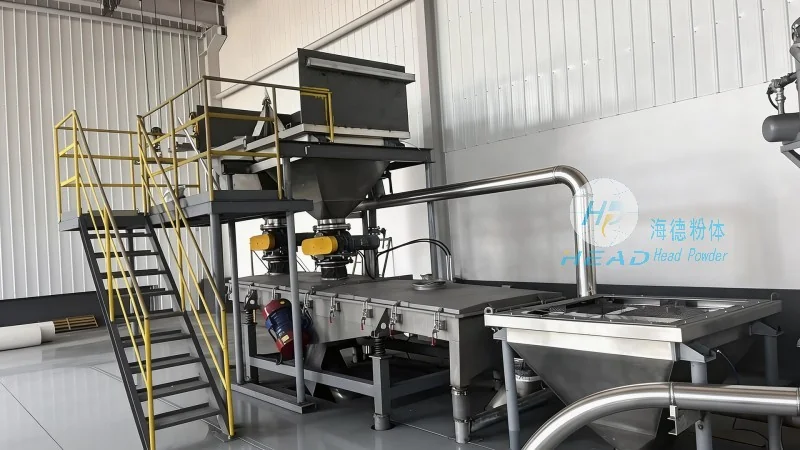
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced pneumatic ash conveying solutions. With a strong focus on innovation and customer-centric service, the company specializes in designing, manufacturing, and installing customized systems tailored to the unique needs of its clients. HeadPowder’s team of experienced engineers and technicians ensures that each project is executed with precision, adhering to international quality standards and industry best practices. The company’s headquarters is located in Shandong, China, where it maintains a state-of-the-art research and development facility to continuously improve its product offerings.
In summary, pneumatic ash conveying represents a highly effective and efficient method for handling and transporting ash materials. Its ability to adapt to various industrial applications, combined with the technical expertise of companies like Shandong HeadPowder Engineering Co., Ltd., makes it a preferred solution for modern waste management and material transport challenges. By understanding the core principles and operational scenarios, industries can make informed decisions to enhance their operational efficiency and environmental sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top