Salts, as a fundamental industrial and consumer product, require efficient and reliable transportation systems to ensure smooth operations from production to distribution. Among various conveying methods, air-flow conveying, also known as pneumatic conveying, has emerged as a preferred solution for salt handling due to its ability to transport bulk materials like salt with minimal mechanical contact and reduced risk of contamination. This article delves into the fundamental principles of salt air-flow conveying and explores the key characteristics of its working scenes, providing insights into how this technology optimizes salt processing and logistics.
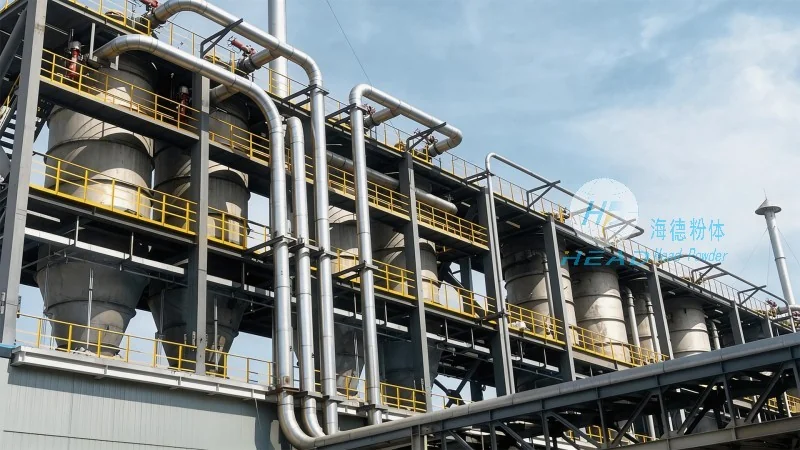
Salt air-flow conveying operates on the principle of using air as the medium to transport solid particles, such as salt granules, through a pipeline system. The process typically involves two main categories: positive pressure conveying and negative pressure (or vacuum) conveying. Positive pressure systems use a blower or compressor to generate air pressure that pushes the material through the pipeline, while negative pressure systems employ a vacuum pump to create a suction effect that draws the material into the pipeline. Both methods rely on the interaction between the air flow and the salt particles to achieve movement. The core components of a salt air-flow conveying system include a hopper for material storage, a feeder to control the flow rate, a conveyor line (pipeline), and a separator to separate the salt from the air at the discharge point. The system is designed to maintain consistent air velocity and pressure to ensure efficient and continuous transport of salt, minimizing issues like clogging or material degradation.
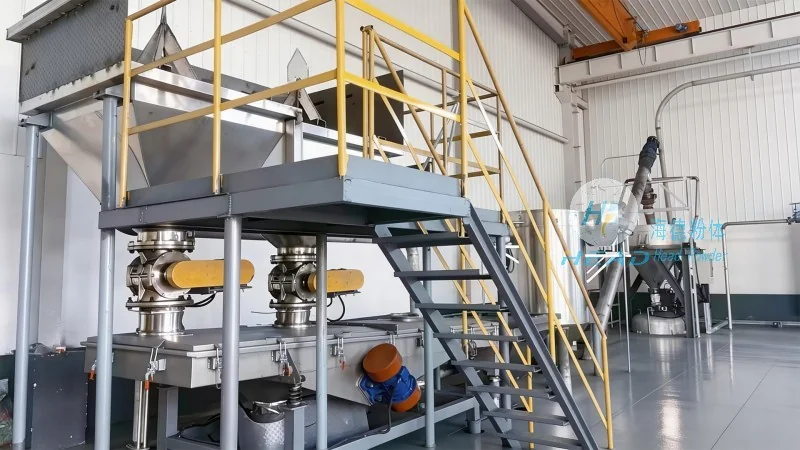
The application of salt air-flow conveying varies across different industrial settings, each with distinct characteristics that influence the system design and performance. In salt production facilities, for instance, air-flow conveying is commonly used to transport raw salt from mining or evaporation ponds to processing units, such as crushers or grinders. The system's ability to handle large volumes of salt with minimal labor makes it ideal for high-throughput operations. In storage and warehousing environments, air-flow conveying is employed to move salt between storage silos, loading docks, and packaging lines. This method ensures that salt is transferred without the need for manual handling, reducing the risk of dust exposure and product contamination. Additionally, in food processing and chemical industries, where salt is used as an ingredient, air-flow conveying maintains the purity of the material by avoiding contact with external contaminants. The flexibility of air-flow conveying systems allows them to adapt to different production scales, from small-scale operations to large industrial plants, making it a versatile solution for salt handling across various sectors.
When applied in specific working scenes, salt air-flow conveying exhibits several advantages that enhance operational efficiency and product quality. In industrial production lines, the system's ability to integrate with other equipment, such as conveyor belts or packaging machines, streamlines the entire workflow. The reduced need for manual intervention minimizes labor costs and improves safety in environments where salt dust can be a hazard. For example, in a salt processing plant, an air-flow conveying system can be connected to a grinder to transport crushed salt directly to a packaging line, eliminating the need for intermediate storage and reducing the risk of material loss. In storage facilities, the system's ability to handle bulk quantities efficiently reduces the space required for storage and simplifies inventory management. The low maintenance requirements of air-flow conveying systems, particularly when using high-quality materials for the pipeline and components, also contribute to long-term cost savings. Furthermore, the system's adaptability to different salt types, including table salt, industrial salt, and de-icing salt, makes it a versatile solution for various applications. These features collectively make salt air-flow conveying a preferred choice for companies operating in the salt industry, as it aligns with modern industrial standards for efficiency, safety, and sustainability.
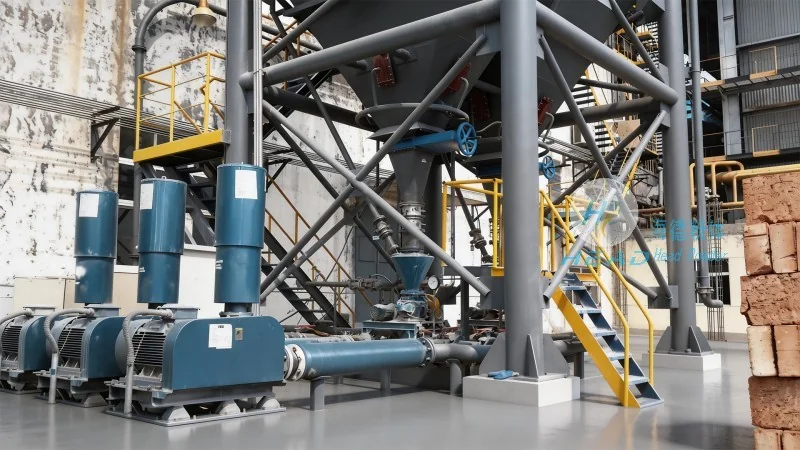
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for bulk material handling, including air-flow conveying systems for salt and other industrial products. With a focus on innovation and customer-centric design, HeadPowder has established itself as a trusted partner in the salt industry, offering tailored solutions that meet the unique needs of each client. The company's headquarters is located in Shandong, China, where it leverages advanced technology and extensive industry experience to develop and manufacture high-quality conveying systems. HeadPowder's commitment to quality and reliability ensures that its products are designed to withstand the demands of industrial environments, providing long-lasting performance and minimal downtime. By combining technical expertise with practical application knowledge, HeadPowder helps clients optimize their salt handling processes, enhance productivity, and maintain compliance with industry standards. Whether for new installations or system upgrades, HeadPowder offers comprehensive support, from initial consultation to installation and maintenance, ensuring that clients achieve their operational goals efficiently and effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top