Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a specialized enterprise dedicated to the design, manufacturing, and installation of pneumatic conveying systems for calcined ash. The company is headquartered in Shandong, China, and has established itself as a reliable partner in the field of industrial material handling solutions. With a focus on innovation and customer-centric service, headpowder delivers high-quality equipment tailored to the specific needs of clients in various industrial sectors.
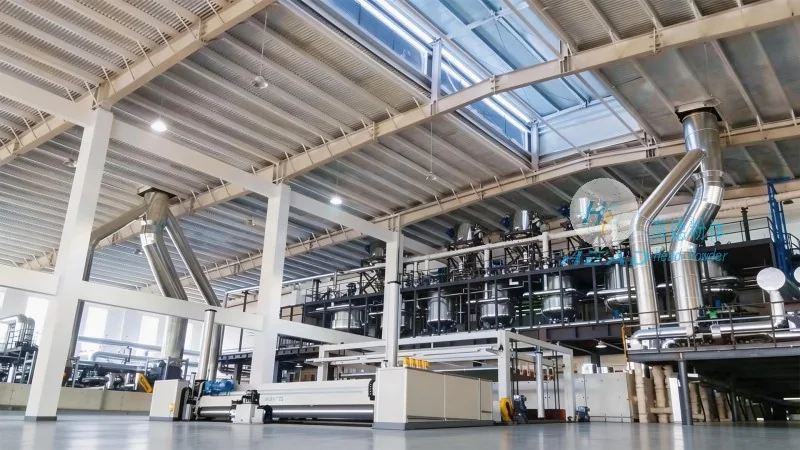
The core of headpowder's offerings is the pneumatic conveying system designed specifically for calcined ash. This system comprises several key components that work in harmony to ensure efficient and reliable material transport. The primary components include a dust collector, a conveying pipeline network, a blower or air compressor, and a control system. The dust collector is responsible for capturing and filtering the calcined ash particles, ensuring compliance with environmental regulations and maintaining air quality. The conveying pipeline network, typically made of high-quality stainless steel or other corrosion-resistant materials, is engineered to handle the abrasive nature of calcined ash, minimizing wear and extending the system's lifespan. The blower or air compressor provides the necessary air pressure to move the material through the pipeline, with options available to suit different capacity and distance requirements. The control system integrates all components, allowing for automated operation and real-time monitoring of the conveying process. Each component is meticulously designed and manufactured to meet industry standards, ensuring optimal performance and durability.
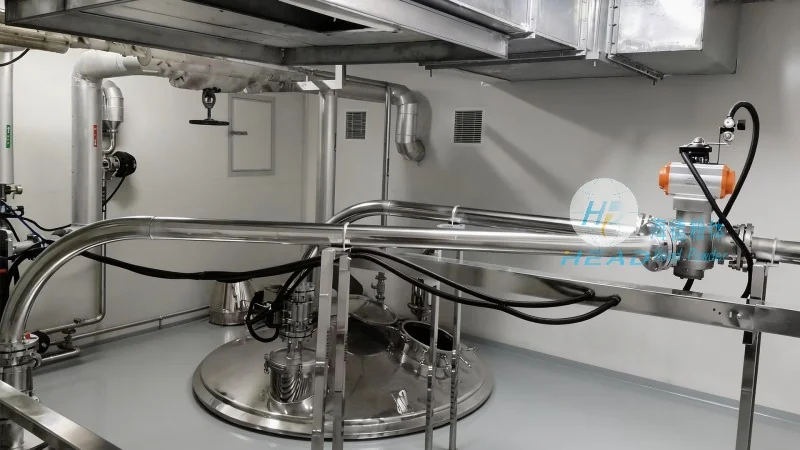
Headpowder's pneumatic conveying system for calcined ash offers several advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and clean conveying process, which is crucial for maintaining a safe and healthy working environment. Unlike traditional methods such as bucket elevators or belt conveyors, pneumatic systems eliminate the need for manual handling of bulk materials, reducing the risk of dust exposure and improving workplace safety. Secondly, the system offers high efficiency in material transport, with the ability to handle large volumes of calcined ash over long distances with minimal energy consumption. The design of the conveying pipeline and the control system ensures that the material is transported smoothly and without blockages, maximizing throughput and reducing downtime. Thirdly, the system is highly flexible and adaptable, allowing for easy integration with existing industrial facilities and the ability to expand or modify the system as production needs change. This flexibility makes it suitable for a wide range of applications, from small-scale operations to large industrial plants. Additionally, the system is designed for low maintenance, with components that are easy to access and replace, reducing operational costs and minimizing the need for frequent repairs.
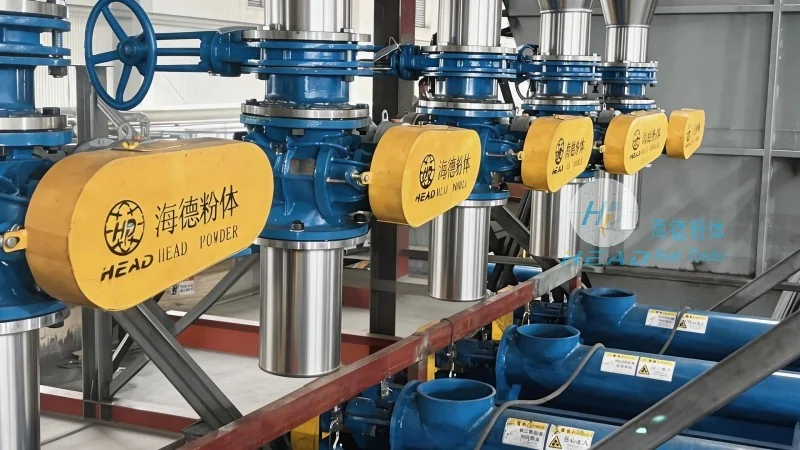
The pneumatic conveying system for calcined ash is widely used in various industrial sectors, including power generation, cement production, and waste management. In power plants, the system is used to transport calcined ash from the boiler to the storage silos or disposal sites, ensuring efficient and safe material handling. In cement plants, the system is used to convey calcined ash as a raw material or as a supplementary fuel, contributing to the production of high-quality cement. In waste management facilities, the system is used to transport calcined ash from incineration processes to landfills or recycling facilities, helping to manage waste more effectively. The system's versatility and reliability make it suitable for these and other applications where the efficient and safe handling of calcined ash is critical.
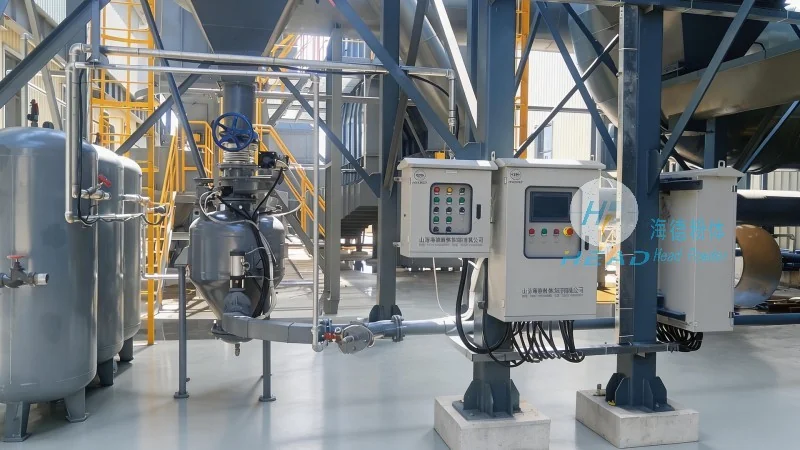
Headpowder provides comprehensive support to its clients, from the initial design and consultation phase to the installation and maintenance of the pneumatic conveying system. The company's team of experienced engineers and technicians work closely with clients to understand their specific requirements and develop customized solutions that meet their needs. The design process involves detailed calculations and simulations to ensure that the system is optimized for performance and efficiency. During the installation phase, headpowder's technicians ensure that the system is installed correctly and that all components are properly commissioned. After installation, the company provides regular maintenance and support services to ensure that the system operates at peak performance. This comprehensive approach to customer support ensures that clients receive the best possible service and that their investment in the pneumatic conveying system is protected.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top