Diatomite pneumatic conveying systems are integral to industrial processes that require the efficient handling of diatomite, a natural sedimentary rock known for its high porosity and exceptional filtration capabilities. Understanding the components that constitute such a system is essential for optimizing operational performance, ensuring reliability, and maximizing the lifespan of the equipment. This article provides a comprehensive overview of the key elements that make up a diatomite pneumatic conveying system, detailing how each component contributes to the overall transport process and highlighting the importance of proper integration and maintenance.
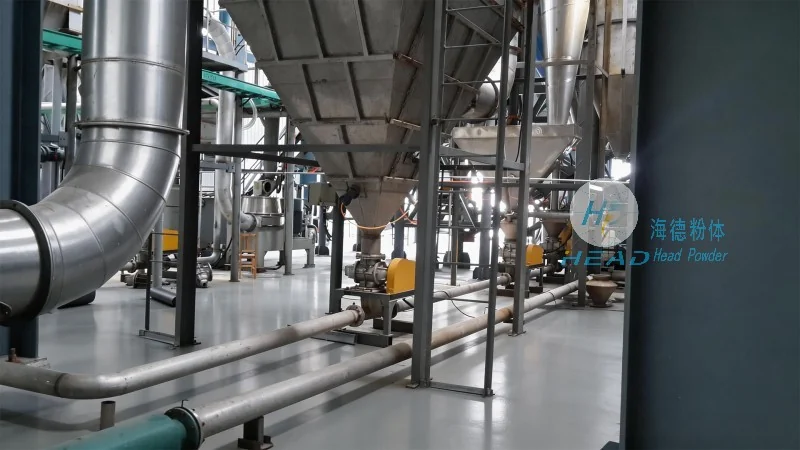
The fundamental components of a diatomite pneumatic conveying system typically include the material storage and feeding unit, the conveying pipeline network, the air supply and compression unit, and the control and monitoring system. Each of these elements is designed to work in concert to facilitate the movement of diatomite from its source to the desired destination. The material storage and feeding unit serves as the initial point of contact, holding the diatomite and controlling its discharge into the system. The conveying pipeline, often constructed from durable materials like stainless steel or high-density polyethylene, forms the path through which the diatomite and air mixture travels. The air supply unit generates the necessary pressure and airflow to propel the material, while the control system regulates the flow and monitors system parameters to prevent issues like blockages or overpressure.
The material feed and storage unit is a critical component that ensures a steady and controlled supply of diatomite to the pneumatic conveying system. This unit is typically a hopper or silo designed to hold a sufficient quantity of diatomite, with features such as a gate or valve to regulate the flow rate. For diatomite, which can be fine and prone to bridging or caking, the hopper may include pre-drying or pre-screening mechanisms to remove moisture and oversized particles, preventing blockages in the downstream pipeline. The design of the feed hopper is crucial as it directly impacts the system's ability to maintain a consistent flow, which is essential for preventing pressure surges and ensuring smooth operation. Additionally, the unit may be equipped with level sensors to monitor the material inventory, alerting operators when the hopper is low and requiring replenishment.
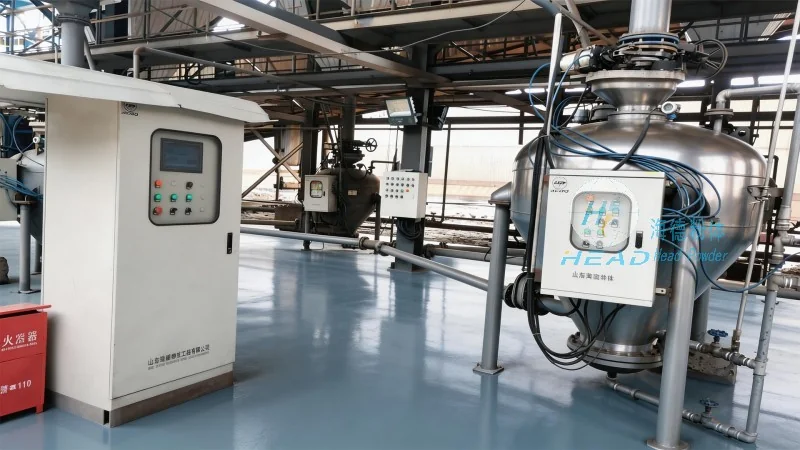
The conveying pipeline is the central conduit of the pneumatic conveying system, responsible for transporting the diatomite and air mixture from the feed hopper to the discharge point. The pipeline is constructed from materials that can withstand the abrasive nature of diatomite and the pressure of the air flow. Stainless steel is a common choice due to its corrosion resistance and durability, while some systems may use plastic pipes for applications where weight or cost is a factor. The pipeline diameter is carefully selected to balance the flow rate and pressure drop, ensuring that the system operates efficiently without excessive energy consumption. The pipeline layout, whether in a straight line or a loop configuration, is determined by the facility's layout and the distance between the source and destination. Additionally, the pipeline includes bends, elbows, and other fittings that are designed to minimize pressure losses and prevent material accumulation or blockages, with smooth transitions to maintain consistent flow.
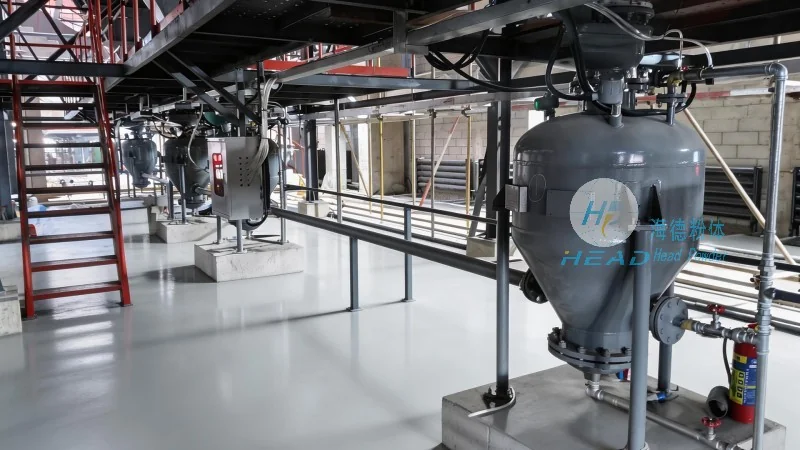
The air supply and compression unit is the energy source for the pneumatic conveying process, providing the necessary airflow and pressure to move the diatomite through the pipeline. This unit typically consists of a blower or compressor, with the choice depending on the specific application and the characteristics of the diatomite being conveyed. Blowers are often preferred for low-pressure, high-volume applications, as they are more energy-efficient and can handle larger volumes of material. Compressors, on the other hand, are suitable for high-pressure applications where the material is more abrasive or the distance to be conveyed is longer. The unit is equipped with filters and moisture separators to ensure that the air entering the pipeline is clean and dry, preventing contamination of the diatomite and reducing wear on the system components. The air pressure and volume are adjustable to match the requirements of the conveying system, allowing for flexibility in handling different material types and flow rates.
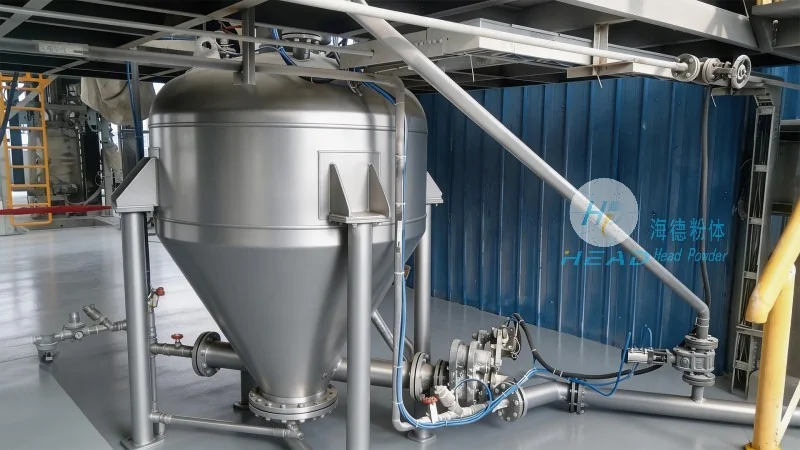
Control valves and monitoring sensors are essential for maintaining the stability and safety of the diatomite pneumatic conveying system. These components regulate the flow of air and material, monitor system pressure and flow rates, and detect potential issues such as blockages or overpressure. The control valves, which can be manual or automated, are used to adjust the air pressure and material flow rate as needed. For example, if the system detects a blockage in the pipeline, the control valves can be activated to reduce the flow or increase the air pressure to clear the obstruction. Sensors, such as pressure transducers, flow meters, and level sensors, provide real-time data on the system's performance, allowing operators to monitor and adjust the system parameters as required. Safety valves and pressure relief devices are also installed to prevent overpressure situations, ensuring the safety of the system and the personnel operating it. The integration of these control and monitoring components enhances the system's reliability and reduces downtime due to operational issues.
The successful operation of a diatomite pneumatic conveying system relies on the proper integration of all components and regular maintenance. The system components must be matched to the specific characteristics of the diatomite, such as particle size, moisture content, and flow properties, to ensure optimal performance. Regular maintenance, including cleaning the pipeline, replacing filters, and inspecting valves and sensors, is essential to prevent wear and tear and maintain system efficiency. Additionally, training operators on the proper use and monitoring of the system can help identify issues early and prevent major failures. By following best practices for integration and maintenance, users can maximize the lifespan of their diatomite pneumatic conveying system and ensure consistent, reliable performance in their industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top