Slurry pneumatic conveying is a sophisticated method for transporting particulate materials suspended in a fluid, typically air or gas, through a pipeline system. This technology is particularly effective for handling materials that are difficult to convey using traditional methods, such as those with high moisture content, abrasive properties, or varying particle sizes. The core principle involves creating a flow of air that lifts and transports the slurry mixture through the pipeline, ensuring efficient and reliable material movement from the source to the destination.
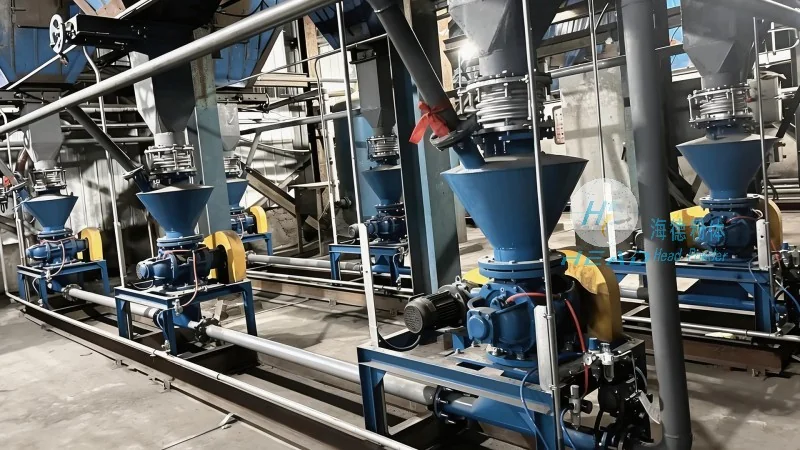
The operation of slurry pneumatic conveying is based on several key principles that ensure the effective transport of materials. First, the creation of a sufficient air velocity within the pipeline is crucial. This velocity must be high enough to overcome the gravitational forces acting on the particles and maintain them in suspension. The air velocity is typically calculated based on the specific properties of the slurry, including particle size, density, and moisture content. Second, the system must maintain a consistent pressure and flow rate to prevent clogging and ensure smooth operation. This is achieved through the use of specialized equipment such as blowers, pumps, and control valves that regulate the air and slurry mixture. Third, the design of the pipeline system, including the diameter, length, and bends, plays a critical role in minimizing pressure losses and maintaining the stability of the slurry flow. Properly sized and positioned elbows, tees, and other fittings are essential to avoid turbulence and ensure the material remains in suspension throughout the conveying process.
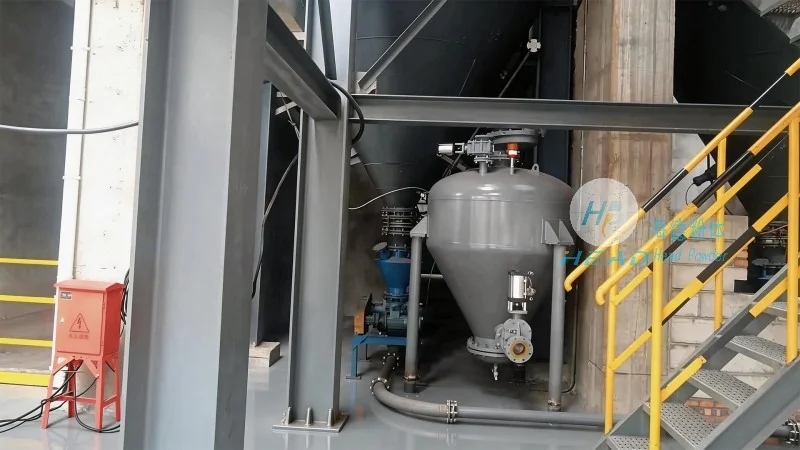
A slurry pneumatic conveying system consists of several essential components that work together to achieve efficient material transport. The primary components include a slurry pump or feed system that introduces the slurry into the pipeline, a blower or compressor that provides the necessary air pressure and flow, a pipeline network that transports the mixture, and a receiver or discharge system that collects the material at the end of the line. The slurry pump is responsible for feeding the slurry at a consistent rate, while the blower generates the air pressure required to lift and move the mixture. The pipeline system must be constructed from materials that are resistant to corrosion and abrasion, such as stainless steel or high-density polyethylene, to withstand the harsh conditions of slurry transport. Additionally, the system includes control devices such as pressure sensors, flow meters, and valves that monitor and regulate the operation of the system, ensuring optimal performance and preventing issues like clogging or overpressure.
Slurry pneumatic conveying is widely used in various industrial applications where the transport of difficult-to-handle materials is required. One of the most common applications is in the mining and mineral processing industry, where it is used to transport ore, tailings, and other mineral slurries from processing plants to storage facilities or for further treatment. The technology is also extensively used in the chemical and petrochemical industries, where it is employed to convey slurries containing chemicals, catalysts, or other reactive materials. In the food and beverage industry, slurry pneumatic conveying is used to transport ingredients such as fruit purees, dairy products, or other food materials that require gentle handling to maintain quality. Additionally, the construction and cement industries utilize this technology to transport cement slurry, mortar, or other building materials to construction sites. Each of these applications benefits from the ability of slurry pneumatic conveying to handle materials with high moisture content, abrasive properties, or varying particle sizes, making it a versatile and reliable solution for material transport.
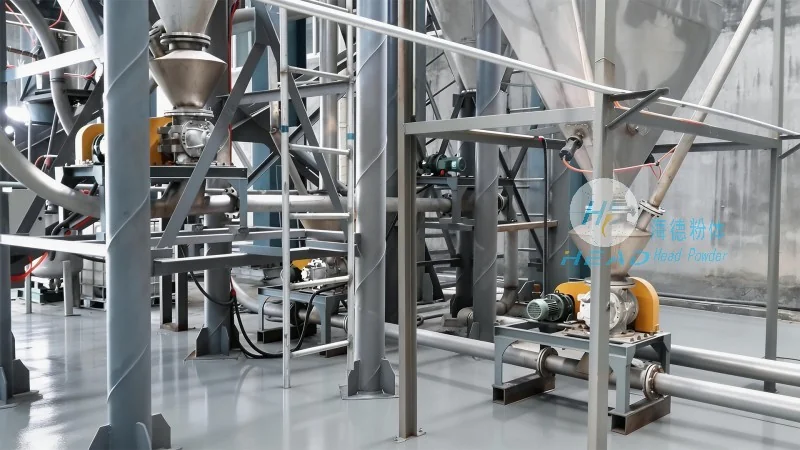
Compared to traditional material transport methods, slurry pneumatic conveying offers several advantages that make it an attractive choice for many industries. One of the primary advantages is its ability to handle materials that are difficult to convey using other methods, such as those with high moisture content or abrasive properties. This reduces the risk of equipment wear and tear, extending the lifespan of the conveying system. Another advantage is the compactness of the system, which requires less space compared to traditional conveyor systems, making it suitable for installations with limited floor space. The system also provides a more hygienic and controlled environment for transporting materials, especially in the food and pharmaceutical industries, where contamination and quality control are critical. Furthermore, slurry pneumatic conveying is energy-efficient, as it uses less power compared to other transport methods, leading to lower operational costs. The ability to transport materials over long distances without the need for intermediate storage or handling points also contributes to increased efficiency and reduced downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top