Warehouse vacuum conveying systems represent a sophisticated solution for material handling in modern industrial and logistics environments. These systems leverage vacuum technology to efficiently and safely transport bulk materials, making them an essential component in facilities where traditional mechanical conveying methods may be impractical or inefficient. The core principle revolves around creating a pressure differential between the source and destination, which enables the material to be drawn through a network of pipes and containers. This approach is widely adopted across various industries due to its versatility and ability to handle diverse material types, including powders, granules, and small parts. The technology is developed and implemented by Shandong HeadPowder Engineering Co., Ltd., a leading engineering firm based in Shandong, China, specializing in material handling solutions.
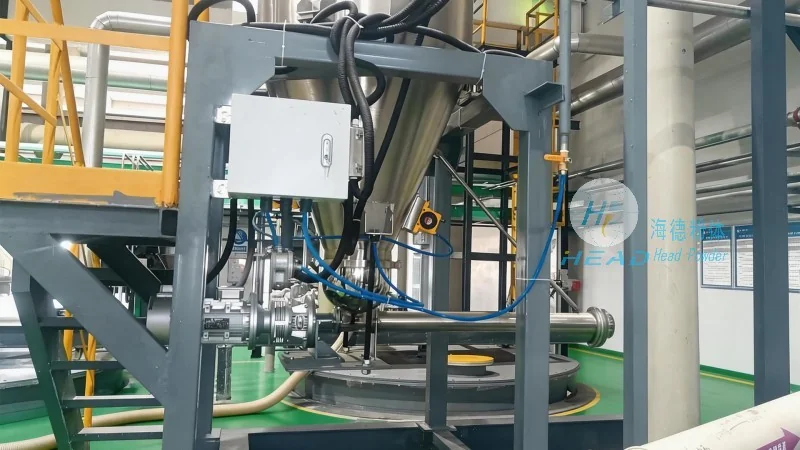
The operation of a warehouse vacuum conveying system relies on a carefully integrated set of components that work in concert to achieve material transfer. At the heart of the system is a vacuum pump, which generates the necessary suction force to pull material from the source container into the conveying line. The system typically includes a filter to capture fine particles and prevent contamination, a control valve to regulate airflow, and a collection vessel where the material is deposited at the destination. A control system monitors critical parameters such as pressure, flow, and temperature to ensure optimal performance and safety. The entire process is designed to maintain a consistent vacuum level, which is crucial for maintaining material integrity and preventing clogging or degradation.
Warehouse vacuum conveying is particularly well-suited for environments where manual handling is hazardous or where maintaining product purity is paramount. The system's ability to handle fine powders and granules without clogging or degradation makes it ideal for applications in the pharmaceutical, food processing, and chemical industries. In a typical warehouse setting, the vacuum conveyor can be seamlessly integrated into existing storage and processing lines, reducing the need for manual labor and minimizing the risk of product contamination. The flexibility of the system allows for easy reconfiguration to accommodate different material types or operational changes, enhancing overall operational efficiency and adaptability. The low noise and vibration levels of the vacuum pump make it suitable for use in environments where noise control is a priority, such as in distribution centers or manufacturing plants.
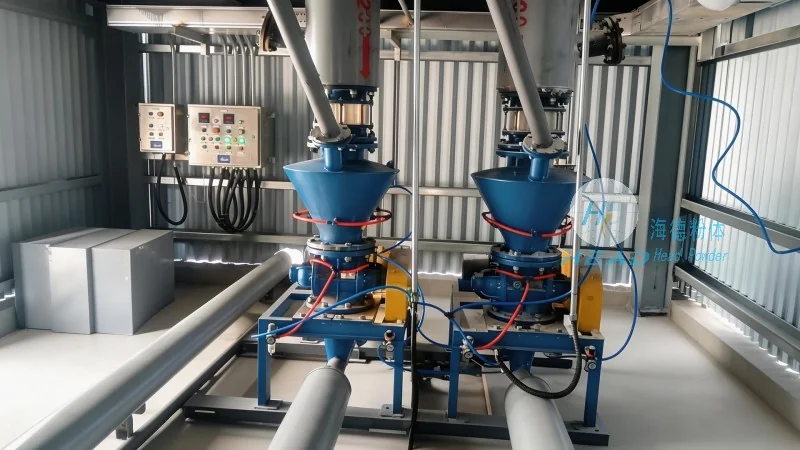
One of the primary advantages of warehouse vacuum conveying is its adaptability to diverse operational needs. For instance, in a food processing facility, the system can be used to transport raw ingredients like flour or sugar from storage silos to production lines, ensuring a clean and hygienic transfer process. In the pharmaceutical industry, the vacuum conveyor is essential for handling sensitive powders, as it maintains product integrity and prevents cross-contamination. Additionally, the system's energy efficiency and reduced maintenance requirements contribute to lower operational costs compared to traditional conveying methods. The ability to handle materials with varying flow characteristics, such as cohesive or fine powders, makes it a versatile solution for a wide range of applications.
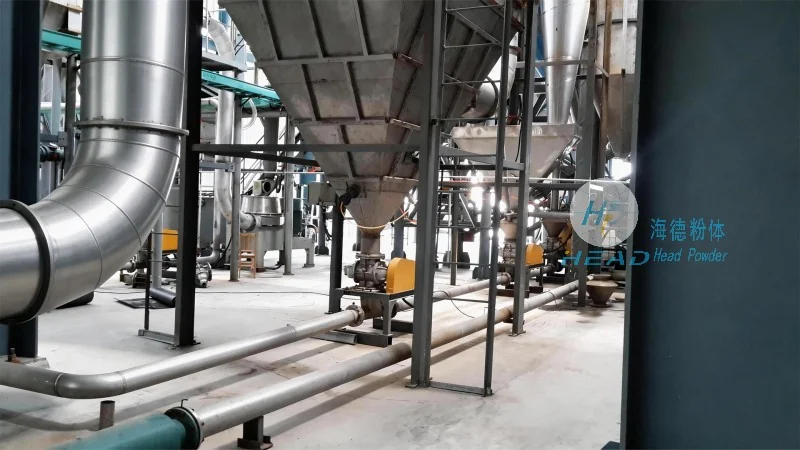
While warehouse vacuum conveying offers numerous benefits, proper operation and maintenance are crucial to ensure long-term performance and reliability. Regular cleaning of the filter and collection vessel is necessary to prevent clogging and maintain suction efficiency. The vacuum pump and control system should be inspected periodically to identify any signs of wear or malfunction. The system's design should consider the specific properties of the material being conveyed, such as particle size, moisture content, and flow characteristics, to optimize performance and prevent equipment damage. Proper training for operators on system operation and maintenance is also essential to maximize the system's lifespan and efficiency.
Warehouse vacuum conveying systems represent a critical advancement in material handling technology, providing efficient, safe, and flexible solutions for modern industrial and logistics operations. By leveraging vacuum technology, these systems enhance operational productivity and maintain product quality across various industries. The integration of advanced control systems and robust component design ensures that the system can meet the demands of diverse applications, from small-scale operations to large-scale manufacturing facilities. As industries continue to seek more sustainable and efficient material handling solutions, warehouse vacuum conveying remains a key technology in enhancing operational performance and supporting business growth. Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing tailored solutions that meet the unique needs of their clients in Shandong and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top