Automatic weighing and material conveying systems are critical components in modern industrial formulation processes, ensuring precision, efficiency, and consistency in material handling. This article explores the underlying principles of such systems and highlights key working scene characteristics that define their application across various industries.
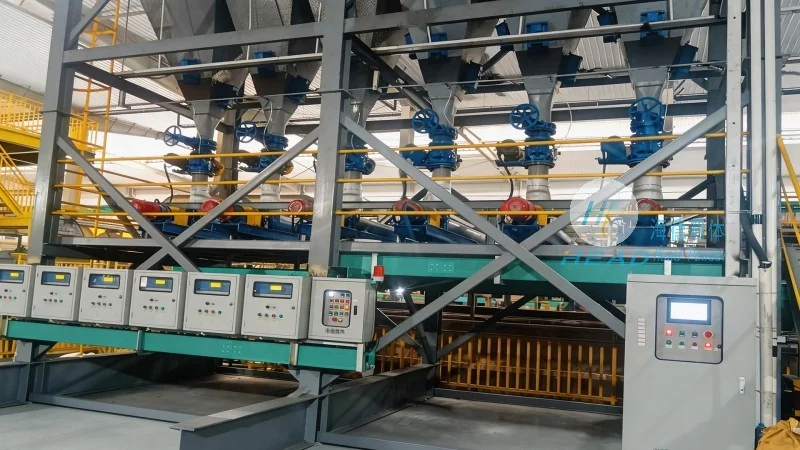
The fundamental principle of automatic weighing systems lies in the precise measurement of material mass using advanced sensors and load cells. These devices convert mechanical force into electrical signals, enabling real-time weight data acquisition. In material conveying, the system integrates with transport mechanisms—such as belt conveyors, screw conveyors, or pneumatic systems—to move ingredients from storage to processing areas. The synergy between weighing and conveying ensures that materials are transferred in controlled quantities, minimizing waste and optimizing production flow.
Automatic weighing and material conveying systems are widely adopted in sectors requiring strict quality control and regulatory compliance, including pharmaceuticals, food and beverage, and chemical manufacturing. In pharmaceutical production, for instance, these systems are essential for preparing active pharmaceutical ingredients (APIs) and excipients with high precision, as even minor deviations can impact drug efficacy and safety. The working scene in this context emphasizes sterile environments, rapid response times, and traceability of materials.
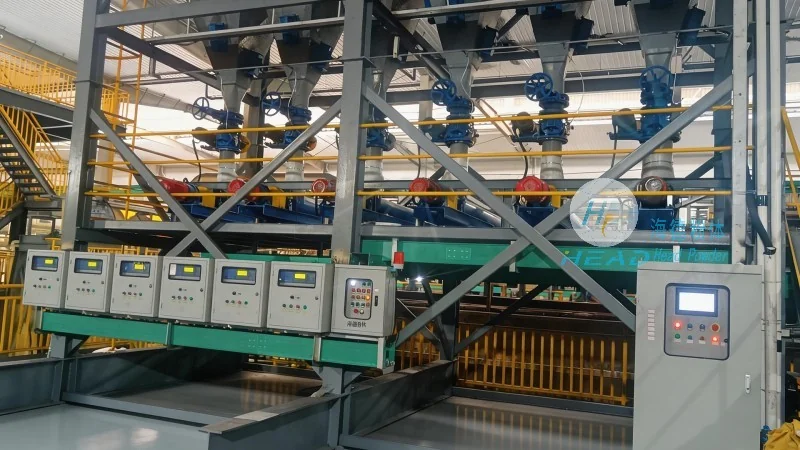
In the food and beverage industry, the systems are used for processing ingredients like powders, liquids, and solids, ensuring consistent product quality and meeting consumer safety standards. The working scene here often involves high-volume production lines, where efficiency and hygiene are paramount. Similarly, in chemical manufacturing, these systems help in blending raw materials for various products, such as fertilizers or coatings, by maintaining accurate ratios and preventing over or under-dosing.
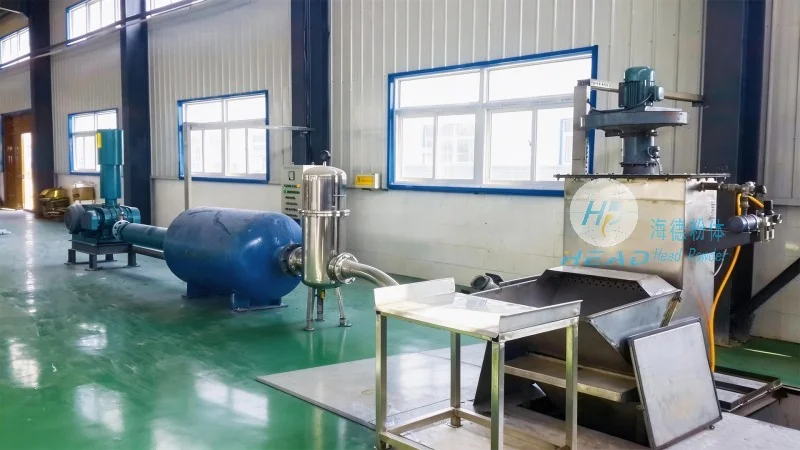
Across different working scenes, automatic weighing and material conveying systems offer several advantages. Firstly, they enhance operational efficiency by automating material handling, reducing manual labor and potential human error. Secondly, they improve product consistency by ensuring each batch is processed with uniform ingredient quantities. Thirdly, these systems contribute to cost savings through reduced material waste and lower labor costs. Additionally, the integration of sensors and control systems allows for real-time monitoring and adjustment, adapting to changing production demands or material variations.
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing advanced automatic weighing and material conveying solutions. With a focus on precision engineering and customer-centric design, the company has established itself as a trusted partner for industries seeking reliable and efficient material handling systems. HeadPowder's systems are tailored to meet the unique requirements of each working scene, ensuring optimal performance and compliance with industry standards. The company's operations are based in Shandong, China, where it leverages local expertise and resources to deliver high-quality products and services to global markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top