Continuous quantitative material conveying systems are integral to modern industrial processes, enabling the efficient and precise movement of bulk materials from one location to another. This technology is crucial for industries such as pharmaceuticals, food processing, and chemical manufacturing, where accuracy and consistency in material handling are paramount. The core principle behind these systems is the ability to transport materials in a continuous flow while maintaining a consistent, measurable quantity per unit time or distance. This ensures that downstream processes receive the exact amount of material needed, minimizing waste and optimizing operational efficiency.
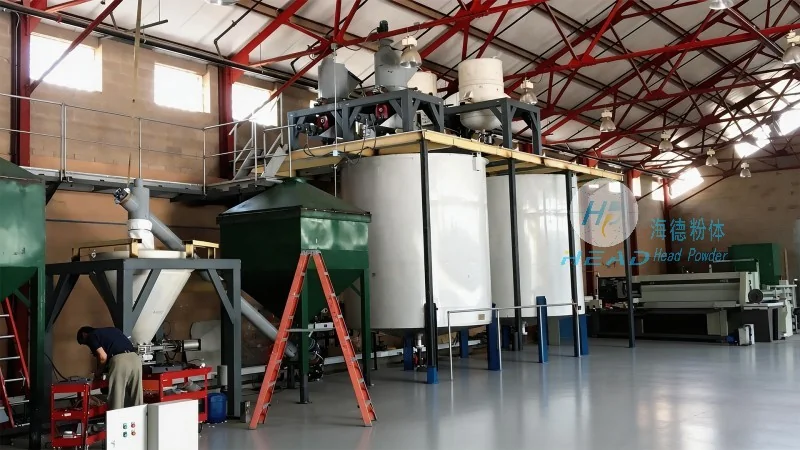
The fundamental principles of continuous quantitative material conveying revolve around precision, control, and reliability. These systems typically utilize mechanisms such as screw conveyors, belt conveyors, or pneumatic conveyors, each designed to maintain a steady flow rate. The key to achieving quantitative accuracy lies in the design of the conveying components, including the speed of the conveyor, the geometry of the conveying path, and the control systems that regulate the flow. For instance, screw conveyors use a rotating helical screw to move material forward, with the pitch and speed of the screw determining the volumetric flow rate. By adjusting these parameters, operators can achieve precise control over the quantity of material being conveyed. Similarly, belt conveyors employ a moving belt that transports material, and the speed of the belt, combined with the width and angle of the belt, influences the material flow rate. Advanced control systems, often integrated with sensors and feedback loops, further enhance the accuracy of the conveying process, ensuring that the output matches the desired quantitative specifications.
Continuous quantitative material conveying finds widespread application across various industrial sectors, each with unique requirements and operational challenges. In the pharmaceutical industry, for example, these systems are used to transport raw materials or finished products with high precision, ensuring compliance with stringent quality standards and regulatory requirements. The need for contamination control and hygiene in pharmaceutical manufacturing makes the selection of appropriate materials for the conveying components critical. Stainless steel and food-grade materials are commonly used to prevent cross-contamination and maintain product integrity. In food processing, continuous quantitative conveyors are employed in processes such as packaging, mixing, and sorting. These systems help maintain consistent product quality and ensure that the correct amount of ingredients is used in each batch, which is essential for meeting consumer expectations and regulatory guidelines. The food industry also demands high cleanliness standards, so conveyors are often designed with easy-to-clean surfaces and minimal dead zones to prevent the accumulation of residues.
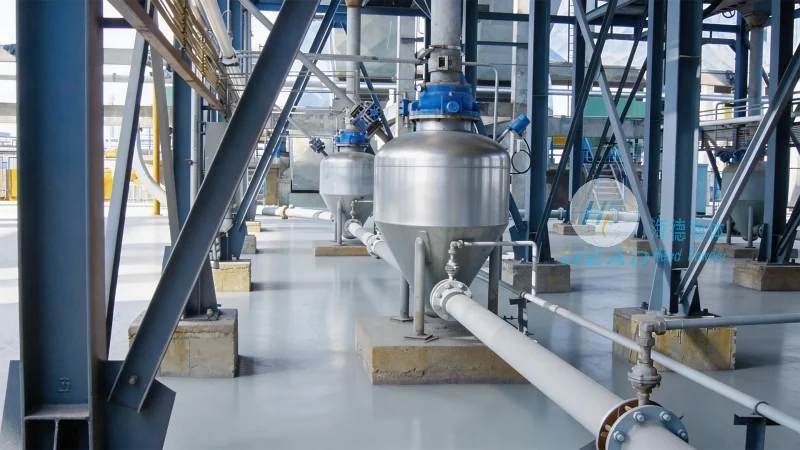
Consider a pharmaceutical company that produces tablets. The production line involves several stages, including raw material handling, mixing, compression, and packaging. The continuous quantitative conveyor system is used to transport raw materials, such as active pharmaceutical ingredients (APIs) and excipients, from storage to the mixing unit. The system must ensure that the exact amount of each ingredient is delivered to the mixer to maintain the correct formulation. Any deviation in the quantity of material could lead to batch failures or product recalls, which are costly and damaging to the company's reputation. The conveyor system in this case uses a screw conveyor with a variable speed drive, allowing precise control over the flow rate. Sensors are installed along the conveyor to monitor the material level and flow rate in real-time, providing feedback to the control system. This closed-loop control ensures that the material is conveyed at the exact rate required, minimizing errors and maximizing product quality. The system also includes cleaning-in-place (CIP) features, which allow for easy sanitation between batches, further enhancing operational efficiency and compliance with GMP (Good Manufacturing Practice) standards.
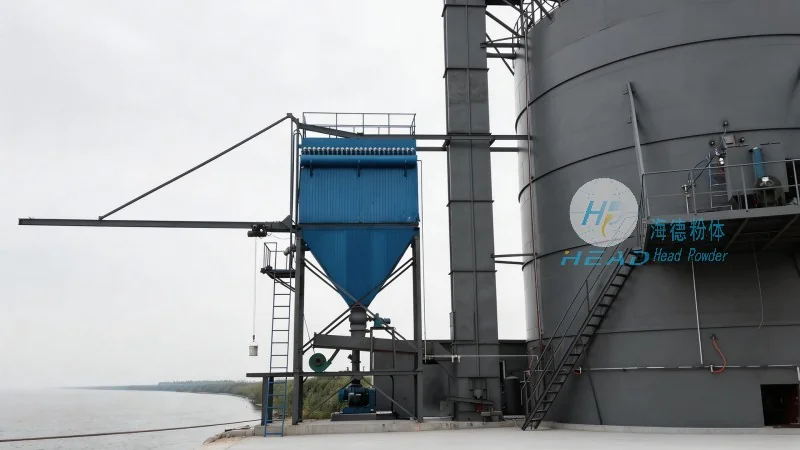
In a food processing plant, continuous quantitative conveyors are used in the production of snack foods, such as chips or crackers. The system transports raw ingredients, like potatoes or grains, from the receiving area to the processing line. The conveyor must maintain a consistent flow rate to ensure that the correct amount of material is fed into the cutting or extrusion machines. This precision is crucial for maintaining product uniformity and preventing over-processing or under-processing, which can affect the final product's texture and taste. The conveyor system in this food processing plant uses a belt conveyor with adjustable speed and tension controls. The belt width and speed are calibrated to handle the specific material characteristics, such as moisture content and particle size. The system is equipped with sensors that detect any blockages or variations in the material flow, triggering an alarm or automatic shutdown to prevent product damage. This ensures that the production line operates smoothly and that the quality of the final product is consistent. The conveyor also includes a cleaning system, which uses water and detergents to maintain hygiene standards, as required by food safety regulations.
Continuous quantitative material conveying systems from Shandong HeadPowder Engineering Co., Ltd. are designed to meet the diverse needs of industrial applications. The company offers a range of conveyor types, including screw conveyors, belt conveyors, and pneumatic conveyors, each with customizable features to suit specific requirements. For example, screw conveyors can be equipped with variable speed drives, adjustable pitch screws, and different materials of construction, such as stainless steel or food-grade plastics. Belt conveyors can be configured with various belt materials, widths, and lengths, and can include features like side walls or cleats to prevent material spillage. Pneumatic conveyors, on the other hand, use air pressure to transport materials, making them suitable for dusty or hazardous environments. The company also provides integrated control systems that can be customized to interface with existing plant automation systems, ensuring seamless integration and operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top