Desulfurization and dust removal processes in power plants and industrial facilities generate large volumes of fly ash, which requires efficient and reliable handling for disposal or reuse. Pneumatic conveying systems offer a sophisticated solution to transport this material, ensuring safety, environmental compliance, and operational efficiency. This article provides an in-depth analysis of such systems, highlighting their design, functionality, and the role of specialized engineering companies like Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder) in delivering tailored solutions.
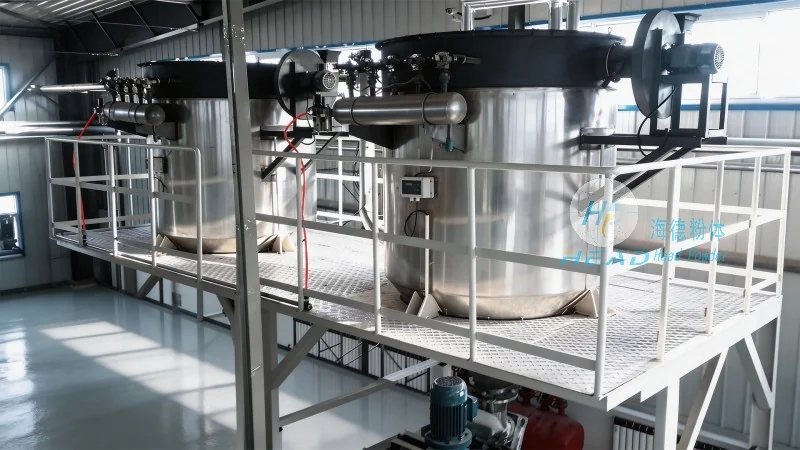
The core of a pneumatic conveying system for fly ash involves several critical components that work in tandem to ensure smooth material transport. The system typically includes a hopper or silo for ash storage, a feeder to control the flow rate, a conveying pipeline, and a receiver for the discharged ash. The working principle relies on the creation of a vacuum or pressure differential within the pipeline to move the ash particles through the system. Air is introduced into the pipeline, either by a blower or a vacuum pump, which generates the necessary force to propel the ash. The design of the system must consider factors such as ash particle size, moisture content, and the distance to be covered, as these variables impact the system's performance and efficiency.
Compared to traditional mechanical conveying methods, pneumatic systems offer several advantages that make them ideal for handling fly ash. One of the primary benefits is the ability to transport ash over long distances without the need for intermediate transfer points or complex infrastructure. This reduces the risk of material spillage and contamination, which is crucial for maintaining environmental standards. Additionally, pneumatic conveying systems are less prone to clogging and blockages, as the air flow helps keep the ash particles in suspension. This enhances the system's reliability and reduces downtime for maintenance. Another significant advantage is the flexibility in system design, allowing customization to meet specific project requirements. HeadPowder specializes in designing systems that optimize these advantages, ensuring that clients achieve cost-effective and sustainable ash management solutions.
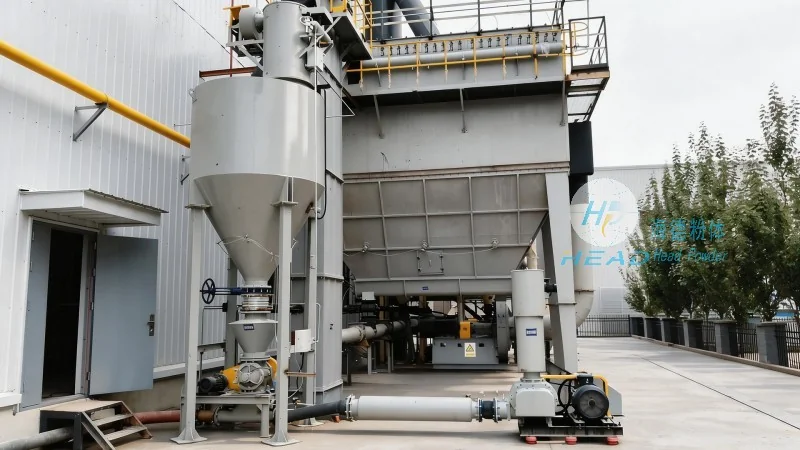
The successful implementation of a pneumatic conveying system for fly ash depends heavily on careful design and engineering. Engineers must consider various parameters, including the ash's physical properties, the required conveying capacity, and the layout of the facility. HeadPowder, with its extensive experience in the field, employs advanced computational fluid dynamics (CFD) and material flow analysis to model the system and predict performance. This approach allows for the optimization of component sizes, such as the blower capacity and pipeline diameter, to ensure efficient operation. The company also focuses on material compatibility, selecting components that can withstand the corrosive nature of fly ash and the abrasive effects of particle impact. By integrating these design considerations, HeadPowder delivers systems that are not only efficient but also durable and low-maintenance.
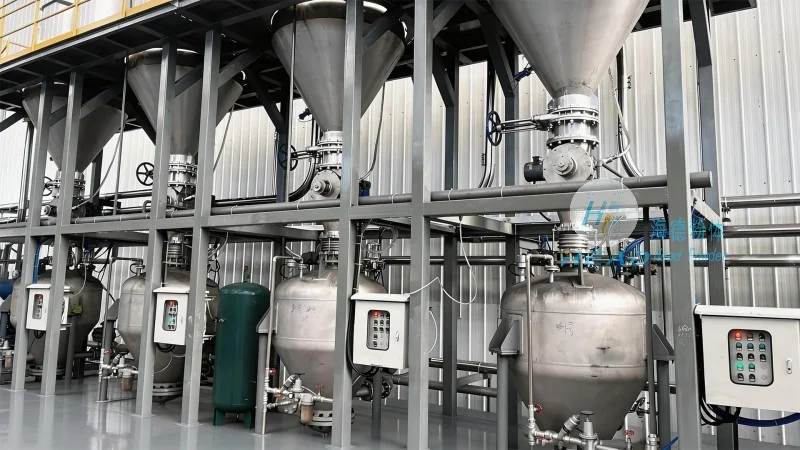
HeadPowder has successfully implemented numerous pneumatic conveying systems for desulfurization and dust removal fly ash in various industrial settings. For example, in a coal-fired power plant in Shandong, China, the company designed a system that transports ash from the flue gas desulfurization (FGD) unit to a storage silo over a distance of 500 meters. The system, equipped with a high-capacity blower and a flexible pipeline, achieved a conveying rate of 20 tons per hour, meeting the plant's operational needs while minimizing environmental impact. Another project involved a steel mill, where HeadPowder's system handled ash from the dust removal process, enabling the mill to recycle the material for cement production. These case studies demonstrate the effectiveness of pneumatic conveying systems in real-world applications and the expertise of HeadPowder in delivering customized solutions.
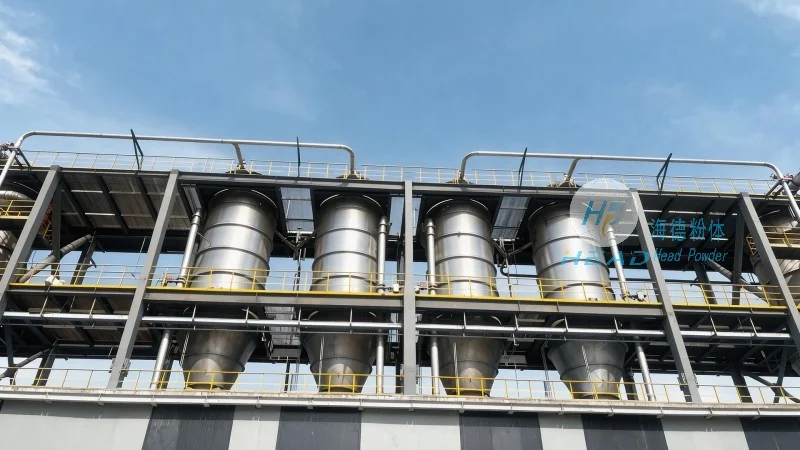
Efficient handling of fly ash through pneumatic conveying systems contributes significantly to environmental protection and workplace safety. By preventing ash spillage and dust emissions, the systems help maintain compliance with environmental regulations. The enclosed nature of the conveying pipeline reduces the risk of airborne dust exposure, which is a major health hazard for workers. Additionally, the systems minimize the need for manual handling of ash, reducing the risk of accidents and injuries. HeadPowder's systems are designed with safety features such as pressure relief valves and emergency shut-off mechanisms, further enhancing operational safety. These benefits make pneumatic conveying an attractive option for industries committed to sustainable and safe operations.
In conclusion, pneumatic conveying systems represent a highly effective solution for handling desulfurization and dust removal fly ash. Their ability to transport material efficiently, safely, and over long distances makes them indispensable in modern industrial facilities. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in developing and implementing these systems, leveraging their engineering expertise to meet the diverse needs of clients. As industries continue to prioritize environmental sustainability and operational efficiency, the demand for advanced pneumatic conveying systems is expected to grow. HeadPowder's commitment to innovation and quality ensures that it remains at the forefront of providing reliable and sustainable solutions for fly ash management.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top